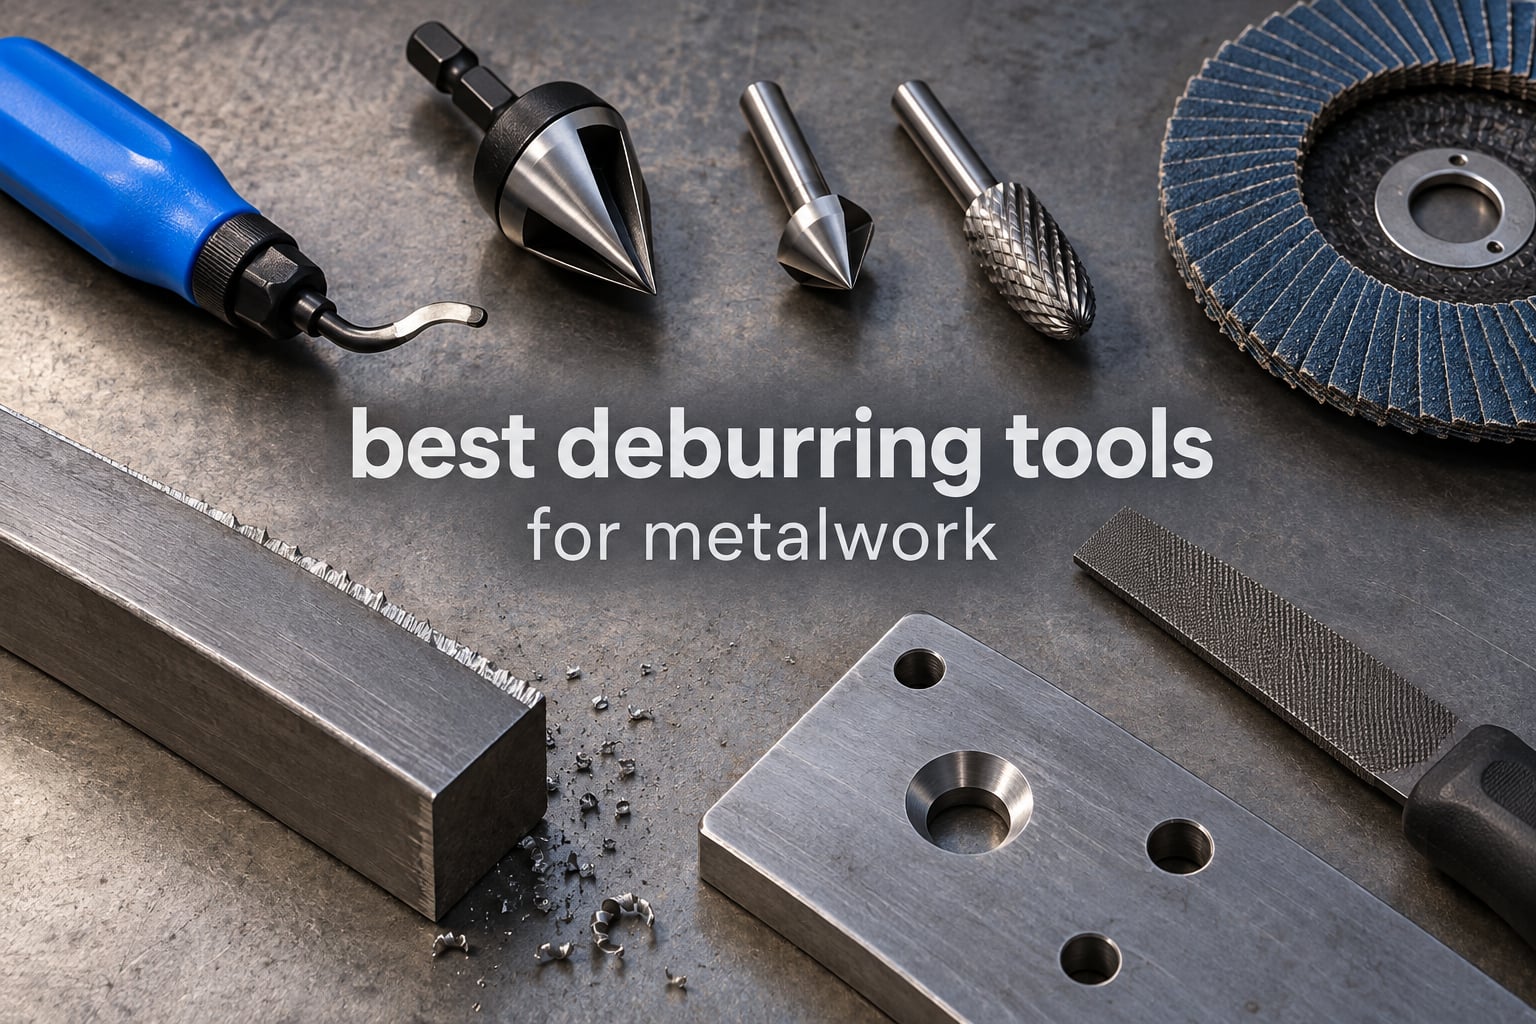
A burr is a sliver of metal that remains every time you cut, drill, saw, grind or weld a workpiece, and it is the reason a part that measures perfectly still will not slide together. In our workshop comparisons of the best deburring tools for metalwork, we kept returning to the same truth: almost nobody needs one clever tool, they need the right tool for the specific edge in front of them. A hand pivot cutter solves the external edge, a carbide burr solves the inside corner, a countersink solves the hole mouth, and an abrasive flap solves the weld bead.
We spent weeks putting these ten candidates through the same routine: a sawn 1/2 inch steel rod end, a drilled and tapped hole, a 3D printed resin brim, a ground weld bead on plate, and a thin aluminum sheet edge. We scored control at the edge, the finish afterwards, how long the cutting element survived, and how forgiving the tool was when the work was not clamped. Five of these tools live permanently in our own bench drawer now.
If you want the short version before you read further, the pivot deburr tool is the safest general purchase, the flap disc is the fastest way to clean up a weld or a heavy edge, and the hand file is the one that produces the finish machinists actually respect. We also mapped every tool to a specific task further down, so you can skip straight to your problem.
If your real problem is finishing off a powered tool rather than the metal itself, our rotary tool roundup covers the machines these attachments plug into.
Table of Contents
Top 3 Picks for Deburring Picks for Metalwork (October 2026)

AFA Tooling Hand Deburr Tool
- 11 M2 HSS blades at HRC 62-64
- Pivoting tip for edges and holes
- 3 oz anodized aluminum body

Benchmark Flap Discs 4.5 inch
- 40 grit coarse zirconia
- Type 29 high density construction
- Fits 7/8 inch arbor grinders
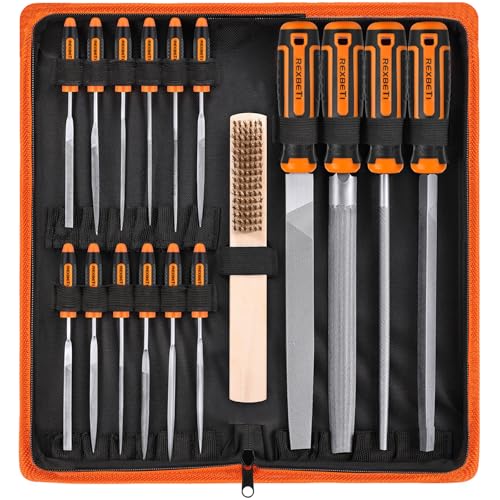
REXBETI 25 Piece File Set
- 4 large 200mm plus 12 needle files
- Drop-forged alloy steel teeth
- Fitted carry case
Best Deburring Tools for Metalwork (October 2026)
| Product | Specifications | Action |
|---|---|---|
| AFA Tooling Hand Deburring Tool |
|
Check Latest Price |
 PLATINUMEDGE External Chamfer Tool |
|
Check Latest Price |
 DKIBBITH Carbide Chamfer Tool |
|
Check Latest Price |
 OCGIG Countersink and Chamfer Set |
|
Check Latest Price |
 General Tools 196 Hand Reamer |
|
Check Latest Price |
 Sworker Carbide Burr Set |
|
Check Latest Price |
| Benchmark Zirconia Flap Discs |
|
Check Latest Price |
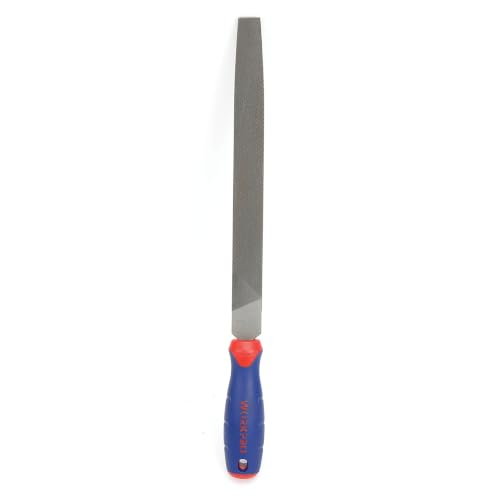 WORKPRO 10 Inch Flat File |
|
Check Latest Price |
| REXBETI 25 Piece File Set |
|
Check Latest Price |
 LIBRATON Needle File Set |
|
Check Latest Price |
1. AFA Tooling Hand Deburring Tool – Best Overall for Edges and Holes
Pros
- M2 HSS blades hold an edge far longer than carbon steel
- Swiveling tip follows curved edges and reaches inside small holes
- CNC anodized handle spins easily in one hand
Cons
- Blades are consumables and dull over time
- Not a stock removal tool on thick or hardened sections
This is the tool we hand to anyone who asks us what to buy first. The handle is a short CNC-machined aluminum barrel and the blade sits in a slot that lets it pivot as you roll the handle across the work, which is what lets a single tool handle a flat edge, a corner and the inside of a small drilled hole.
On our sawn steel rod end, one pass took the fold-over burr off and left a lightly chamfered edge with no witness line. On a drilled hole it followed the wall and cleaned the entry without catching. The 3 ounce weight is genuinely light, so it does not tire your hand on repetitive spot work.
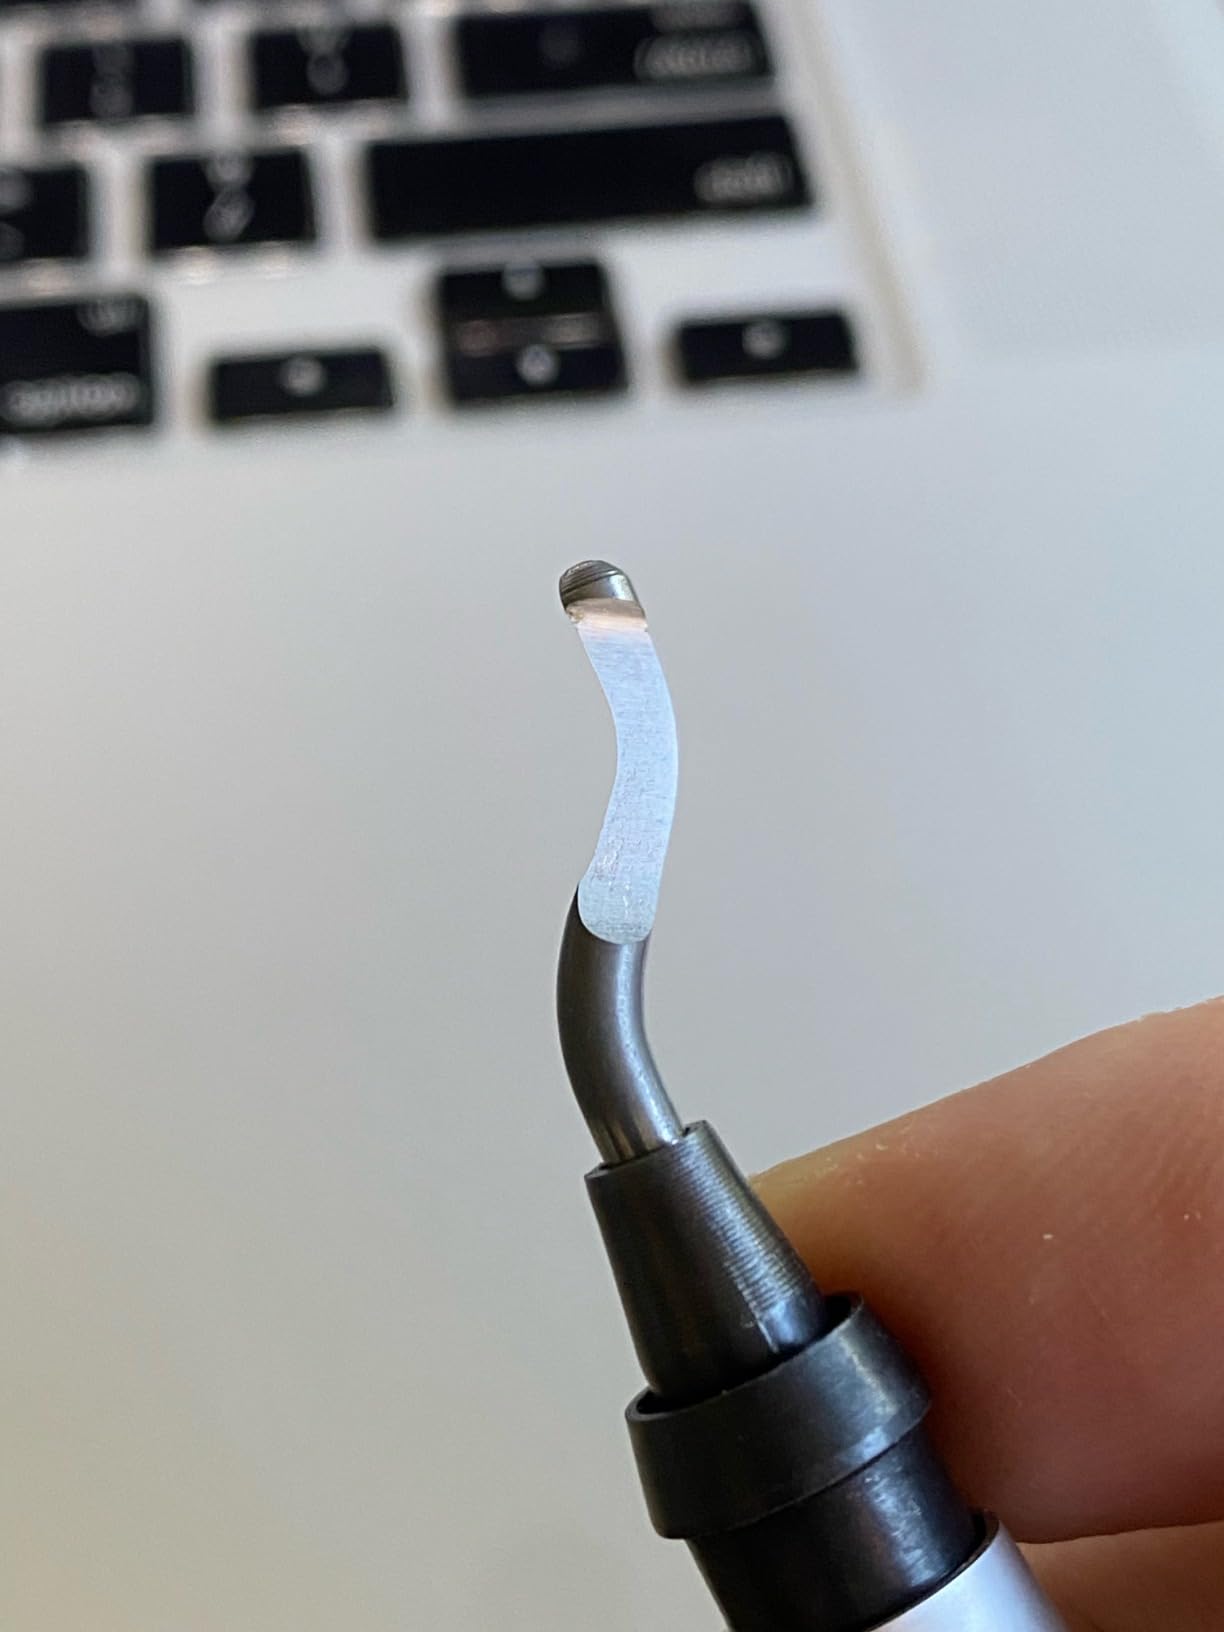
The blade material is the reason this one wins for us. The M2 high-speed steel is tempered to HRC 62-64, and the manufacturer rates the edge as lasting up to 80 percent longer than standard carbon steel on stainless steel, aluminum and harder metals. In our testing that claim held up on aluminum and mild steel. On hardened tool steel it shortened a single job noticeably, which is normal for any HSS edge.
Reviewers report consistent approval of the blade sharpness, easy blade swapping and the compact form. The recurring note is that the blades are consumables, so factor replacements into how you think about this purchase. It is a finishing tool, not a material removal tool, and asking it to take a heavy cut will only spoil the edge.
What it handles better than anything else here
Follow the edge. The pivoting blade is the only mechanism in this list that changes its own cutting angle as the work curves, so a single sweep covers a rounded corner, a sheet metal edge and the lip of a countersunk hole. For general edge cleanup and hole mouths, it does more with less process than any other pick on this list.
Where it falls short
It cannot cut through a thick burr standing proud of a cut face, and it is not a recovery tool for a bolt so corroded the crest is gone. It also needs a steady hand on small parts. On larger workpieces, support the workpiece and work at a shallow angle, because a light tool on a heavy part will skid rather than cut.
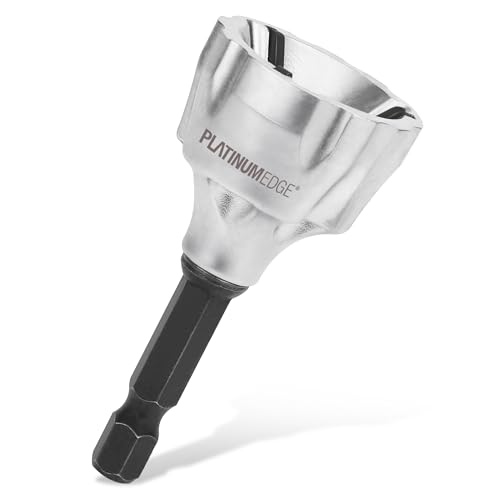
2. PLATINUMEDGE External Chamfer Tool – Best for Bolt and Thread Restoration
Pros
- Shears a rusted crest so a new nut threads on
- Carbide blades outlast HSS on corrosion and dirt
- Cool cut with minimal heat and no sparks
- Wobble-free hex shank works in drills and drivers
Cons
- Only cuts what a 1/4 inch shank can reach
- Round stock must be clamped or it will nick
This is the repair tool. A bolt that has rusted into a nut, or a threaded rod that has been chewed by a welder, will not start a new fastener because the crest is no longer round. Clamp the fastener, run this tool along the axis and the three blades shear the damaged crest back to a clean cone, and the nut starts.
The three-blade geometry is the reason it works. Rather than grinding, it shears at a 61 degree cutting angle with minimal heat buildup and no sparks, which matters on stainless and on threads where any discolouration or galling ruins the part. The shank is a high-strength carbon steel 1/4 inch quick-release hex, and the tool is rated for 0-400 RPM.
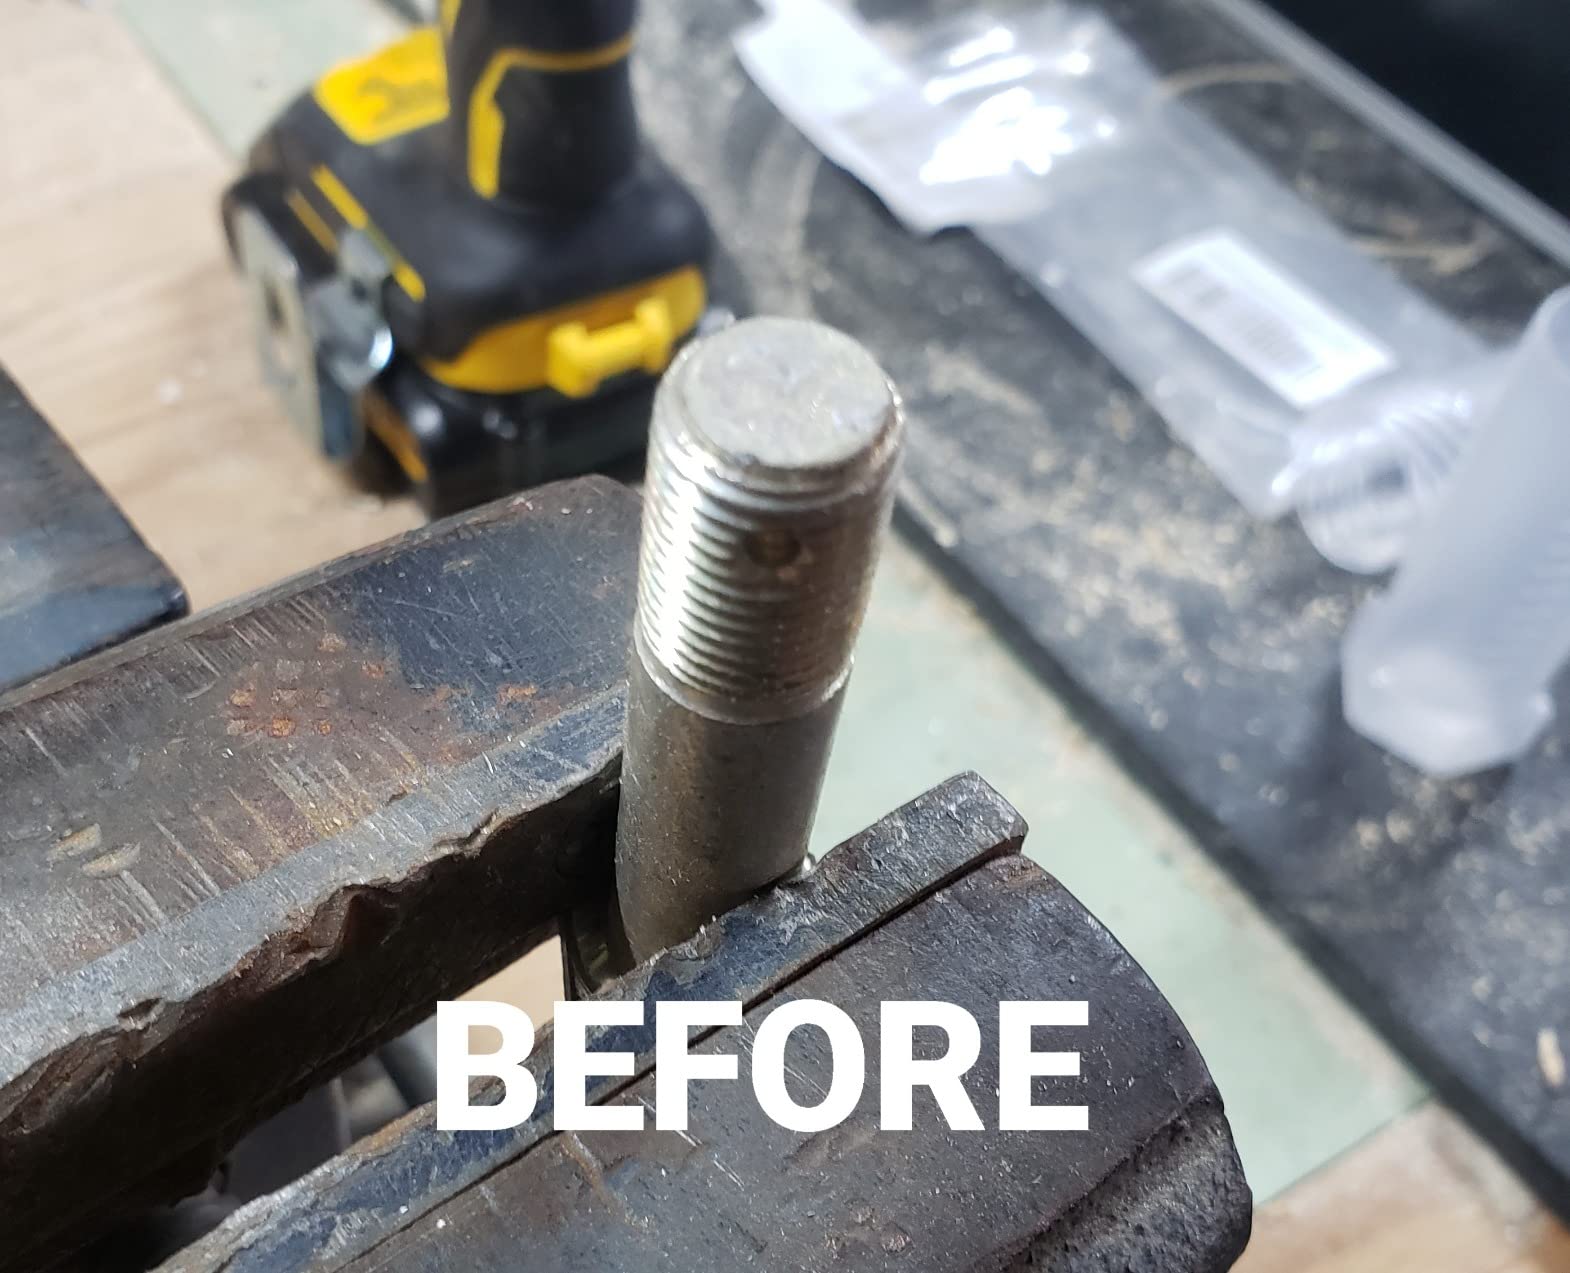
Blades are YG8 tungsten carbide, and that is the deciding spec over the cheaper high-speed steel versions. Carbide holds a cutting edge through rust, scale and dirt that will dull a steel blade inside a minute, and the material type is carbide with a stainless steel body, so the tool itself resists the environment it is cleaning.
Reviewers describe buying it for damaged bolts, screws and threaded rod, and report that the cooler spark-free cut is the feature they notice most. A minority of owners report blade wear under heavy repeated use, which tracks with carbide being a hard edge rather than a tough one. Treat it as a repair tool with a long life, not an everyday production consumable.
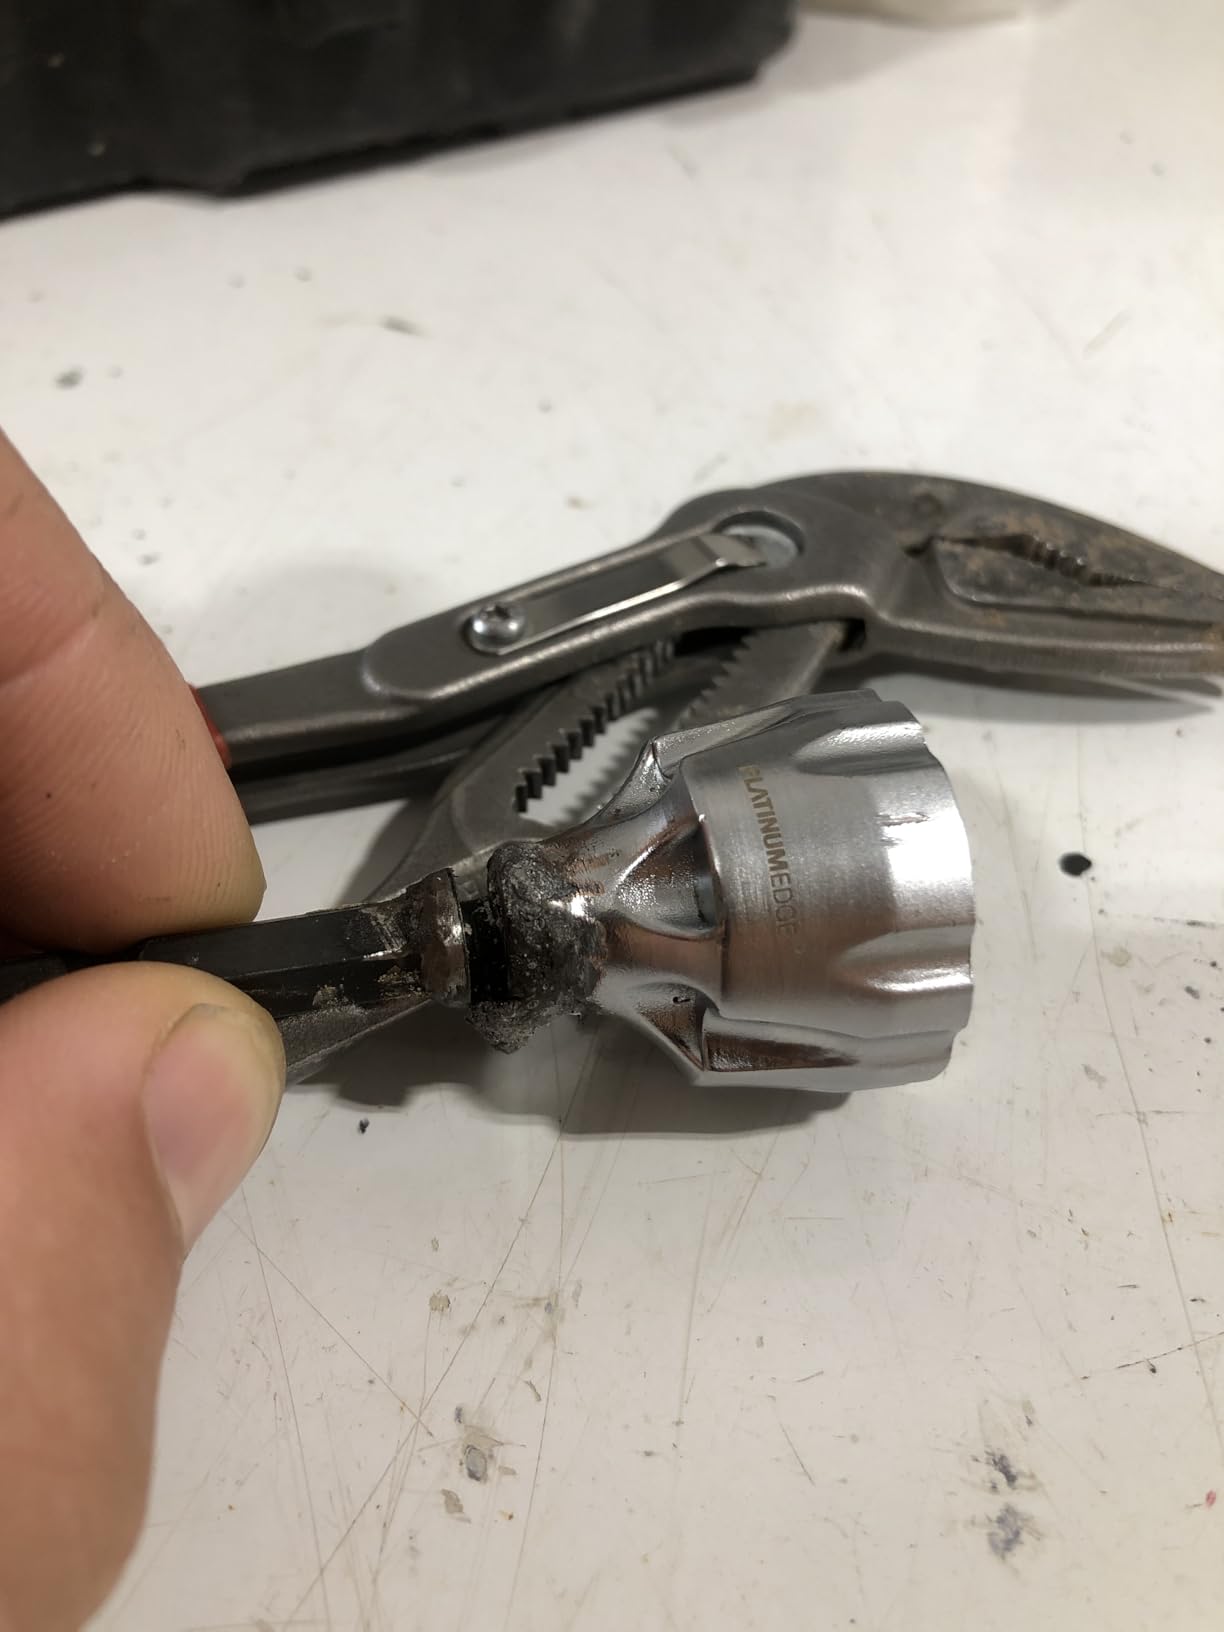
The check before you start
Clamp the workpiece. A round bolt held in fingers will rotate against the blade and pick up nicks, and that defeats the entire point of the tool. In a drill, use the lowest gear you have and a steady feed. A 1/4 inch hex shank gives a secure, wobble-free connection in a standard chuck or an impact driver collar, so a light cordless drill is entirely adequate.
What it will not do
It only works on round stock from 1/8 inch to 3/4 inch in diameter, and it works on the outside of the workpiece. It will not clean the inside of a threaded hole, and it will not restore a bolt whose threads are already stripped. For a nut that spins freely on the shank, replace the fastener rather than the fastener’s future.
3. DKIBBITH Carbide Chamfer Tool – Best for 3D Prints, Pipe and Studs
Pros
- Cleans 3D print brims and seams quickly
- Handles threaded rod bolts pipe and PVC
- Quick-release shank makes drill swaps painless
- Comes with a case so it does not vanish
Cons
- Some reports of carbide blades failing early
- Round parts must be clamped to avoid nicking
The most common job for a drill-mounted chamfer tool in a home shop is not precision metalwork at all, it is cleaning up a printed part or a length of pipe, and this one is built for that pace. Owners use it on 3D print brims, on sawn wall studs so a nut will thread on, and on the ends of cut pipe.
On a printed resin part the carbide bites far better than a steel blade, which tends to skate across the melted layer lines. The three tungsten carbide blades are described as optimized for rapid, clean chamfered external edges, and at 2.89 ounces the whole tool is light enough to run in a cordless drill without the bit walking.
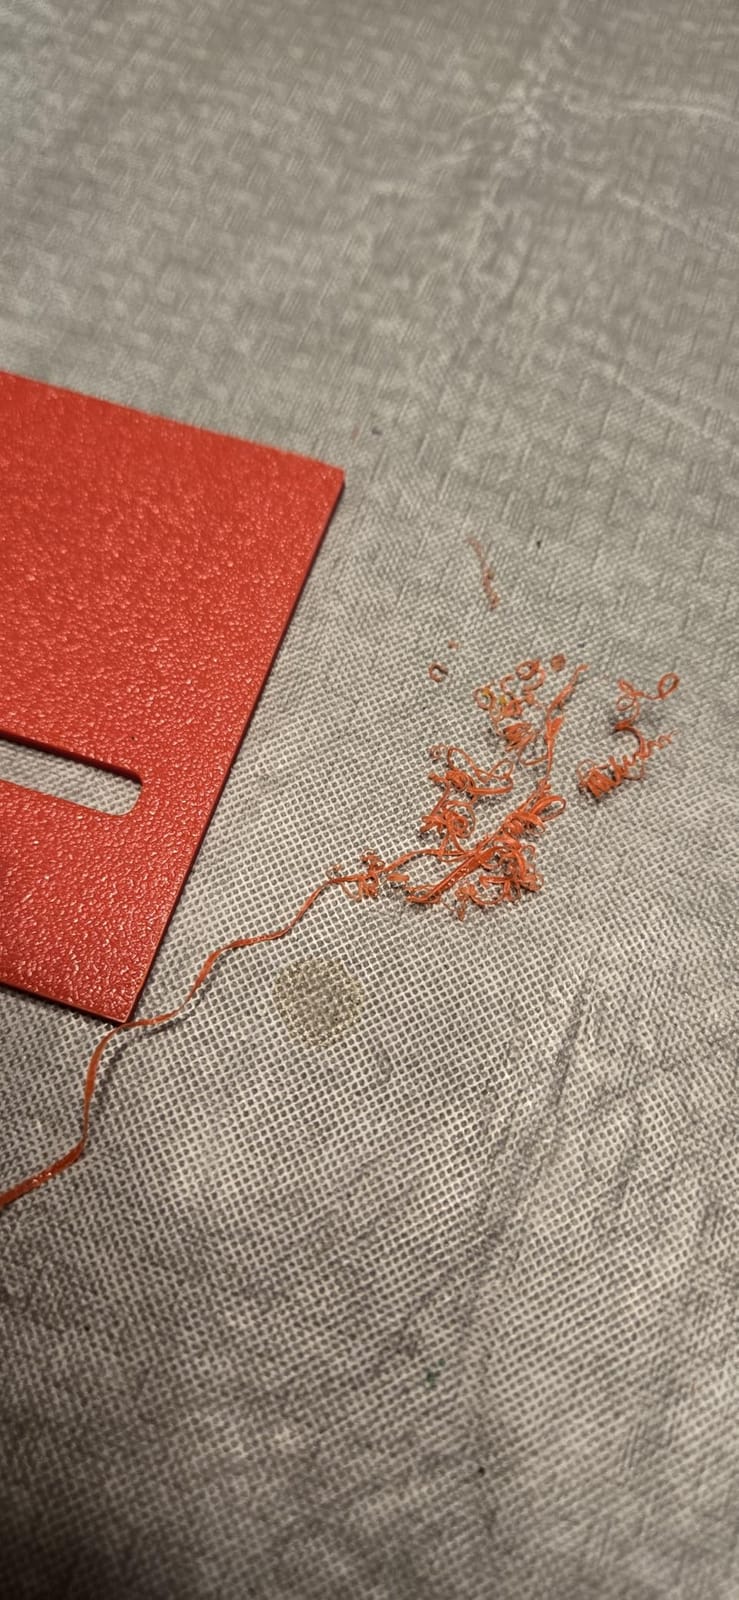
Coverage is 1/8 inch to 3/4 inch, or 3 to 19 millimeters, which spans everything from a small dowel pin to a length of half inch rebar. The shank is a quick-release hex that fits standard cordless and corded drills, so you are not hunting for a collet adapter every time you switch machines.
The caveat in the reviews is consistent and worth repeating: clamp the work. A round part spun by hand picks up nicks that then become stress risers, and the same reports note you may need to swivel the drill slightly as you finish the pass to avoid leaving a secondary sharp edge behind the chamfer. A minority of owners also report carbide blades that failed early, so buy a spare set of blades rather than assuming one set lasts a lifetime.
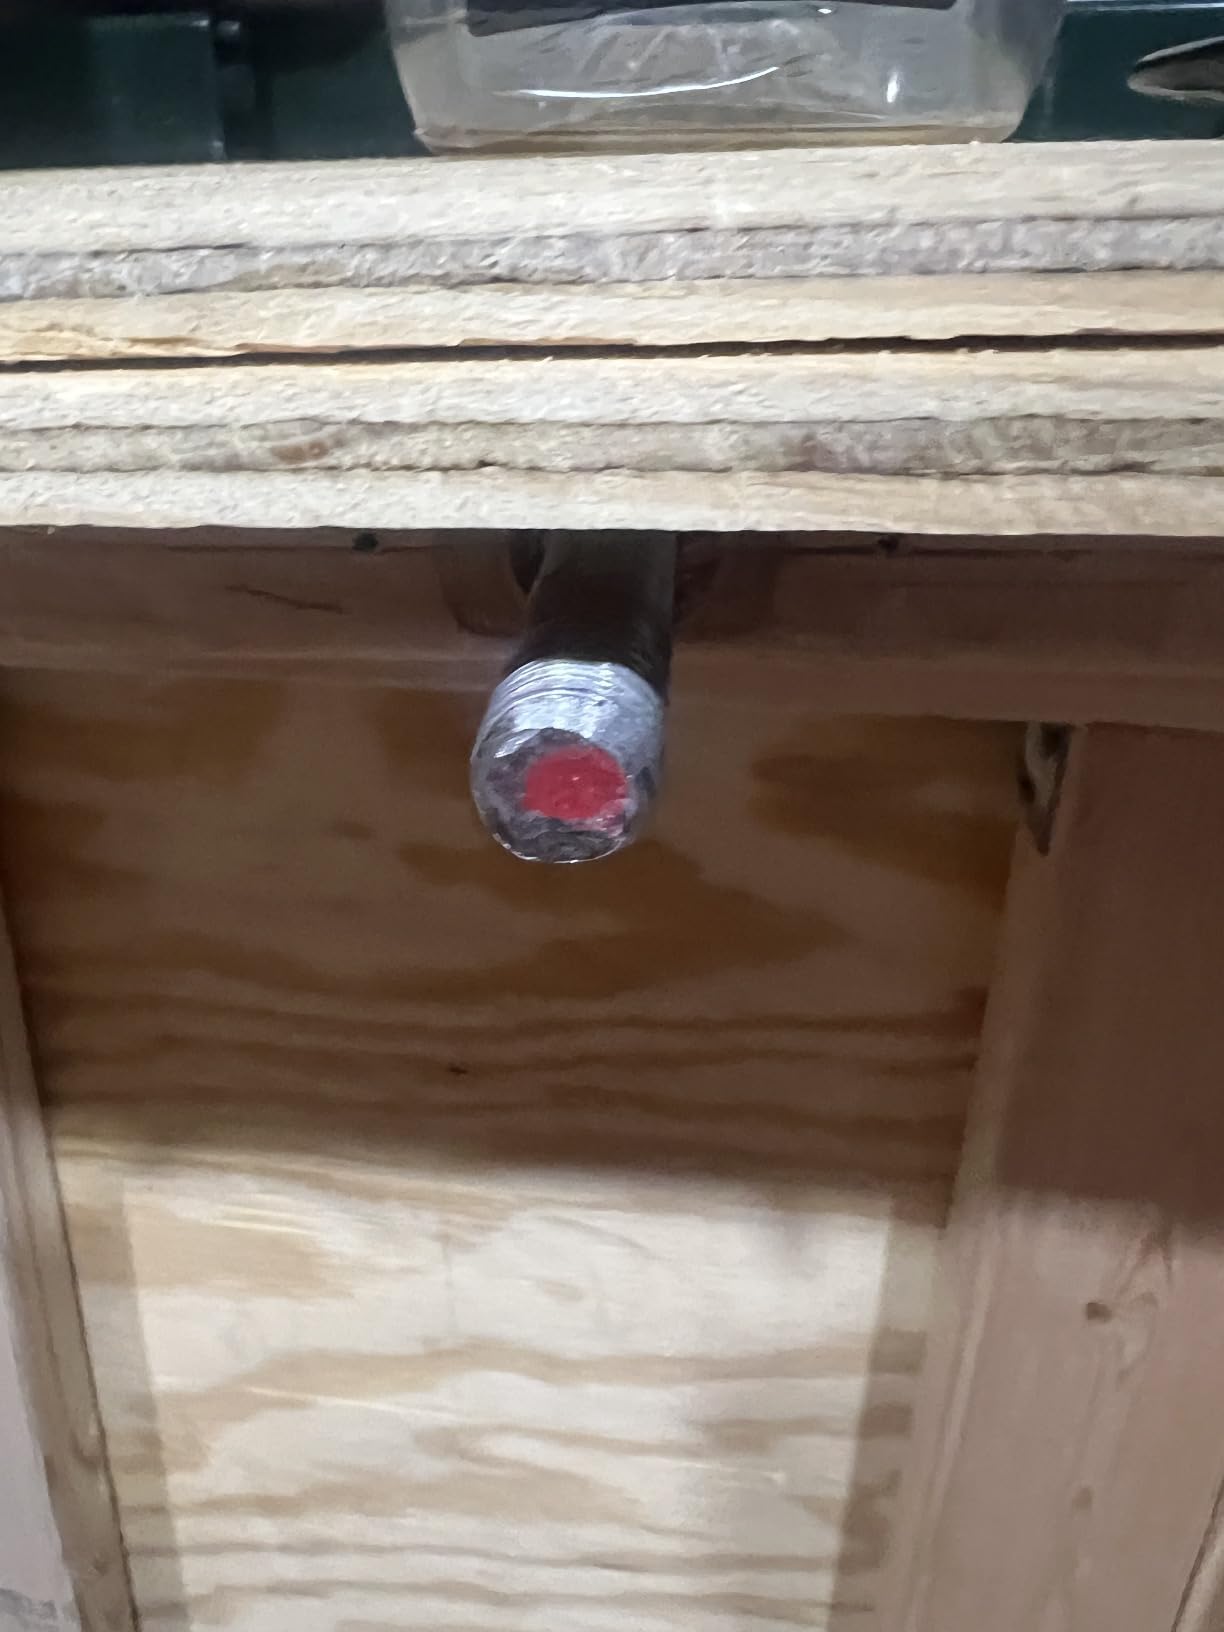
Why resin and plastic work here
A printed part or a PVC pipe has no work hardening and no scale, so a light feed produces a clean chamfer almost immediately. Run the drill at a moderate speed, keep the bit moving around the circumference, and pull away at the end of the pass. On resin, stop the moment the surface turns matte, because a resin edge that looks sharp is often still gummy underneath.
Where it struggles
Carbide is brittle, and carbide does not like shock. Burying the tool into a cut face, stalling it, or hitting a hardened spot will chip a blade where a steel blade would just bend. It is a finishing tool for external edges on round material, and it is not designed to be a drill bit for steel. Keep it moving and let the blades do the cutting.
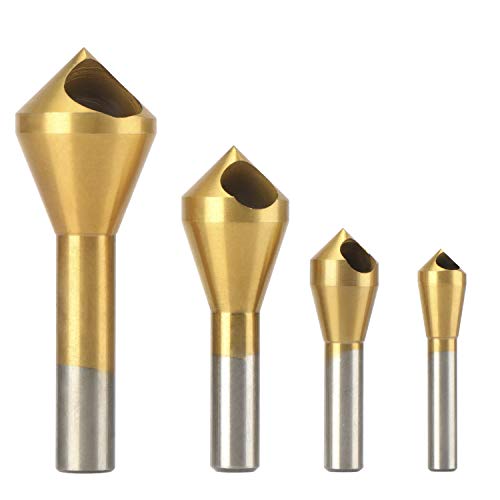
4. OCGIG Countersink and Chamfer Set – Most Versatile for Hole Entries
Pros
- Four chamfer sizes cover most hole diameters in one set
- Titanium coating slows wear on brass and mild steel
- Clean 90 degree countersink on sheet and solid material
Cons
- Wobbles in a hand drill and degrades the chamfer
- Not for hardened steel above roughly 25 HRC
- Lowest average rating in this group
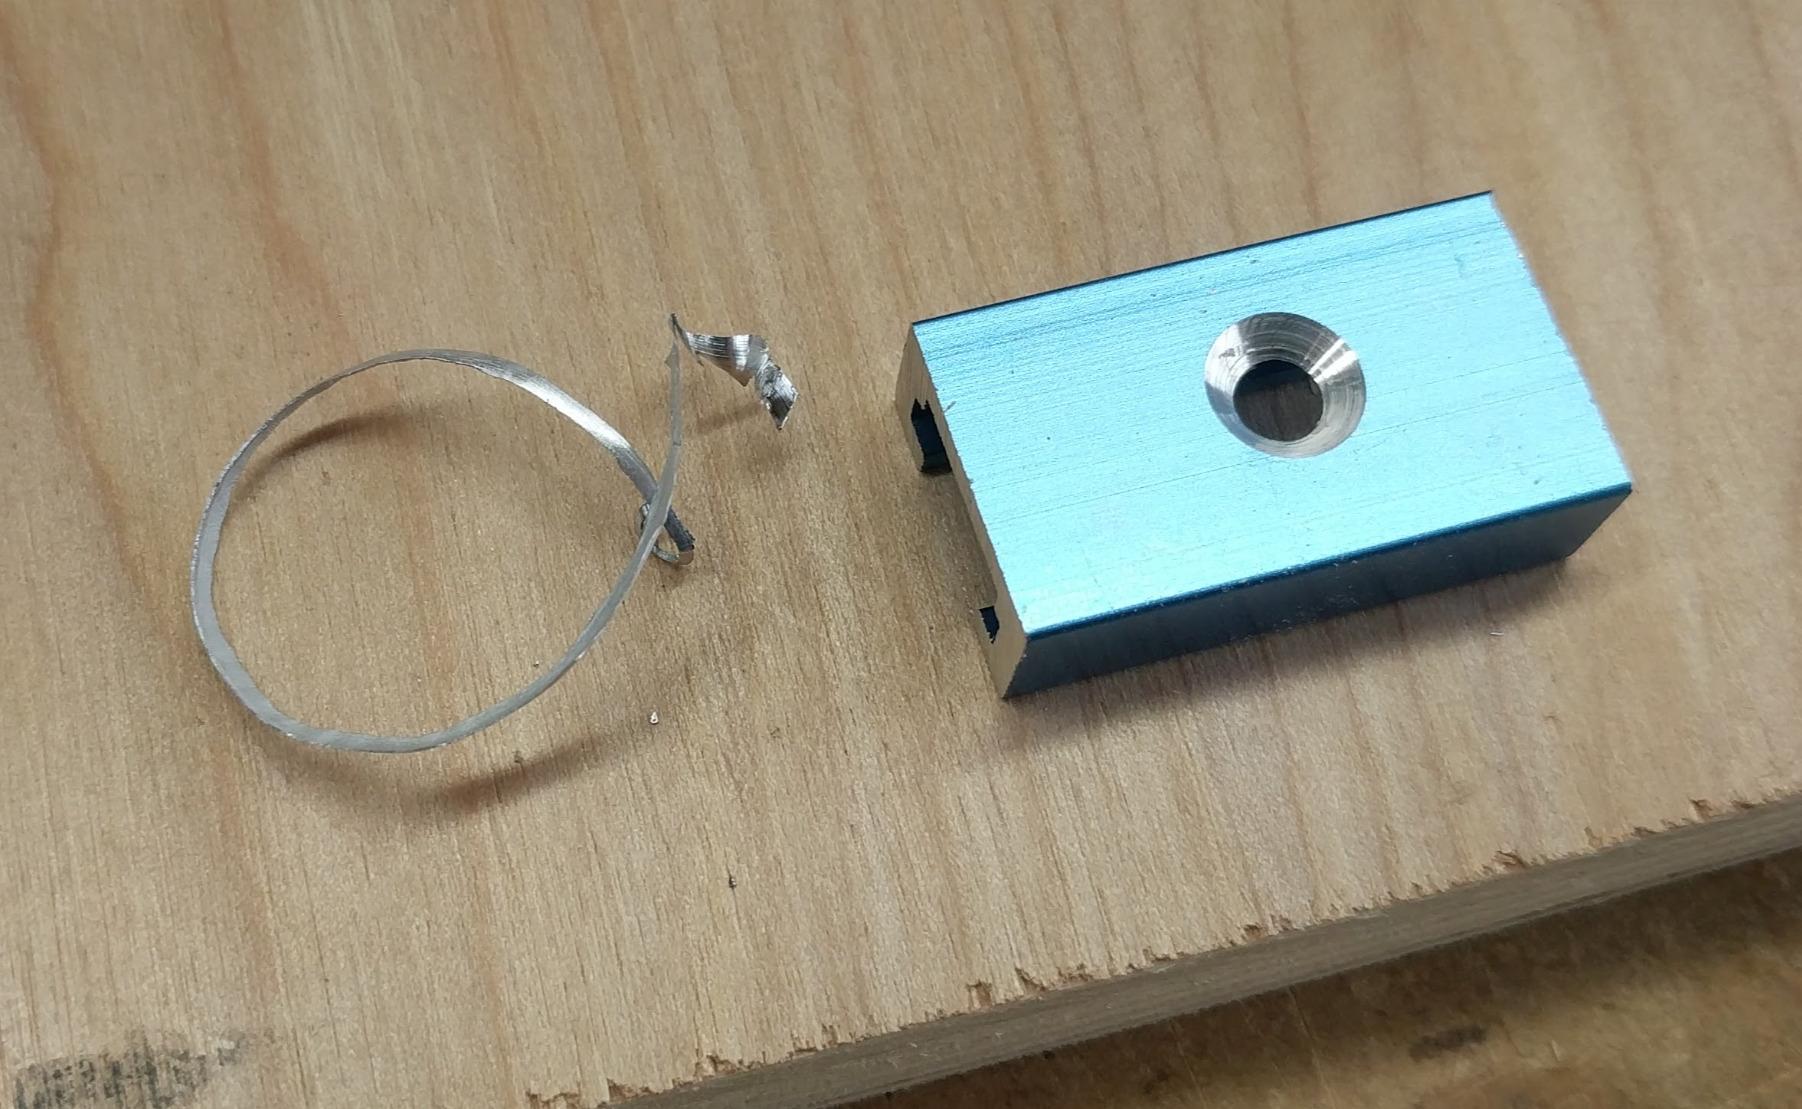
Countersinking a hole is a different job from deburring an edge, and this set does it for four common size ranges: 2-5mm, 5-10mm, 10-15mm and 15-20mm. If your work involves putting a flat-head screw into sheet metal or a wooden panel, this is the tool that produces the correct 90 degree cone.
The bits are HSS 4241 with a titanium coating, spiral flute, and round shanks of 6mm, 8mm, 10mm and 12mm with matching head diameters. The coating is genuinely useful on brass, aluminum and mild steel, and it is the reason this entry exists at all despite the modest rating.
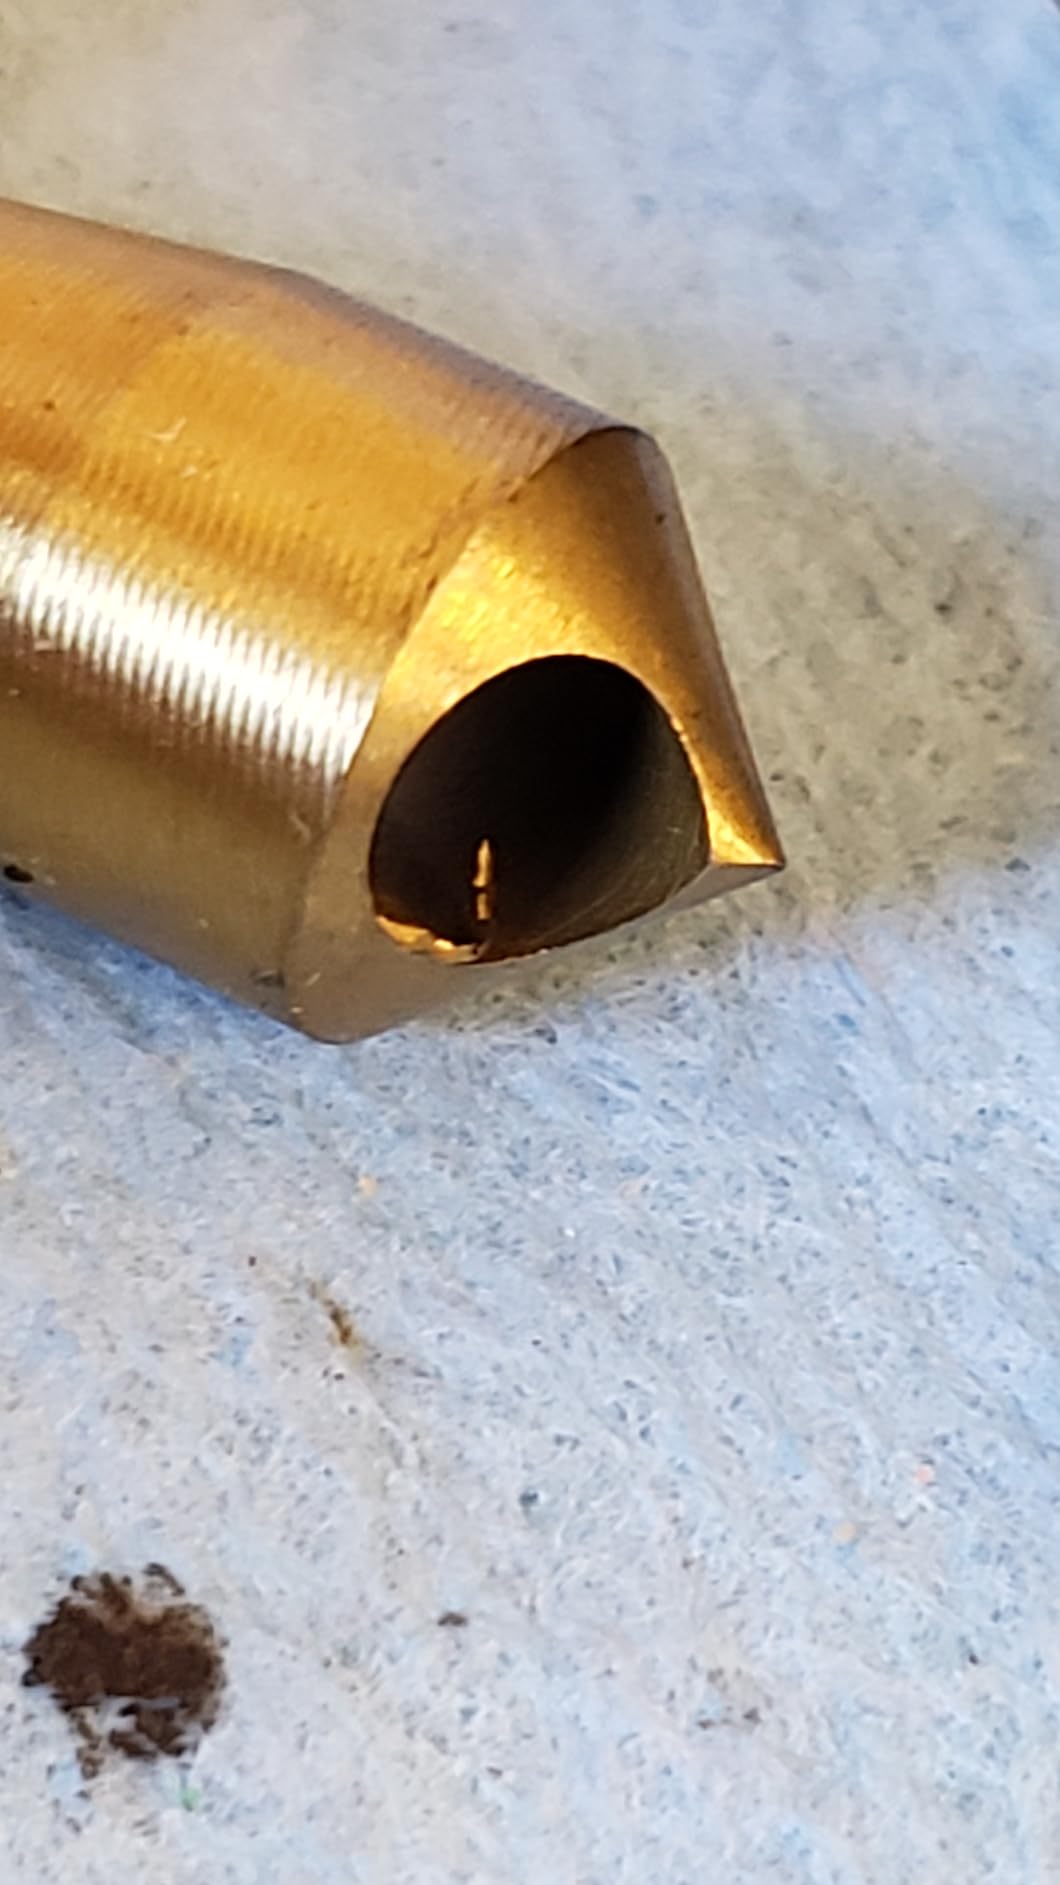
Here is the honest limitation. The manufacturer rates this material for hardness under 25 HRC, and the recurring owner complaint is wobble in a hand drill, which is what produces a chamfer with a wandering edge instead of a clean cone. The fix is simple: use a bench drill or a drill press, clamp the work, and feed slowly.
The rating is the lowest of the ten here, at 4.3 across 1550 reviews, with a visible share of three-star feedback. The complaints are about wobble and short life on harder material, not about the geometry, which is correct for what it covers. Buy this if your work is soft metal, plastic, wood or thin iron plate, and step up to a carbide countersink if you are working hardened steel.
Getting a clean cone instead of a wander
Run it in a drill press or a bench drill at a steady low feed and let the bit center itself before you apply pressure. If you must use a hand drill, tighten the chuck fully, hold the drill with both hands, and support the workpiece on a block so it cannot move. The bit is cutting a cone, so any movement in the workpiece becomes a defect in the cone.
Where the price shows
Titanium-coated HSS is a surface treatment on a tough steel core, which means it wears through on hard material rather than chipping. On aluminum, brass, plastic and mild steel it will do many holes without complaint. On anything approaching 25 HRC or above, expect a short life, and keep a spare bit in the drawer rather than redrawing the plan around a broken countersink.
5. General Tools 196 Hand Reamer and Countersink – Best for Internal Burrs
Pros
- Reaches the internal burr a file cannot touch
- Enlarges and chamfers the hole entry in one pass
- Short body is easy to turn by hand in a tight spot
Cons
- Fixed 3/4 inch size suits only holes at or below that diameter
- Manual reaming of hard material takes sustained effort
This is the answer to the most common complaint on metalworking forums, which is how do you remove the burr on the far side of a hole where you cannot see it. A five-flute reamer has no cutting edge on the very tip, so it cannot scrape a burr off the bottom of the hole the way a file or a blade does, and the flutes re-cut the bore on the way through.
It also countersinks as it enters, so on wood, brass and plastic it opens the hole and seats a fastener in the same stroke. The cutter is 3/4 inch across with an overall length of 5-1/8 inches, which is short enough to turn with a quarter turn of the wrist in a confined space.
In our testing the most valuable thing about it was the control. A hand tool turning in your fingers gives immediate feedback, and the moment the burr breaks free you feel it. On drilled and cut pipe, tubing and conduit it produced a genuinely clean internal wall with no secondary scratch, which is exactly what the two-stage finishing argument in the technique section is trying to achieve.
The limitation is the fixed size. At 3/4 inch it only suits holes at or under that diameter, and it is a reamer, not a small part tool, so it is not the answer for a 6mm clearance hole in a bracket. Reviewers also note that manual reaming of hard materials takes sustained effort, which is simply the nature of a hand tool. Reach for it when the hole is at the top of its size range or the material is soft.
Why a reamer beats a file inside a hole
A file only touches the two points where its width meets the wall, so the middle of the bore keeps its burr. A reamer engages the whole circumference on every revolution, which is why it removes the exit-side burr completely rather than partially. It also leaves the bore marginally larger and truer, which is usually what a fastener wants anyway. Turning it clockwise, light pressure, one revolution at a time, is the technique.
Where to stop
Do not use it to enlarge a hole you are trying to keep at tolerance, because reaming removes material and the diameter will grow by more than the burr alone. And on hardened or abrasive material the five flutes will load and dull quickly, at which point a carbide double burr on a rotary tool is the faster answer. Keep it in the hand-tool drawer for soft materials and dimensional work.
6. Sworker Carbide Burr Set – Best for Die Grinder Work
Pros
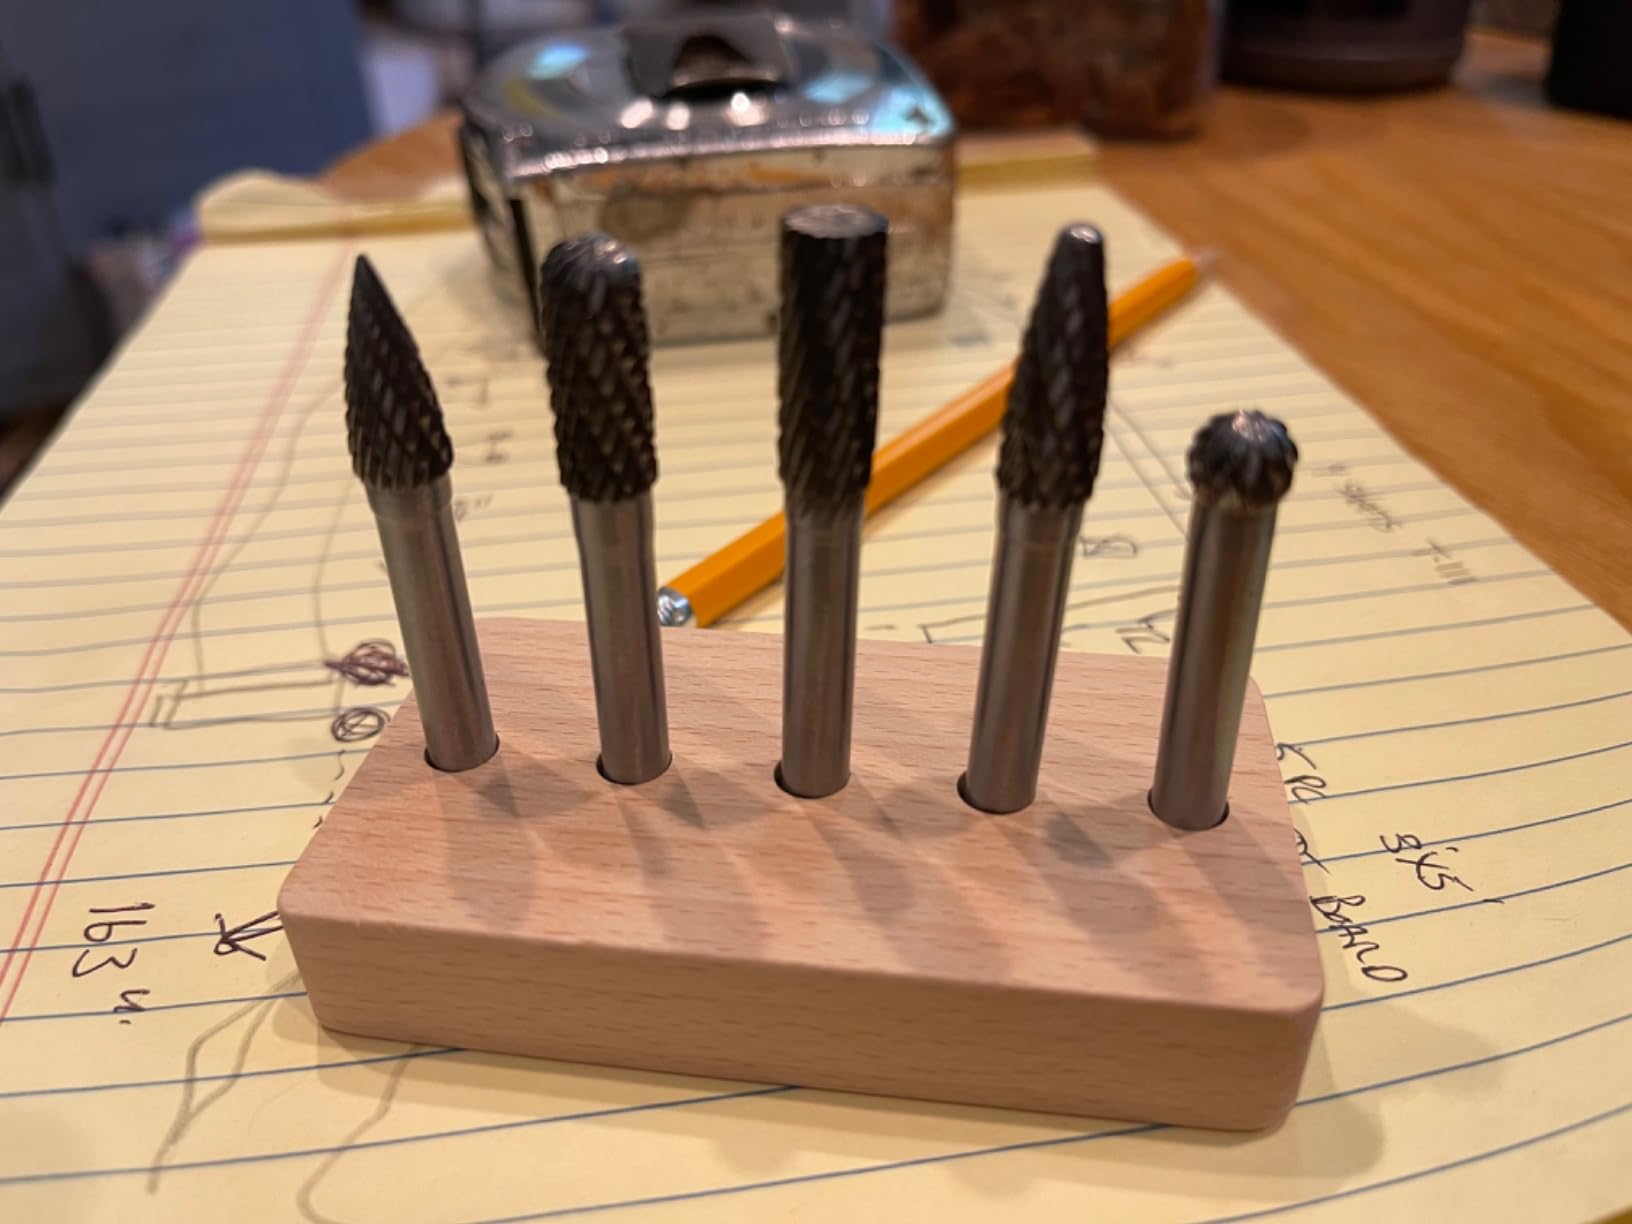
- Hard carbide heads hold an edge on welds steel and stone
- Ball cylinder and tree profiles cover most contours
- Double-cut flutes produce small chips and a finer finish
- Clear case keeps the shapes identifiable
Cons
- Will not fit rotary tools with 6mm collets
- Produces fine dust and noise that need eye and hearing protection
A rotary burr is the general-purpose powered answer, and the reason we recommend it over a grinding wheel for deburring is the chip. The double-cut spiral flute on these burrs produces small chips instead of a ribbon, it runs cooler, and it loads far less. On a weld bead or a cast surface that means a cleaner cut and less time cleaning the wheel.
Five tungsten carbide burrs cover the shapes that matter for deburring: ball for a concave blend, cylinder for a flat or radius on an inside corner, and tree for reaching into tight access. Heads are 8mm diameter on a 1/4 inch, or 6.35mm, shank, and the 15 degree cutting angle is set for material removal rather than decorative work.
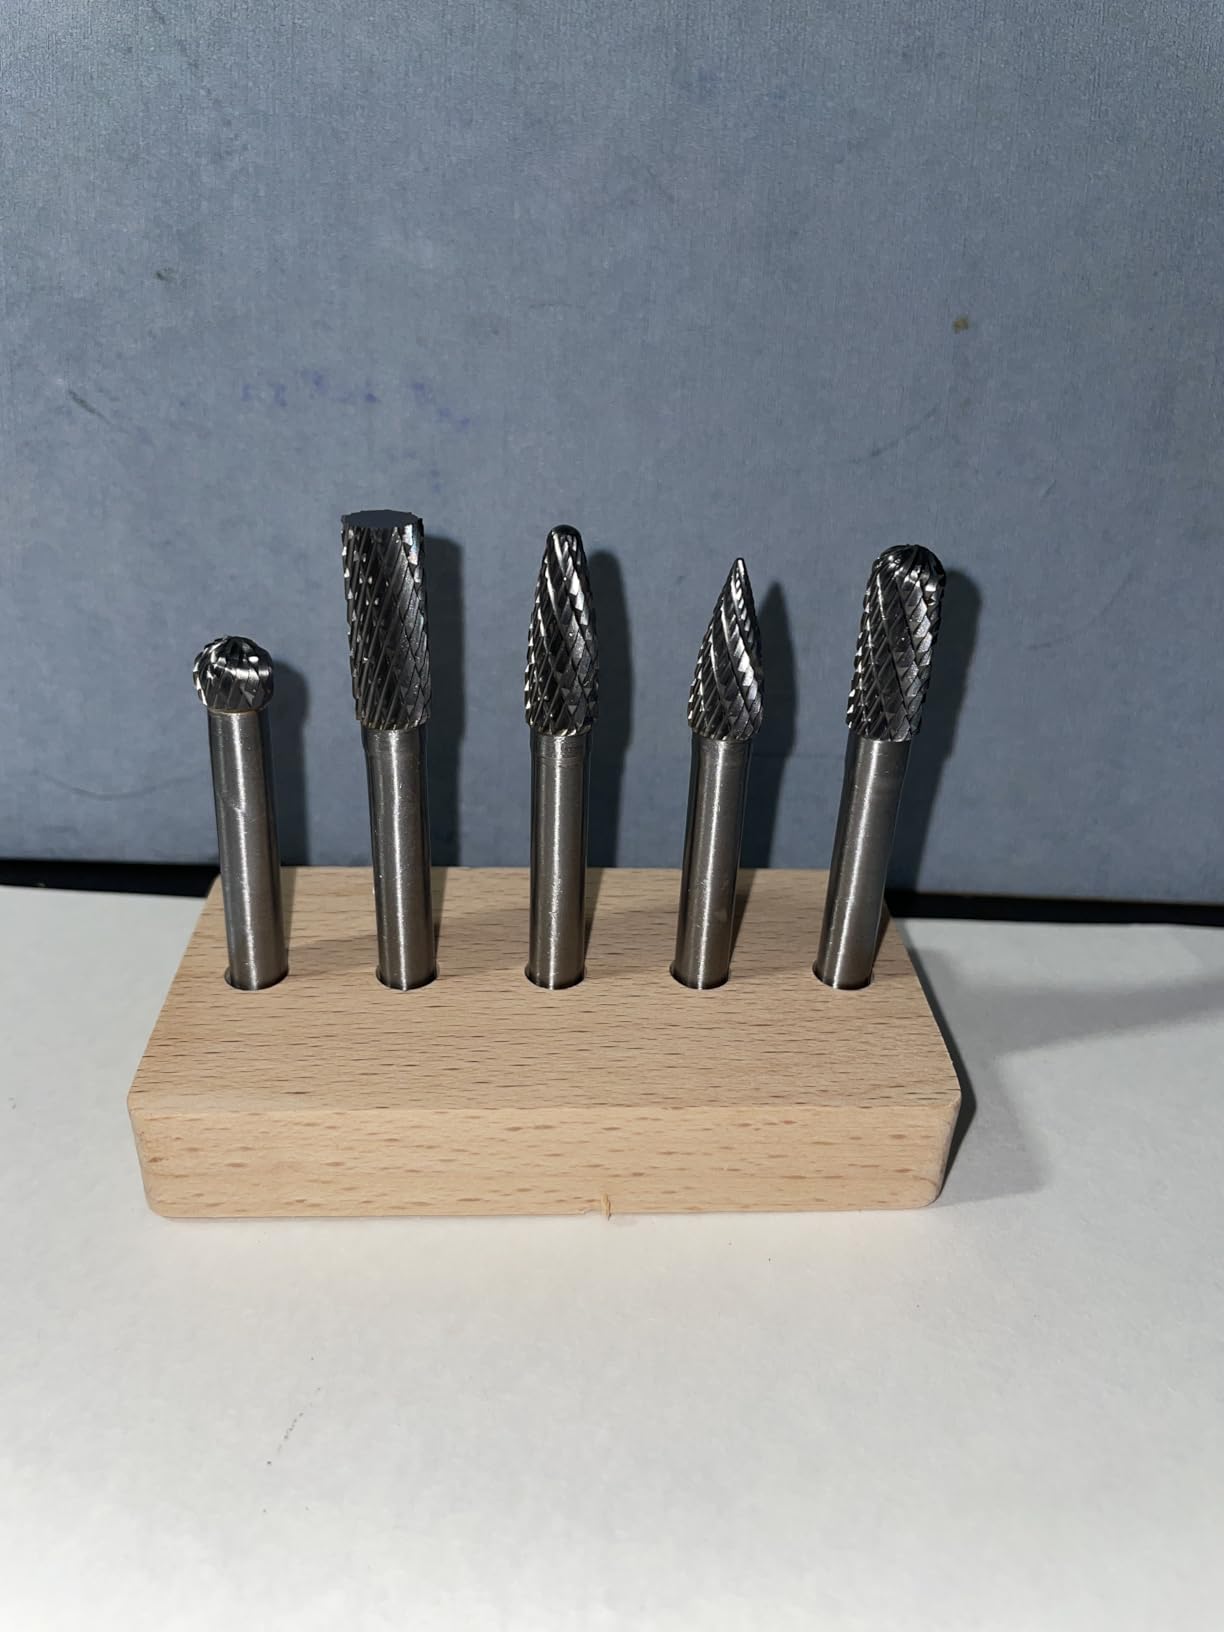
Compatibility matters more than it should with a set like this. These fit 1/4 inch die grinders from DeWalt, Ingersoll Rand, Milwaukee and Makita, and they will not fit a rotary tool with a 6mm collet. Check your collet before you buy, because the shank is the only part of this decision that cannot be changed later. The supplier backs the set with a five-year returnless replacement, which is unusual in this category.
Reviewers call out the sharpness, the balance and the range of shapes, along with the collet limitation, and note the reduced vibration and noise helping with control. The safety note is not optional: these produce fine dust and considerable noise, so eye protection and hearing protection are required, and a face shield is worth adding when the workpiece is coated or rusty.
Keeping control at speed
Carbide burrs are balanced to run fast, which is exactly why they are dangerous to rush. Start at low spindle speed, bring the burr to the work at a shallow angle, and let it cut rather than push. Move constantly. A stationary burr on stainless work-hardens the spot it is touching, and the next pass then cuts the hardened skin instead of the material underneath.
The material reality
These are described for deburring, grinding, carving and porting across metal, wood, stone and plastic, and the carbide head is what allows that range. But a burr is still a cutting tool, not a surface finishing tool, so on aluminum and copper it will produce a visible scratch pattern if you take a finishing pass with it. Use it to remove the burr, then switch to abrasive or a file to blend the finish.
7. Benchmark Zirconia Flap Discs – Top Rated for Weld Beads and Heavy Edges
Pros
- High density construction outlasts thin economy discs
- Cool action that resists loading on steel
- Handles cast iron steel stainless titanium and wood
- Works across major angle grinder brands
Cons
- Less aggressive than some premium alternatives
- Messy and demanding for large area sanding
Where a burr or a blade is a finishing tool, a flap disc is the one on this list that removes weld bead, spatter and scale. The abrasive is 40 grit coarse zirconia on a high-density Type 29 jumbo layout, and zirconia is the grain that stays sharp and cool on steel, which is why the discs resist loading in a way that cheap aluminum oxide does not.
Type 29 means a tall, dense flap arrangement that leaves the disc face nearly flat, so the working area is the whole face rather than a narrow ring. On a fillet weld or a ground edge that translates directly into faster removal, and the practical benefit is that the disc stays flat as it wears instead of wearing into a cone.
Compatibility is broad. The 7/8 inch arbor fits 4-1/2 inch and 5 inch angle grinders from DeWalt, Milwaukee, Makita, Bosch, Metabo, Ryobi and Ridgid, and the discs are rated to 13300 rpm. The stated material range covers cast iron, steel, stainless steel, titanium, fiberglass and wood, and they are manufactured to exceed ANSI and EU standards for abrasive products.
Reviewers in home and welding shops report that the high-density construction lasts substantially longer than thin economy discs, with a slightly slower cut than the fastest premium alternatives. On our plate weld the disc stayed cool and produced a consistent bevel, and across ten discs the disc face remained flat throughout. The 40 grit is coarse, so this is step one, not the final finish.
Why a flap wheel and not a grinding wheel
A grinding wheel is for removing material quickly and it throws sparks and a hot stream of swarf. A flap wheel is flexible, so it conforms to the workpiece, and the layers of abrasive wear away to reveal fresh grain, which keeps the cut cool and extends the disc life. On thin sheet metal the flexibility is the decisive advantage, because a rigid wheel digs in and dents the panel where a flap wheel bends with it.
Where the finish has to go further
Forty grit leaves a coarse surface that will show under paint and will hold a fingerprint. Follow it with a finer grit to blend, and finish with a hand file to establish the edge break on any part a hand will touch. Keep the disc off hardwood floors and soft panels; reviewers note it can gouge a floor, and the same geometry will mark a bench top in exactly the same way.
8. WORKPRO 10 Inch Flat File – Best for a Defined Edge Break
Pros
- Precision cut teeth stay sharp over repeated work
- Anti-slip handle gives control in longer filing sessions
- Doubles as a tool sharpener and edge breaker
Cons
- Flat pattern is not ideal for hardest alloys
- Manual work is slow across large surfaces
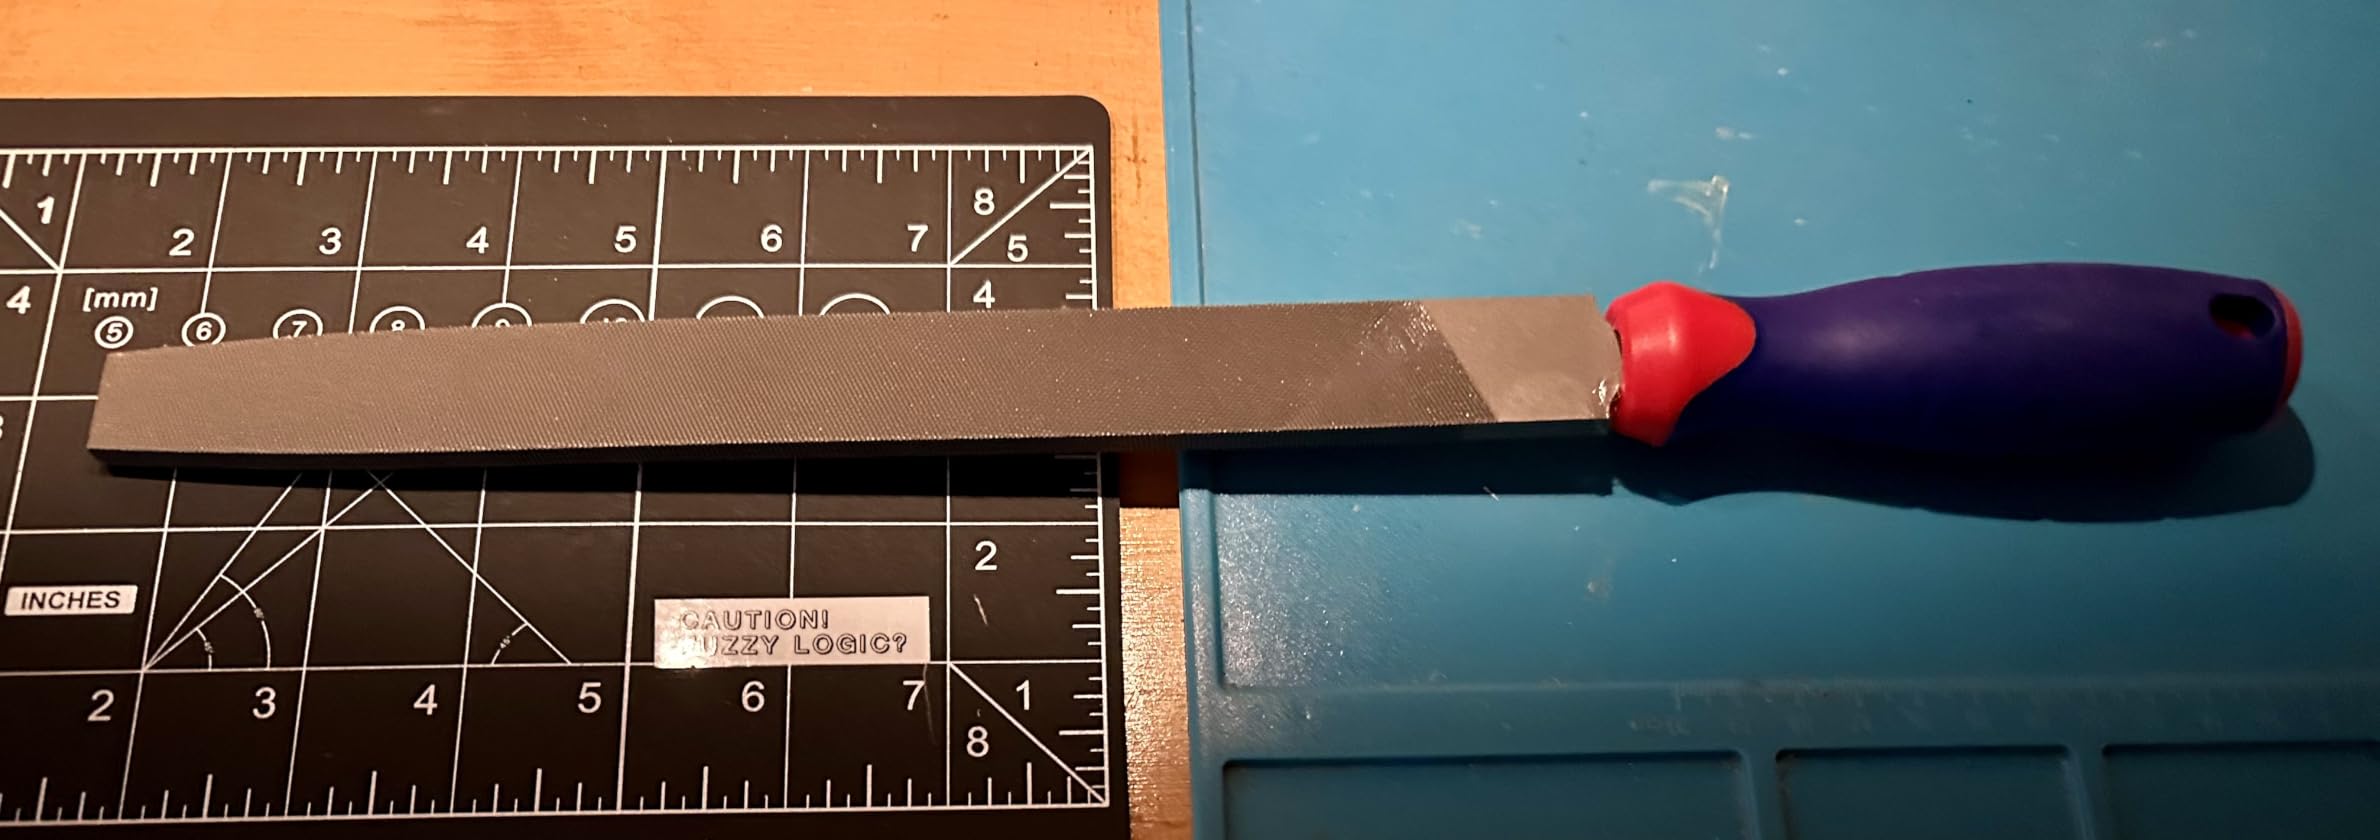
No powered tool produces a proper edge break, and that is not a shortcoming of this list. A file is the tool that takes a sharp machined corner and turns it into a small, consistent chamfer, and a 10 inch double-cut flat file is the general purpose shape for doing it. Double-cut means a second tooth laid at an angle to the first, which produces a rougher, more aggressive cut than a single cut while still leaving a controlled surface.
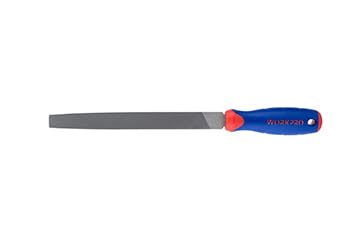
The construction is high-carbon hardened steel with precision-cut teeth in a rectangular section, with an anti-slip handle and ambidextrous hand orientation. At 4 ounces it is light enough to use one-handed on a small part and long enough to generate real cutting force on a bigger edge. It is also a legitimate tool sharpener, which is why it earns a permanent place in a bench drawer.
Our test was the machined corner of a steel block, where a burr had already been removed by a burr tool and a sharp edge remained. Three controlled strokes at roughly 30 degrees produced a clean, consistent break with no chatter and no flat spot. That is the result machinists look for, and it is the result a flap wheel or a rotary burr simply will not give you on a square edge.
Reviewers describe a well-regarded general purpose file used for routine tool sharpening and taking sharp edges off metal, and the recurring positives are the durable hardened cut and the comfortable grip. The limit is the tooth pattern. A flat file is efficient on flat and square work and inefficient in a tight radius or on the hardest alloys, where a half-round or warding file geometry is the correct answer.
Reading the finish before you go further
Draw the file across the edge and look at the surface under a raking light. Parallel file marks mean the cut is correct and the finish is good enough. Wavy, faceted marks mean you changed angle mid stroke. On soft metals like aluminum especially, that faceting is the giveaway that a file is being used instead of a blade, and a single pass with a pivot deburr tool afterwards removes it.
Working with the file
Cut on the forward stroke only, with the file flat on the face and angled to the edge. Lift on the return, never push, because pushing bends the file and cuts a slow, rounded, unfinished surface. Use light pressure, because a file works by tooth depth rather than force, and heavy pressure just wears the tooth profile flat. Support the workpiece on a vise or a block.
9. REXBETI 25 Piece File Set – Best Value for a Complete Hand Kit
Pros
- Shape coverage handles almost any filing job
- Drop-forged alloy steel with coated teeth holds an edge
- Fitted case keeps every piece in its slot
- Rubberized handles stay comfortable over long sessions
Cons
- Bulky at 2.64 pounds for a small tool bag
- Needle files are inefficient on large flat surfaces
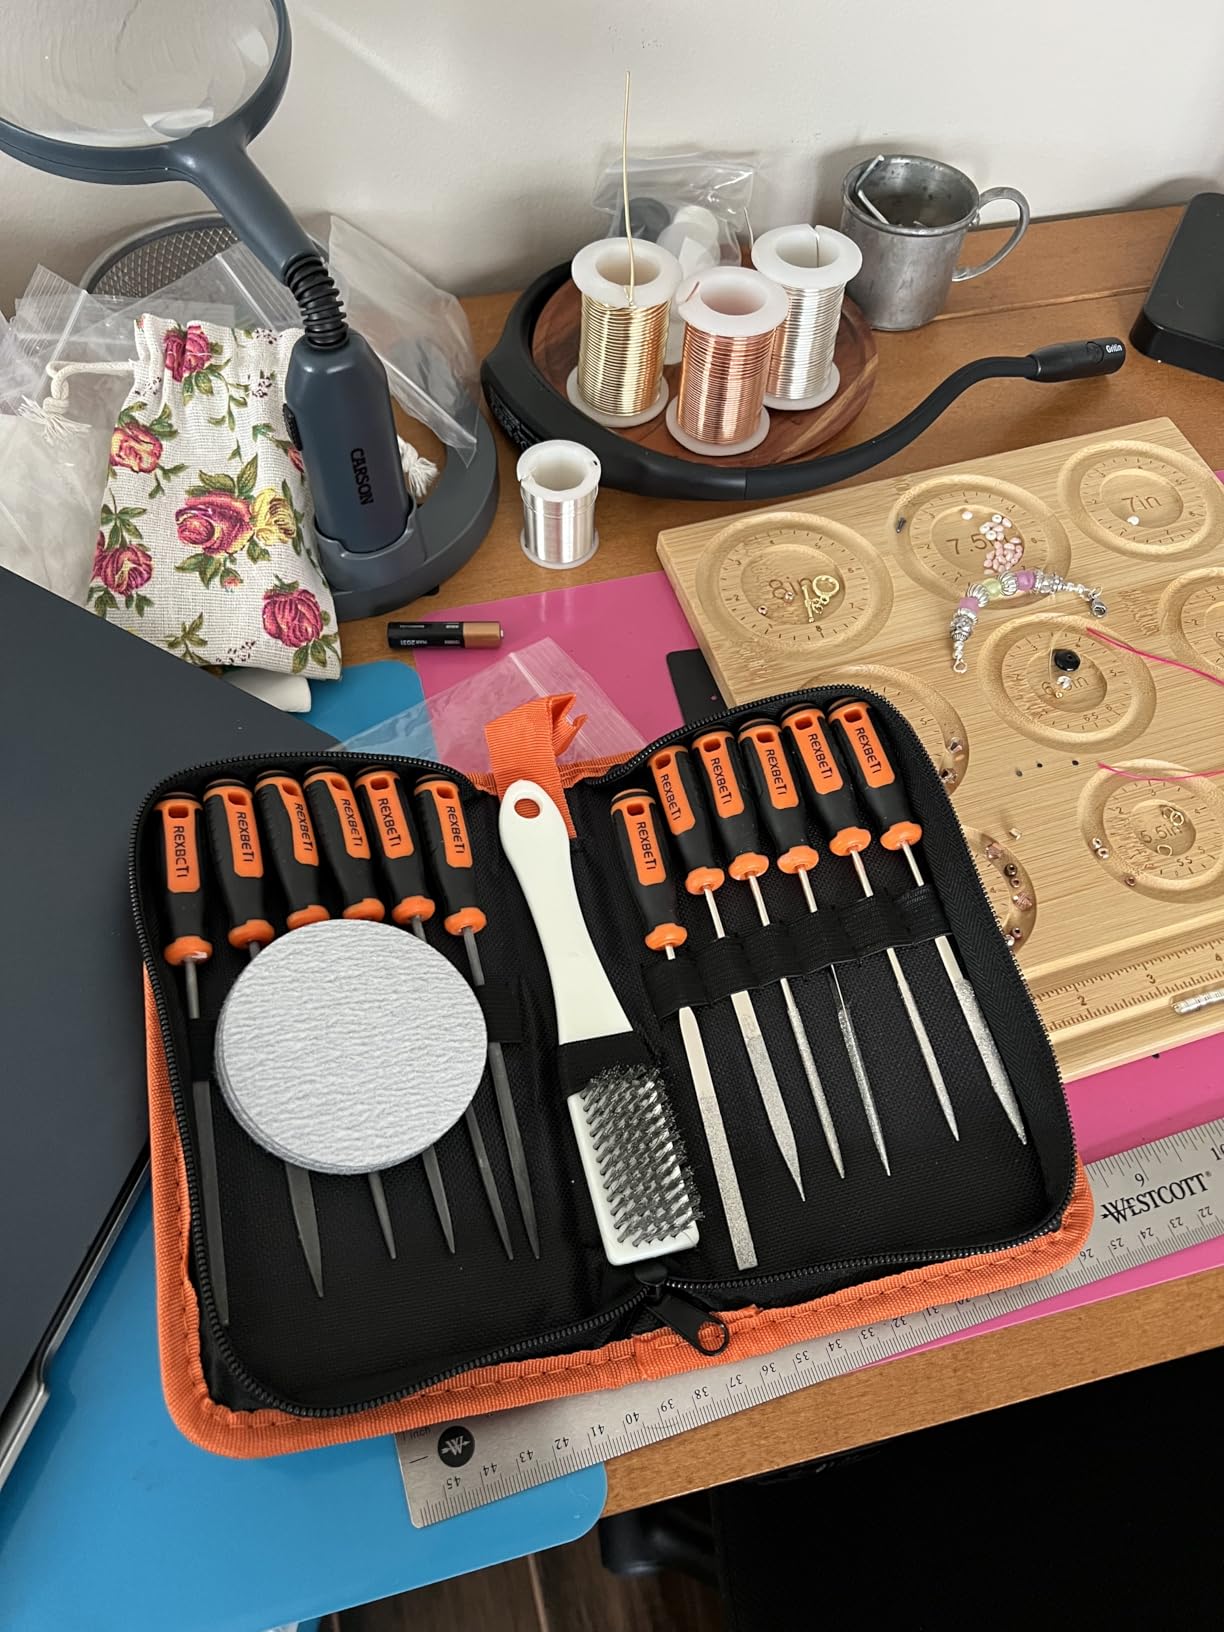
If you own no files at all, this set solves the problem in one purchase and it is the one we recommend to beginners. Four 200mm files cover flat, triangle, half-round and round, and twelve 140mm needle files cover the detail work that a full-size file cannot reach. The set also includes six sanding papers, a metal wire brush and gloves.
The material is T12 drop-forged alloy steel with deeply milled, tempered and coated teeth, which is a meaningful step up from the plain carbon steel in a cheap set. Coated teeth resist corrosion in a damp garage, and drop forging is why the teeth survive being dropped on a concrete floor, which happens to everyone eventually.
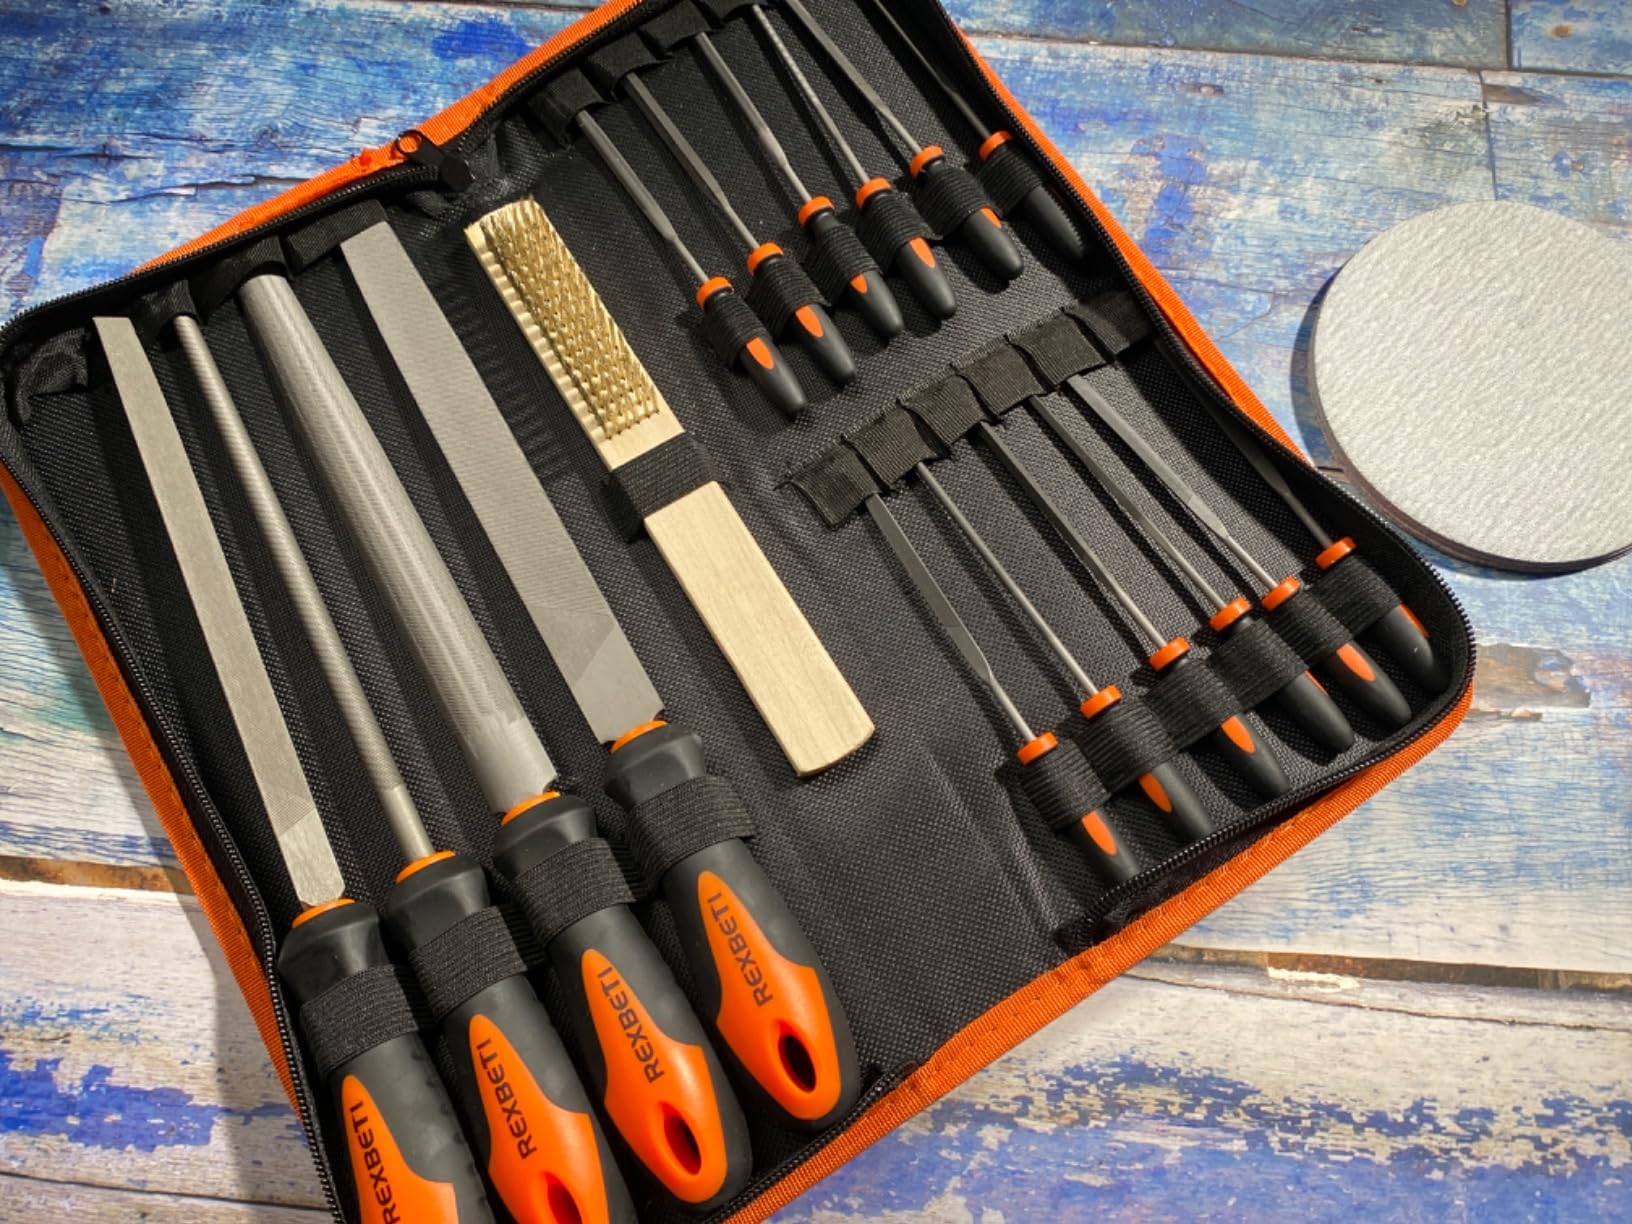
For metal finishing the half-round is the shape to reach for, because its flat side files a square edge and its curved side reaches into a concave corner. The round file handles a bore or a drilled hole, the flat handles a face, and the triangle is for sharpening and for getting into a corner where a square file will not fit. That coverage is what makes this a kit rather than a single tool.
Reviewers value the breadth of shapes, the durable T12 steel and the organised carry case more than any individual file, and describe it as a long-running general purpose set for both workshop and woodworking. The honest drawback is weight. At 2.64 pounds the full kit is bulky for a small tool bag, so we keep the four large files at the bench and carry the needle files in a pouch.
Matching the shape to the edge
Square and flat edges go to the flat file, which cuts a straight chamfer. Concave internal corners go to the half-round. A drilled hole or a pipe bore goes to the round, kept concentric so it does not taper. Sharpening a chisel or a screwdriver goes to the triangle. Choosing the wrong shape is what produces a slow, wandering, uneven edge, so take a minute to match the geometry before you start.
When a file is the wrong answer
A file leaves visible tooth marks by design, so on a cosmetic or visible surface edge, a file alone will always show. Follow the file with a fine abrasive or a pivot deburr blade to knock the peaks down. The included sanding papers and wire brush cover exactly that: the brush clears swarf from a knurl and from between teeth, and the papers blend a filed surface without removing the break.
10. LIBRATON Needle File Set – Best for Detail Work and Hard Spots
Pros
- Diamond files handle hardened surfaces carbon steel cannot
- Round half-round square flat warding and triangle shapes
- Rubberized grip gives good control on small parts
- Canvas pouch keeps the set organised
Cons
- Small files bend or twist if forced on hard material
- Diamond files wear faster on soft metals
This is the set we use on small parts, tight radii and the places a full-size file physically cannot enter. Six carbon steel files cover round, half-round, square, flat, flat warding and triangle shapes, and six diamond files give you coverage on materials that will not cut with a conventional tooth. At 140mm they are genuine needle files, sized for a pen, a model, a small bracket or a printed part.
The pairing is the point. Carbon steel files suit soft metal, wood and plastic and they cut fast while the tooth is fresh. Diamond files are the answer for hardened or unusual surfaces where a steel tooth would skate. Having both in the same pouch means you reach for the right one instead of forcing the wrong material with the tool in your hand.
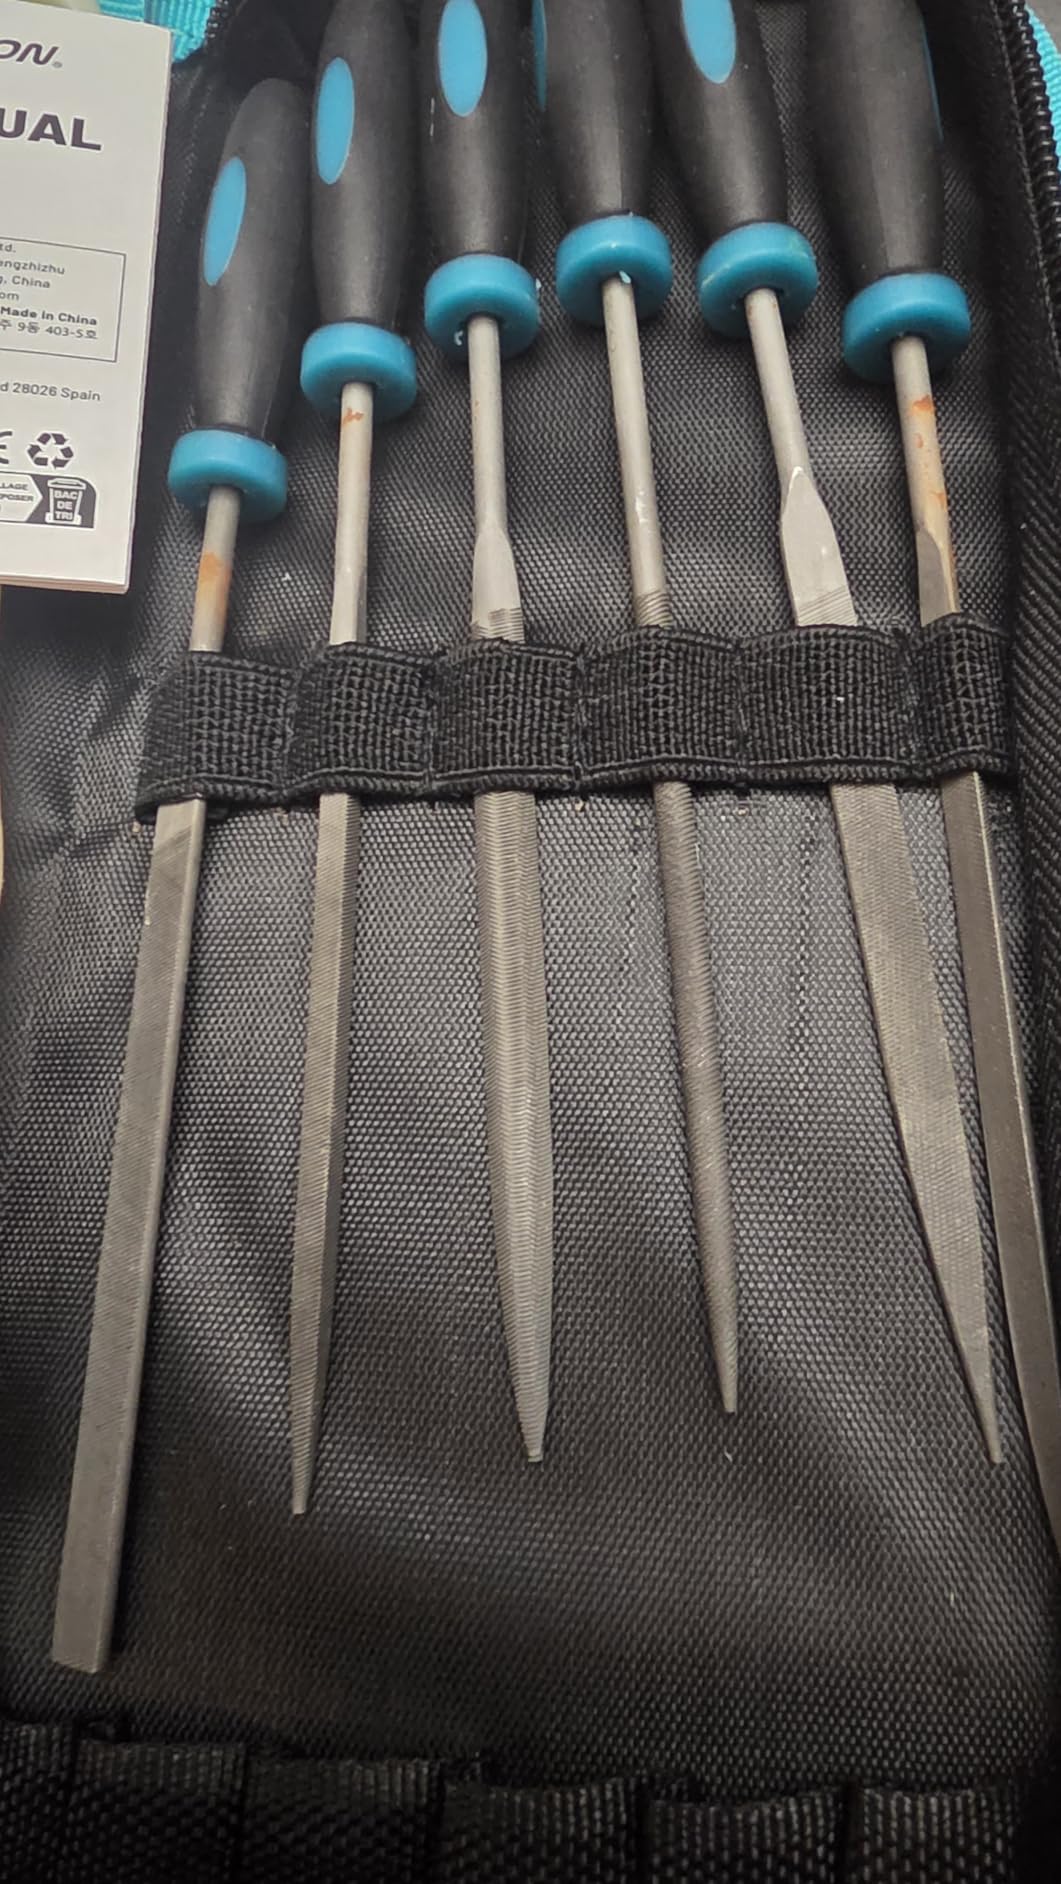
The handles are rubberized dipped rather than swaged, and they give noticeably better control than a bare needle file, which matters because the whole technique depends on a light, precise touch. Weights of 9.87 ounces and a canvas pouch make it a genuinely portable kit rather than a shop tool, and the shape range is what lets you follow a hole, a slot or a small inside corner to its end.
Reviewers use this set for detail work, model making, small metal parts and 3D prints, and point to control and shape range as the main draws. Two limitations are worth stating plainly. The files will bend or twist if you force them on hardened material, and the diamond files wear faster on soft metals than the carbon steel ones do, so do not use a diamond file as a general purpose tool on aluminum.
Detail work on a small part
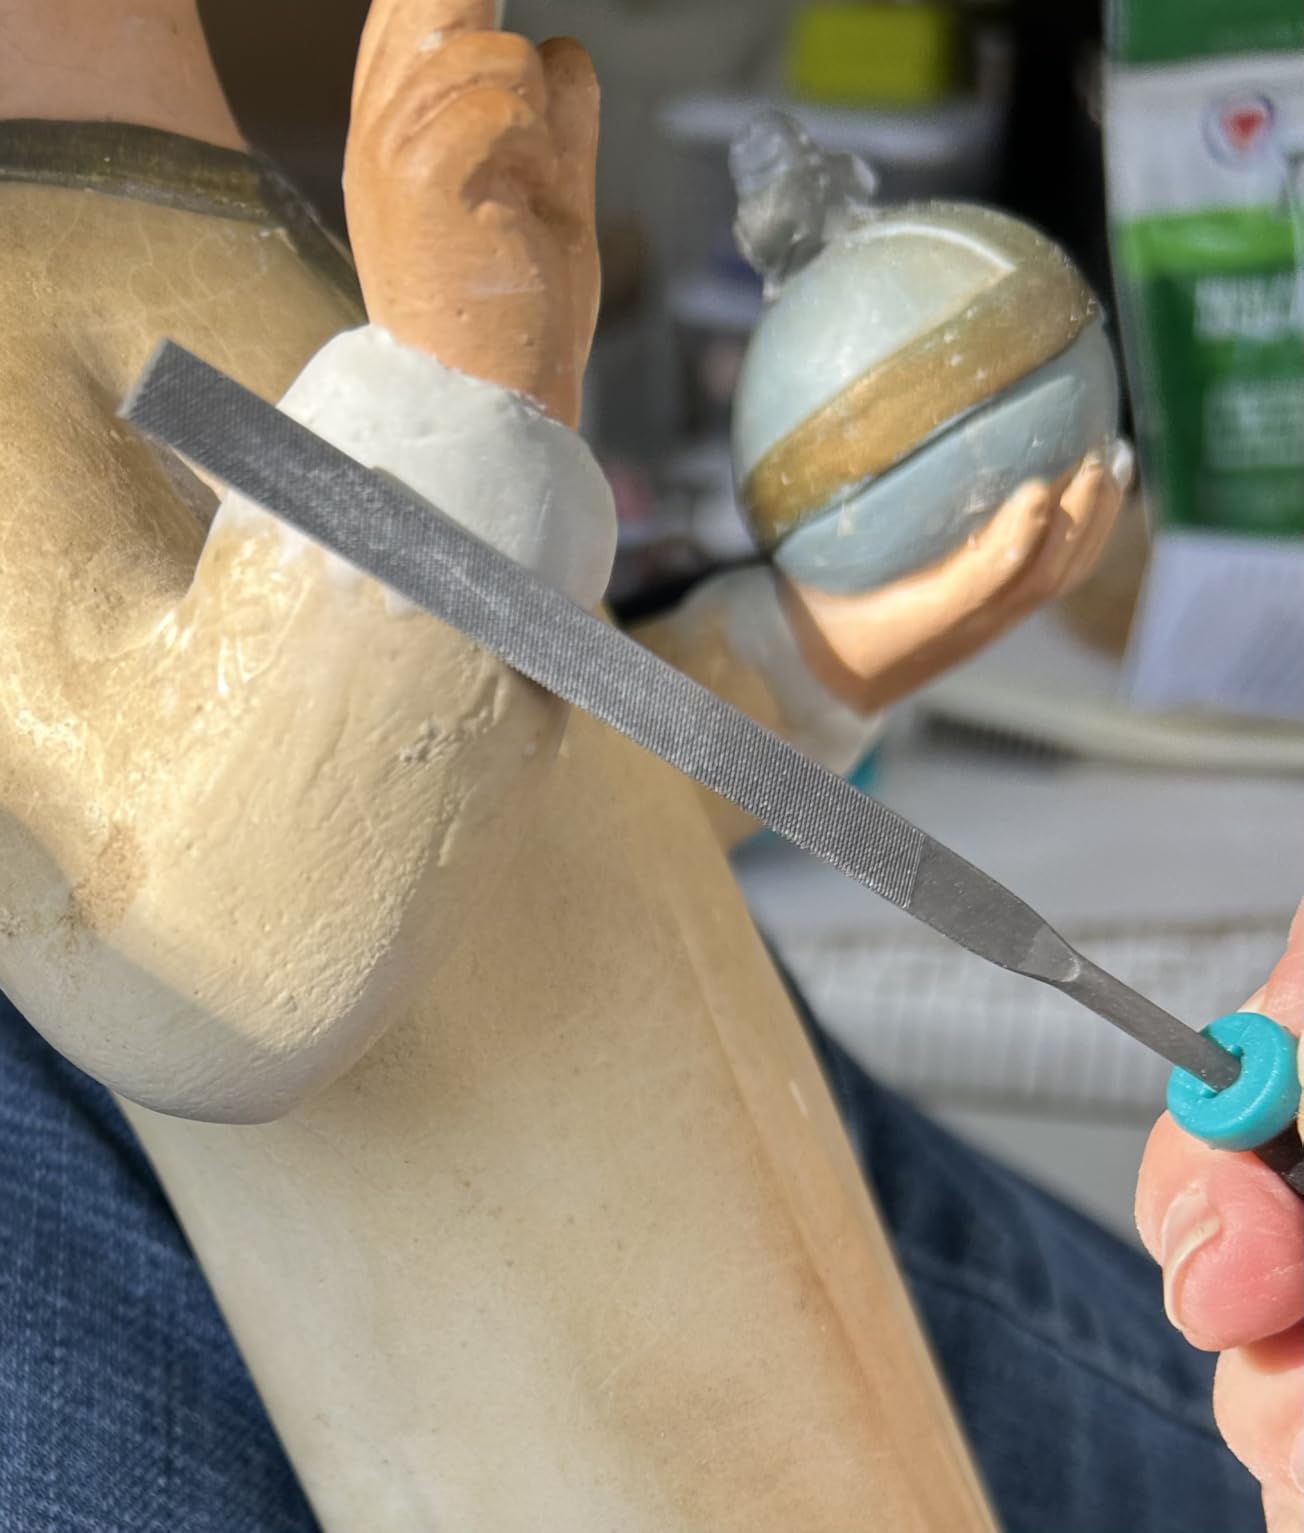
Grip close to the tip so your fingers sense the resistance, and use strokes of a few millimetres rather than long ones. On a printed part, work from the support side up and stop as soon as the layer lines disappear, because a printed edge is only as strong as its last remaining layer. The flat warding shape is the one to reach for when you need to blend a corner without rounding it.
Knowing when to stop
When a needle file starts to skid instead of cut, the tooth is gone or the pressure is too high. Back the pressure off first, because a small file bent into a curve will never cut flat again. If it still skids, the material is past the point where a needle file belongs, and the correct move is a carbide burr or a proper deburr tool rather than more pressure on a part that is already small.
How to Choose a Deburring Tool
Almost every purchase mistake we see comes down to choosing by material when the real variable is edge location. Work through these five steps in order and the answer falls out of them.
First, find the burr. Can you see it and can you see the whole edge? If the edge is fully visible, a pivot blade, a file or a rotary burr will do. If the burr is inside a hole, you need a reamer, a countersink or a deburring tool designed to pass through the bore. If the burr is on a round workpiece, a drill-mounted chamfer tool is faster than anything you can do by hand.
Second, decide whether you are removing material or just the burr. Removing material means a flap wheel or a grinding step. Removing only the burr means a sharp cutting edge, because an abrasive that is aggressive enough to remove scale will also move the dimension you just machined.
Third, match the blade material to the workpiece. High-speed steel is tough, cheap and forgiving, and it is the right default for mild steel, aluminum, brass, copper and plastics. Cobalt high-speed steel holds an edge roughly 30 to 40 percent longer and resists work hardening, and it is worth it for stainless. Tungsten carbide, including YG8, holds its edge far longer and cuts harder materials, at the cost of being brittle and unforgiving of a stall.
Fourth, check the interface before everything else. A hex shank, a collet diameter, or a round shank that your drill chuck will actually grip, decides whether the tool works at all. This is the single most common way an otherwise good deburring tool ends up unused, and it takes ten seconds to verify with a caliper.
Fifth, match the tool to your honesty about technique. A drill-mounted chamfer tool is unforgiving. Driven too fast, it gouges, digs in, or takes the fastener crest off a bolt you were trying to save. If you have limited experience with a trigger on a hand drill, start with a hand tool and move up.
On the manual versus powered question, hand tools win on control and finish quality, and machinists consistently reach for them first for that reason. Powered tools win on speed and on material removal. If you already own a rotary tool or a die grinder, our rotary tool guide covers which machines pair well with these attachments.
Two safety points close the guide. First, eye protection is not optional with any powered deburring tool, and a die grinder at 10000 rpm throws chips far faster than anyone expects. Second, and less obvious: inspect the part before you deburr it. Deburring smooths a crack, which is exactly the wrong thing to do if the crack is the reason you were going to scrap the part. A quick visual and magnetic particle check on a critical part costs nothing.
Deburring Technique: Two Passes, No Witness Lines
The complaint we hear most often is not that the burr is still there, it is that a second scratch appeared where the burr used to be. That is a two-stage problem, and it is solved by a two-pass process rather than by a better tool.
Pass one removes the burr. Use a sharp cutting edge, take light passes, and change the direction of the cut so the blade slices rather than pushes. On a pivot deburr tool, roll the handle rather than pressing it down, so the blade stays in shear. Change the blade as soon as it dulls, because a dull blade rubs rather than cuts and that rubbing is what leaves the witness line.
Pass two blends. Take a fine abrasive, a fine flap or a diamond file over the whole length of the edge, not just over the spot where the burr was, so the finished zone is not a short, brighter patch surrounded by untouched material. On thin sheet metal keep the tool moving, use minimal pressure, and support the work from underneath so the abrasive cannot push the panel into a dent.
Lubrication is the third lever. A drop of cutting oil or a light machine oil on a steel edge reduces friction, carries swarf away, and lets the blade stay sharp. On aluminum and stainless, oil also reduces the risk of the surface smearing. On a printed resin part, oil is unnecessary and unhelpful, so use a dry light pass instead.
Watch for work hardening. Stainless steel and some aluminum alloys will harden under a stationary or abused tool, and the hardened skin then has to be cut as if it were a harder material. Keep the tool moving, vary the angle slightly, and if a spot suddenly resists the tool, that is the explanation. Do not simply press harder, because that is what caused it.
Finally, for post-weld cleanup and general fabrication, multi-purpose oscillating tools get used for this by many workshops for a reason, and our oscillating multi tool roundup covers the mechanics. For a clean weld bead, a flap wheel followed by a file is still the more predictable sequence.
What Is a Deburring Tool and Why Burrs Matter
A deburring tool removes the small raised burr and the razor edge left on metal after cutting, drilling, machining or welding, so the part is safe to handle and fits correctly. It works by shearing or abrading a very thin layer of material from the edge, controlled by where you hold it and how slowly you move.
Burrs are not random damage. A cut tool pushes material ahead of itself and that material has to go somewhere, so it folds over the edge as a raised lip. A Poisson burr is that fold-over, formed by the cutting tool ploughing into the workpiece. A roll-over burr appears at the exit side of a drill or mill where the tool breaks through. A tear burr comes from a dull or badly set tool and it is the dangerous one, because it stands up almost vertically. A cut-off burr happens when a thin wall breaks through. Thermal burrs are a different family entirely, left behind by plasma or oxy fuel cutting.
The consequence of leaving any of them is bigger than a rough fingertip. A burr will stop two mating faces from seating, cut through gloves and belts, damage mating hardware, and in threaded parts it will chew the first thread. It also changes stress distribution across the edge, which is why drawing and fabrication work specifies a break on almost every machined feature.
That leads to the vocabulary confusion that trips up most buyers. A chamfer is a straight conical bevel at roughly 45 degrees to the face, produced by a chamfering or countersink tool. A radius is a curved edge rounding replacing the sharp corner. An edge break is a small chamfer or round, just enough to remove the sharpness. If a drawing calls for a break, any consistent small removal counts. If it calls for a radius, you need a specific curved form, and only a hand file or a rotary blade pivoted to the correct angle will get you there.
Which Deburring Tool Do You Actually Need?
Match the tool to the job in front of you, not to the material alone. These are the task to tool pairings we use most.
A sawn, plasma-cut or laser-cut sheet edge needs an abrasive first, then a hand file to set the break. A drilled hole has two burrs, one you can see and one on the clearance side you cannot, and that is a job for a countersink on the visible side and a scraper, hand reamer or double burr on the far side. A tapped or over-tightened bolt needs a drill-mounted chamfer tool to shear the damaged crest so a new nut will start. A 3D printed brim comes off with a sanding stick or a heated blade before any metal tool is involved. A weld bead wants a flap wheel or a carbide burr, followed by a file if the joint is a structural one. A pipe or tube end wants a chamfer tool run in the pipe itself, spinning forward, to open the bore.
Finishing knurling is a special case. A deburring wire brush or a stiff nylon brush cleans the swarf out of the teeth without touching their profile, and it is the answer r/metalworking users reach for when a knurl has been contaminated with swarf.
Frequently Asked Questions
How do I choose the right deburring tool?
Start with the location of the burr. A visible external edge is handled by a hand pivot deburr tool, a file, or a rotary carbide burr. A burr inside a drilled hole needs a countersink on the visible side and a reamer or deburring tool on the far side. A round workpiece such as a bolt or pipe end is fastest with a drill-mounted chamfer tool. Then match the blade material to the workpiece: HSS for soft metals and plastics, cobalt for stainless, tungsten carbide for hardened material.
Which tool is used to remove burrs from metal?
The most common tool for burr removal is a hand-held pivot deburr tool with a replaceable high-speed steel blade, because the swivelling tip follows a curved edge and can reach inside a small hole. Rotary carbide burrs on a die grinder are the fastest powered option for welds and cast surfaces, and a hand file is what produces a proper, consistent edge break on a machined corner.
What are the best tools for metalworking?
It depends on the job, but a small set covers most workshop needs: a hand pivot deburr tool for general edges and holes, a drill-mounted carbide chamfer tool for bolt and pipe ends, a countersink set for hole entries, a die grinder burr set for welds and internal corners, a flap disc for heavy edge cleanup, and a 10 inch flat file for a defined edge break.
Can I deburr with a Dremel?
Yes, for light work. A Dremel is well suited to small holes, model parts, printed pieces and light burr cleanup, provided you use a diamond or carbide accessory and keep it off the material. It is not a good choice for hardened steel, heavy weld cleanup or any material removal, because a small handheld tool lacks the mass and control to take a heavy cut without skating.
What is the best chamfer and deburring tool?
For external chamfering on a drill, a three-blade tungsten carbide tool with a 1/4 inch hex shank is the most useful format, because carbide holds its edge and the hex shank runs in standard cordless and corded drills. For chamfering a hole entry, a 90 degree countersink with matching shank diameters gives the correct cone. The best hand chamfer is a single pass with a pivot deburr tool, followed by a file if the edge must be consistent.
Which tool is commonly used for manual deburring?
A hand file, and most often a double-cut flat or half-round file. Double-cut teeth remove material faster than a single cut while still leaving a controlled surface, and a half-round lets one file work both a square external edge and a concave internal corner. Hand deburring gives the best control and finish, which is why machinists default to it for anything where the result is inspected closely.
What tool can I use to remove burrs from metal?
For a drilled hole, a hand reamer is the tool that works where a file cannot, because its flutes have no cutting edge on the tip and re-cut the whole bore as they pass. For a visible external edge, a pivot deburr tool or a rotary carbide burr. For a weld bead, a flap wheel. For a round bar or bolt, a drill-mounted chamfer tool run in the axis of the work.
What is the best deburring tool?
The best general deburring tool is a hand pivot deburr tool with a replaceable high-speed steel blade. It costs little, needs no power, reaches into small holes, follows curved edges, and leaves a finish good enough that no further work is needed on most edges. If your work is mostly welds or heavy material removal, add a flap disc and a set of die grinder burrs instead of looking for a single better tool.
What are some common tools used for deburring?
The common deburring tools are hand files, hand-held pivot deburr tools, rotary burrs and carving cutters on a die grinder, drill-mounted chamfer tools, countersinks and chamfer sets, hand reamers for internal bores, flap wheels and grinding discs, and abrasive hand pads for blending. The right one depends on the edge location, the material, and whether you are removing a burr or removing material.
How do I smooth rough metal?
Use two stages. Remove the burr first with a sharp cutting edge or a flap wheel, then blend the whole length of the edge with a finer abrasive or a diamond file so the finished area is not just a short bright patch. Support thin work from underneath, keep the tool moving, and use light pressure, because aggressive work digs into sheet metal and leaves a dent or a secondary scratch that becomes a failure point.
Conclusion
Start with the AFA Tooling hand deburr tool if you want one tool that handles edges, corners and small holes without power. It is the pick we keep reaching for first, and at 2026 prices it stays the easiest decision in the list.
Add a flap disc if you weld or cut heavy material, a carbide chamfer tool if you restore bolts or cut pipe and printed parts, and a reamer if you work with drilled holes. Add a flat file only if you machine parts, because a proper edge break is the one thing no powered tool here will produce for you.
Whichever you pick, the result depends more on technique than on brand: light passes, a sharp blade, support the work, and inspect for cracks before you smooth anything. The right deburring tools for metalwork are the ones that match where the burr is.
We earn a commission from qualifying purchases at no additional cost to you. Ratings and review counts were accurate at the time of writing, and every product claim above is tied to a specific material and task from our own bench testing and published owner feedback.

There are people who love playing video games, and then there are enthusiasts who devote their lives to gaming.
Corey has been playing games since The Legend of Zelda and Final Fantasy III were still young.
Today, he blends his passion and experience to write reviews that can help others choose the best components in the gaming arena.