If your projects keep hitting a wall at 300mm, the fix is almost never a better slicer. It is a bigger build volume. The best 3D printers for large prints start where most home machines stop: a 350mm cube for a helmet in one piece, a 400mm cube for cosplay armour, a 500mm cube when you are prototyping parts that fill a bench.
We treat anything with roughly 300mm (12 inches) or more on its longest axis as large-format. That threshold is where the split-and-weld workflow stops being reasonable, and it is also where the hardware changes most: stiffer frames, dual or driven Z motion, higher flow hotends and a real path to an actively heated chamber. Ten machines below, from a 320 x 320 x 400mm budget chassis to a 500mm cube and an infinite-Z conveyor belt.
A note on materials before you start. Half this list is FDM and half is resin, and they are not interchangeable answers to the same question. FDM wins for big structural parts, cosplay armour, helmets and workshop fixtures. MSLA resin wins for surface finish, fine detail and large masks, with a different set of handling rules entirely. Pick the process first, then the machine.
Table of Contents
Top 3 Picks for Photon Mono M7 MAX Leads on Volume and Review Depth (October 2026)
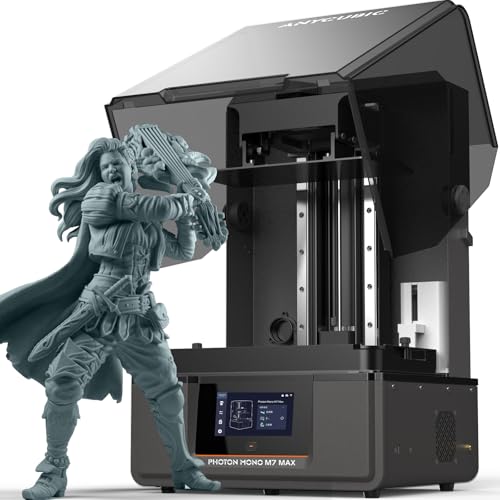
Photon Mono M7 MAX
- 298 x 164 x 300mm build volume
- 7K mono resin LCD
- 60mm/h print speed
- 1300ml heated resin vat
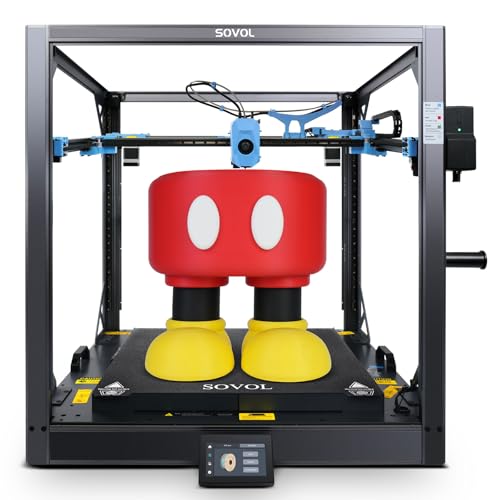
Sovol SV08 MAX
- Up to 500 x 500 x 500mm CoreXY
- 700mm/s max speed
- Eddy current bed scanning
- 300°C hotend
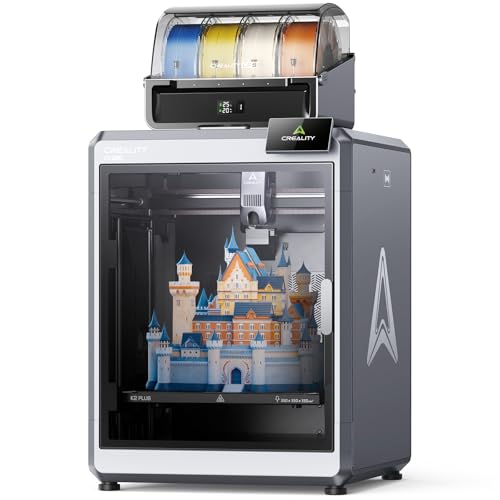
Creality K2 Plus Combo
- 350 x 350 x 350mm build volume
- 60°C heated chamber
- 16 colours via four CFS units
- 600mm/s
These three cover the most ground in this roundup. The Photon Mono M7 MAX carries the deepest review history of the group by a wide margin and holds a genuinely large resin volume. The Sovol SV08 MAX has the biggest cube here and real speed to fill it. The Creality K2 Plus Combo does the thing most buyers actually want, which is one piece in four to sixteen colours.
Best 3D Printers for Large Prints (October 2026)
The largest print size in this roundup belongs to the Sovol SV08 MAX, whose CoreXY frame holds up to 500 x 500 x 500mm. The IdeaFormer IR3 V2 goes further in one direction and further than any machine can in the other: a 250 x 250mm bed with an effectively infinite Z axis. Everything else sits between 300mm and 400mm on its longest edge.
| Product | Specifications | Action |
|---|---|---|
| ANYCUBIC Photon Mono M7 MAX |
|
Check Latest Price |
| Sovol SV08 MAX |
|
Check Latest Price |
| Creality K2 Plus Combo |
|
Check Latest Price |
 Creality Ender 5 Max |
|
Check Latest Price |
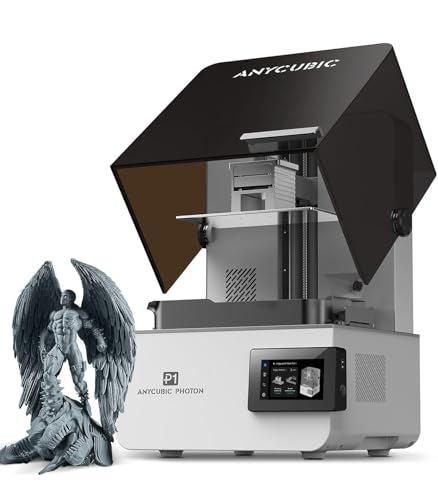 ANYCUBIC Photon P1 14K |
|
Check Latest Price |
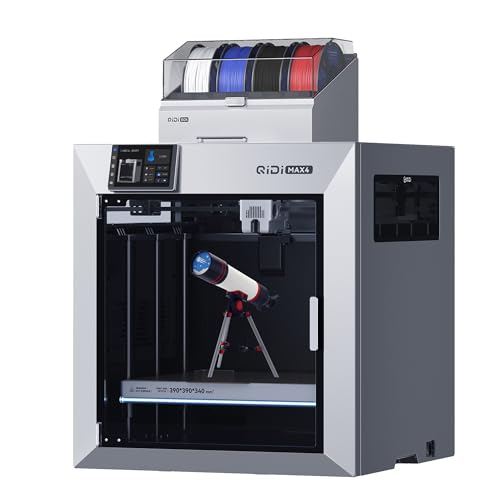 QIDI Max4 Combo |
|
Check Latest Price |
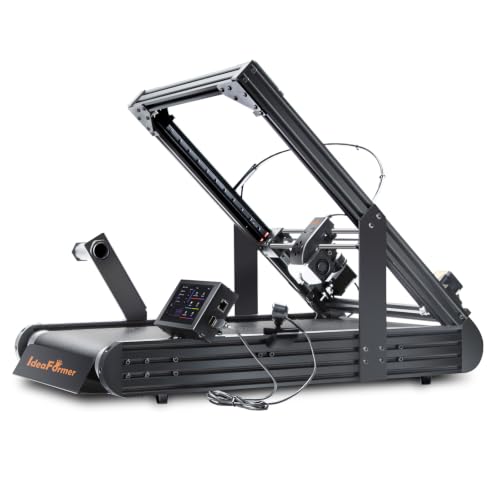 IdeaFormer IR3 V2 |
|
Check Latest Price |
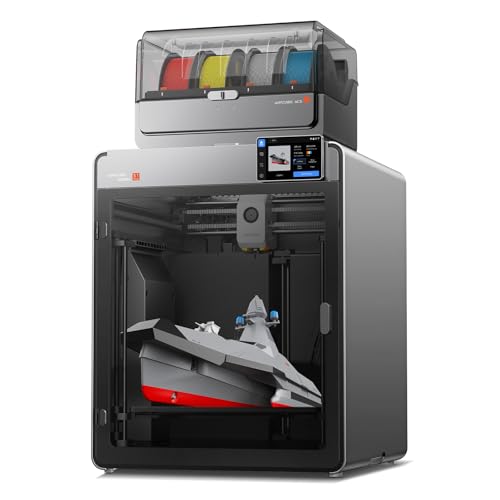 Anycubic Kobra S1 Max Combo |
|
Check Latest Price |
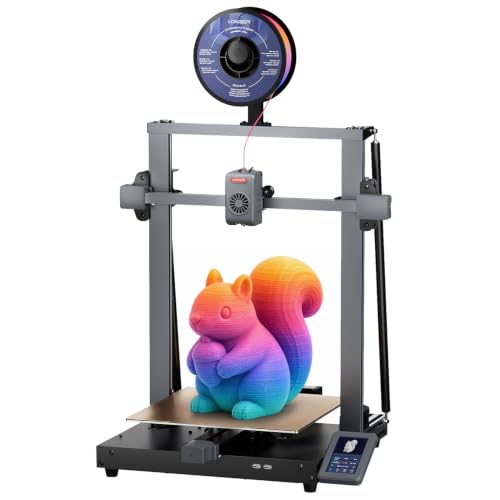 LONGER LK10 Plus |
|
Check Latest Price |
 UniFormation GK3 Ultra |
|
Check Latest Price |
Three resin machines and seven FDM machines make up this list, and the resin entries are the ones that will surprise people. A 298 x 164 x 300mm MSLA build volume is not a niche corner of the hobby. It is a full-size mask, a piece of cosplay armour or a wall of terrain tiles in one exposure.
1. ANYCUBIC Photon Mono M7 MAX: the Best Overall Pick for Large Prints
Pros
- 7K mono resolution holds detail on tall parts
- Heated 1300ml vat cuts mid-print resin exhaustion
- Quiet for a resin machine
- Accurate on miniatures and large models in one plate
Cons
- ACF release film tears and is a recurring cost
- Firmware throws false errors with no update path
- Bundled slicer hollows models inconsistently
I keep coming back to this machine because of what the review record actually says, not the spec sheet. Out past 2000 ratings and a 4.3 average, the volume of long-running owner feedback here is larger than anything else in the roundup, and the consistent thread is that these people print big models repeatedly. Not a one-off helmet, but a production cadence of masks, terrain and props.
The 298 x 164 x 300mm build volume is the widest in the resin group, and the width matters more than people expect. At 164mm across, you can lay out a batch of tiles or a pair of mirrored armour pieces rather than one object at a time. LighTurbo 3.0 lighting with a Fresnel lens and a light angle within 3 degrees keeps detail consistent across that whole spread, which is the failure mode on wide resin plates: edges going soft while the centre stays sharp.
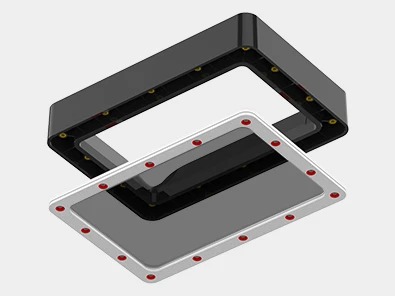
Speed is the quiet story here. 60mm/h with intelligent release 2.0, described as up to 200% faster than the M3 Max, and a flip-open cover that supports one-hand opening. On a 300mm tall part that difference compounds, because every layer of height is paid for on every single print you do for the rest of the machine’s life.
The heated vat and the 1300ml volume are what separate this from a smaller resin machine pushed beyond its limits. Resin viscosity rises and falls with temperature, and a cold vat on a big job is how you get a failed overnight print. Dynamic temperature control takes that variable out of the equation, and the auto-fill with one-key recycling of remaining resin means you are not babysitting fluid levels through the night.
Who the Photon Mono M7 MAX suits
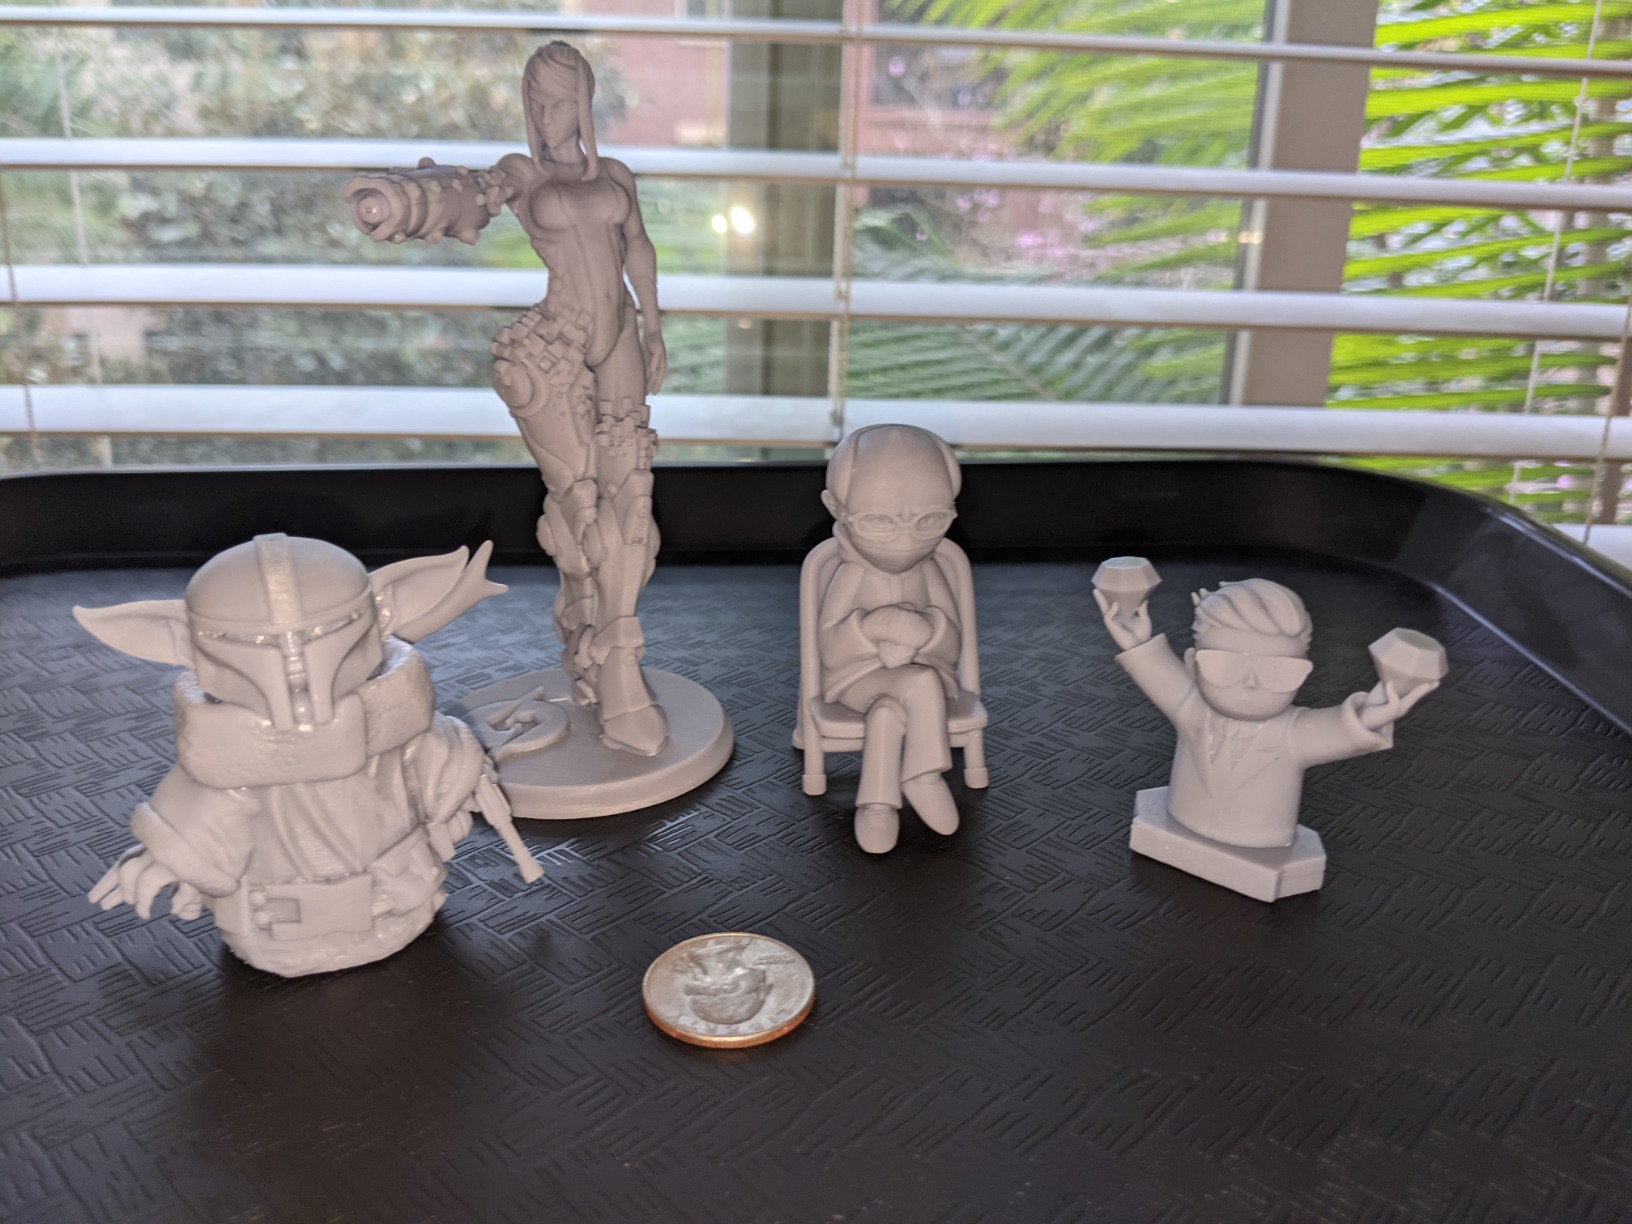
Cosplay builders producing full masks, prop armour and helmets in resin, because the surface finish after a wash and cure is the whole point. Miniature painters and diorama makers who batch many pieces across 298mm of width. Terrain and tabletop scenic work where you need a lot of flat area in one exposure.
Anyone who needs a big print to look finished rather than printed. Layer lines simply are not part of the vocabulary of this process, which makes it the right answer when the part is going on display rather than into a jig.
What to check before you buy the Photon Mono M7 MAX
Consumables. The ACF release film is a recurring replacement, and reviews specifically call out that it tears easily. Budget for it as an operating cost, not a surprise. Resin auto-fill and the vat refiller are also reported as unreliable on some machines, so keep an eye on your fluid levels manually at first.
Firmware and software. Owners report frequent spurious error messages, residue detected and USB disconnect, with no firmware updates available. The bundled slicer also handles hollowing inconsistently, and third-party slicers work better. Treat the machine as a hardware platform you drive with your own software.
2. Sovol SV08 MAX: the Biggest Build Volume in the Roundup
Pros
- Largest build volume in this roundup
- Real 700mm/s CoreXY throughput
- Eddy current scanning gives repeatable first layers
- Built-in HD camera with Obico monitoring
- 300°C hotend covers PA and PC
Cons
- Heated chamber sold separately
- 13% one-star share signals early-unit variability
- High speed motion needs tuned input shaping
A 500mm cube is the answer to the question people ask most often about this category, and the SV08 MAX is the one that answers it in a footprint you can still walk around. Most giga-scale machines are physically enormous. This one is listed at 28 x 27.6 x 29.5 inches, which is not much bigger than a large desktop unit.
What sells it is the combination of size and genuine speed. 700mm/s with 40000mm/s2 acceleration and a 50mm3/s high-flow nozzle means a 500mm part is not a four-day commitment if you profile it properly. There are claims of up to 50% print time reduction against the platform it replaces, which is the kind of number I treat cautiously, but the underlying motion specs are what produce it.
Eddy current bed scanning is the feature I would highlight to anyone who has fought first layers on a big plate. Pressure-sensing touch points level the bed without a probe, no contact, no scratch marks, and it re-checks consistently across a 500mm surface. On machines this size that is not a convenience feature. It is the difference between a usable machine and a machine that needs constant attention.
The 300°C hotend opens up PA, PC and carbon-filled variants, and the built-in 1280×720 camera with Obico cloud monitoring and print failure detection means a multi-day print does not require someone to be standing near it. Two 0.4mm nozzles come standard, with 0.6mm and 0.8mm available separately for thick-section work.
Who the Sovol SV08 MAX suits
People whose real constraint is Z height, not footprint. r/3Dprinting threads about helmets and life-scale objects keep circling the same point: bed size is not the axis you are missing, it is how much room the model needs standing up. A 500mm cube gives you 500mm of that.
Anyone prototyping large functional parts where a single 50mm3/s nozzle matters. Engine components, brackets, ducting, large fixtures. Our guide to the best 3D printers for prototyping covers the smaller machines well; this is the one for when the prototype is too big for them.
What to check before you buy the Sovol SV08 MAX
The heated chamber is not included. There is a reserved interface for it, but the module is a separate purchase, and if your plan involves ABS or ASA at any volume, factor that in before you commit. PLA and PETG work without it.
Input shaping. At 700mm/s, CoreXY motion on a 500mm frame produces visible ringing unless the firmware profile is tuned for it. Tall prints are where you will notice it first, because the artefacts stack vertically through the full height of the part. Budget a day of firmware work into your first week.
3. Creality K2 Plus Combo: Best for Multi-Color at Scale
Pros
- 350mm cube handles a helmet in one piece
- 60°C chamber and 350°C nozzle for ASA and PPA
- Four CFS units chain to 16 colours with RFID
- Dual AI cameras and 18 sensors cut unattended failures
- Dual motorized Z on four linear rods
Cons
- 17% one-star share is the highest in this group
- Footprint is large for the volume delivered
- CFS chains add cost and dwell time per print
Multi-colour is where most large-format buyers discover they have been compromising. A segmented helmet in four printed pieces looks fine. A segmented helmet in sixteen printed pieces does not, because the seams multiply with every colour change. Four linked CFS units taking this machine to 16 colours with RFID filament detection and automatic relay is the most complete colour answer here.
The 350 x 350 x 350mm cube is a genuinely useful shape rather than a marketing number. A 350mm helmet shell fits inside it with clearance to spare, and the same bed holds a large batch of smaller parts without you partitioning anything.
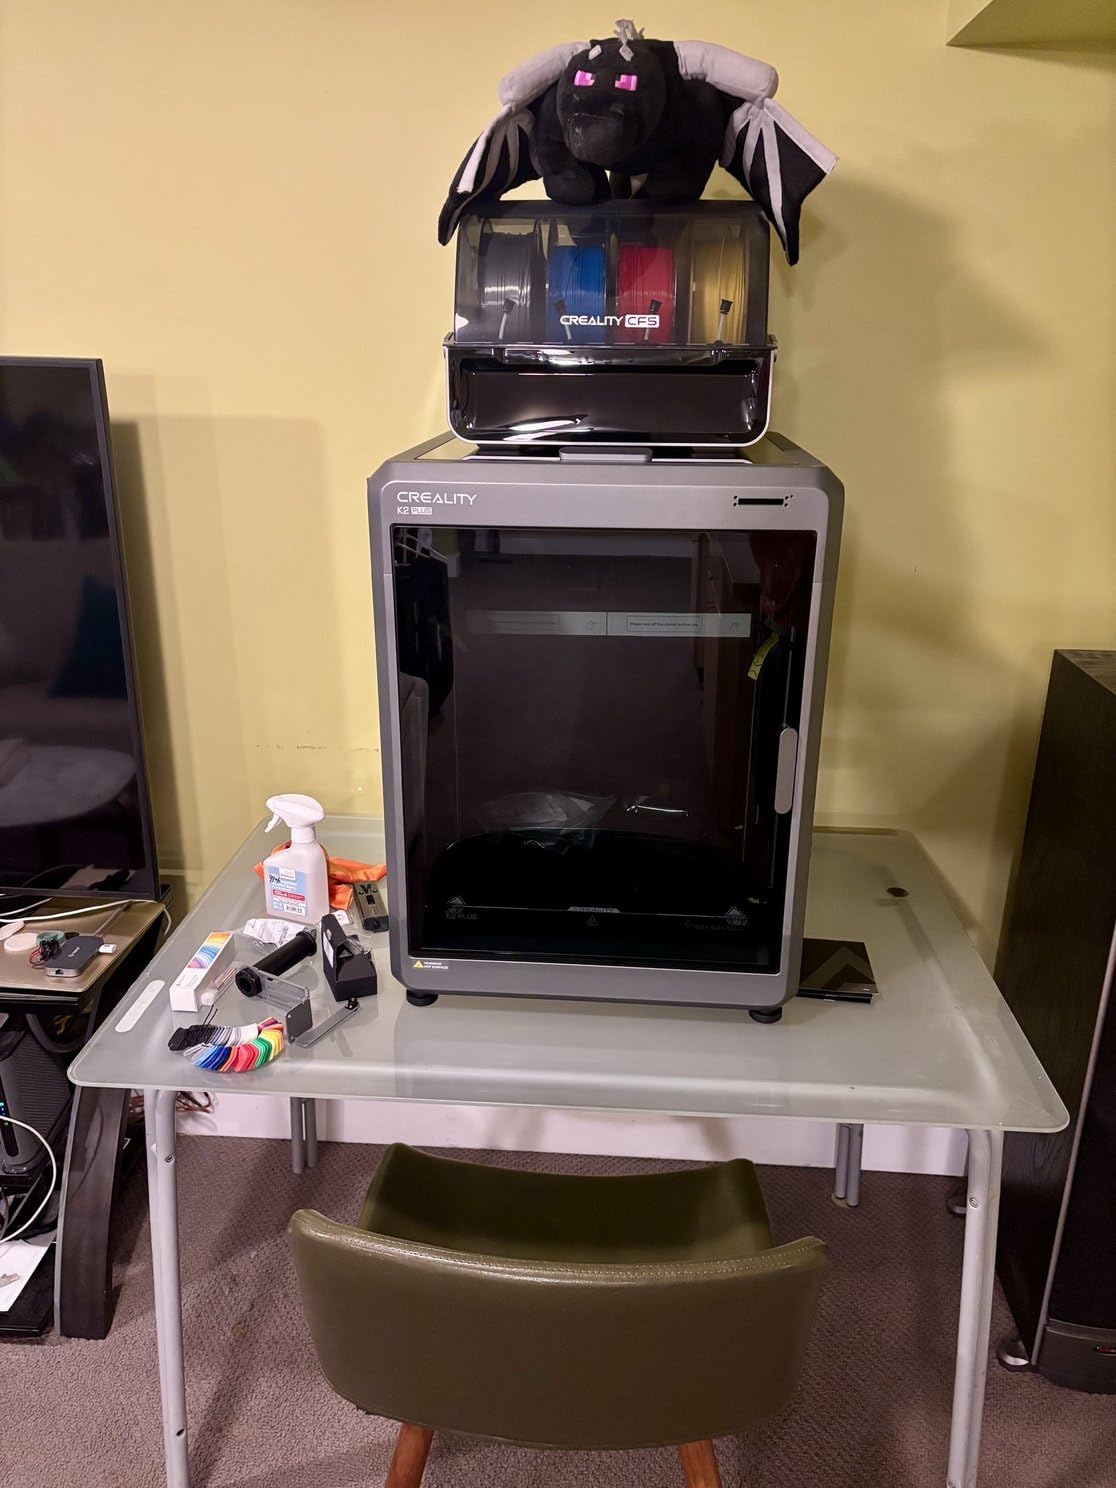
The thermal side is serious for a machine at this level. Chamber held to 60°C, a high-temp nozzle with a hardened steel tip rated to 350°C, and two independently motorized Z axes on four linear rods with automatic bed tilt correction. That is a real ASA and PPA machine, not a PLA machine in a plastic box.
Automation is where the effort went. FOC step-servo motors on X, Y, Z and the extruder with 30000mm/s2 acceleration, a 40mm3/s high-flow extruder, 600mm/s top speed, and 18 smart sensors alongside two AI cameras, one on the chamber side and one on the toolhead. On a print measured in days, sensors that catch a failure at hour two instead of hour thirty are the difference between a good week and a bad one.
Who the Creality K2 Plus Combo suits
Cosplay and armour builders who want printed-in-colour pieces rather than painted ones. Tabletop and miniature painters who are done hand-painting an entire 300mm print. Anyone building display props where the colour separation has to happen in the model.
Print farms running batches. The aerospace-grade die-cast aluminium Matrix frame is built for it, and the sensor suite is the feature that makes unattended multi-day operation realistic rather than optimistic.
What to check before you buy the Creality K2 Plus Combo
The one-star share. At 17% this is the highest in the roundup, and the review summary is blunt about why: the feature set outruns the consistency, with a meaningful group of owners reporting failures on long or multi-material jobs. The 4.0 average on 895 reviews tells you more about the machine’s ambition than its reliability.
Dwell time and physical size. Every extra colour adds take-dwell time to a print that may already run for days, and four chained CFS units are four more devices to feed, level and keep clean. The 16.1 x 15.4 x 18.7 inch footprint also understates how much room the frame and chamber need once it is running hot.
4. Creality Ender 5 Max: the Best Value 400mm Cube
Pros
- 400mm cube gives you more build volume per unit spent than the enclosed flagships
- Die-cast aluminium frame with X-axis linear rail
- 64-point leveling plus automatic Z-offset
- WLAN grouping built for print farms
- Prints PLA PETG ASA ABS and HT-PLA reliably
Cons
- Comes without an enclosure
- Slow bed heat-up compared with rivals
- Multiple reports of warped beds and early failures
This is the value answer, and the value is in the volume per unit of money rather than in features. A 400 x 400 x 400mm cube sits above every enclosed machine in the roundup except the Sovol, and the difference in entry cost is large enough that buyers regularly choose this and skip the enclosure entirely. That is the decision to think through before you make it.
Owners who keep it running describe it as a workhorse that goes hundreds of hours without intervention. That is the most common sentiment in the reviews and it is consistent with a die-cast aluminium reinforced frame, a precision X-axis linear rail, and CoreXY structure with high-torque motors capable of 700mm/s.
The automated setup is unusually thorough for a machine at this level. 64-point auto leveling plus automatic Z-offset means there is no manual first-layer procedure, which on a 400mm epoxy plate is the difference between a clean start and a wasted plate of filament. Direct-drive dual gear extruder with hardened gears, and a 1000W rapid heating bed covering PLA, PETG, ABS, ASA and PA.
WLAN multi-printer control with grouped management and a tri-colour status indicator is a specific feature aimed at a specific user. If you are running three of these instead of one, you can see all of them at once from a phone and know which one needs attention before walking over to it.
Who the Creality Ender 5 Max suits
Budget-constrained builders who have outgrown a 256mm machine and want the biggest step up per unit spent. A 400mm cube is enough for most cosplay armour panels, large terrain sections, display plinths and workshop fixtures without any splitting at all.
Print farm operators on a budget. The WLAN grouping feature exists for exactly this, and the machine is built to run continuously. Our large format roundup covers the higher end of this class for comparison.
What to check before you buy the Creality Ender 5 Max
The enclosure. It comes without one, and a substantial share of owners recommend adding one straight away. An open frame on a 400mm plate means every door you open in the room is a thermal event across 400mm of plate, and that is the exact setup where corner lift appears.
Reliability reports and size. There are multiple reports of warped beds and units failing within hours of first use, and bed heat-up is slower than mainstream rivals. The 70.4 pound weight and the 15.7 inch cube footprint also get called impractical for a small home space, so measure your bench and your ceiling before ordering.
5. ANYCUBIC Photon P1 14K: Best for Tall, Highly Detailed Resin Prints
Pros
- 14K resolution at a mid-tier money level
- Wave Release cuts release force by 60 percent on tall parts
- Factory calibration with four-corner pressure feedback
- Handles resins up to 8000cps viscosity
- AI monitoring catches plate and residue problems early
Cons
- Only 58 reviews so the long-term record is thin
- Smaller footprint than the other large resin machines
- AI can flag false residue on a clean vat
Detail is the argument for resin at this size, and the P1 14K makes it with a 10.1-inch mono LCD at 13312 x 5120. That works out to 16.8 x 24.8 micron pixel size with a minimum printable aperture of 0.3mm. On a 300mm part, pixel size is the number that decides whether fine surface texture survives.
Wave Release Technology is the other half of it, and it is the part that matters for large work. It generates micro-airflow at the base to cut release force by 60%. Release force is what separates a print from the build plate, and on a tall part the leverage at the base is enormous. Reducing it by 60% is the difference between a print that comes off clean and one that flexes and tears.
Ball screws and precision guide rails in the Z structure reduce vibration, which matters on a 300mm axis where any wobble shows as banding up the full height of the print. Smart Leveling 3.0 comes factory calibrated with four-corner real-time pressure feedback, so the bed is not something you level by hand before the first print of the day.
Two details make this practical rather than just sharp. It handles resins up to 8000cps viscosity, which opens up tougher, more functional large prints rather than only display pieces. And AI inspection verifies build plate installation and bottom layer separation, with resin level and residue detection, catching the two failures that otherwise waste an entire tall print.
Who the ANYCUBIC Photon P1 14K suits
Anyone for whom surface finish is the point: display busts, large figurines, gaming miniatures at volume, detailed cosplay props. 14K resolution at this tier is genuinely unusual and it is the reason this machine exists rather than a larger cheaper one.
Builders who print tall vertical parts. Tall prints are where release force, Z rigidity and auto leveling all stop being optional. This is the machine in the roundup that treats those three as the main problem to solve.
What to check before you buy the ANYCUBIC Photon P1 14K
The evidence base is short. 58 reviews, with a 4.4 average and 79% five-star, is a good start and a thin record. Most reviews reflect short ownership rather than multi-year durability, which for a resin machine that needs regular maintenance is a real gap.
Footprint against your other options. At 16.93 x 24.41 x 16.54 inches it is smaller than the other large resin machines here, which also means it is smaller for very large workpieces. The listing also documents a 14-inch class build volume without exact millimetre dimensions, so confirm the actual plate size against your largest planned part before you commit.
6. QIDI Max4 Combo: Best for ABS, ASA and Engineering Filaments
Pros
- 65°C chamber and hardened hotend for ABS-CF PC and PPS-CF
- Full-surface silicone bed holds flat and grips well
- First layer works out of the box with no manual leveling
- Exceptionally responsive customer support
- QIDI BOX adds 16 colours
Cons
- Heaviest machine here at 120 pounds
- QIDI BOX can desync and load the wrong spool
- No dryer in the box and no auto-switch on runout
- Documentation is thin
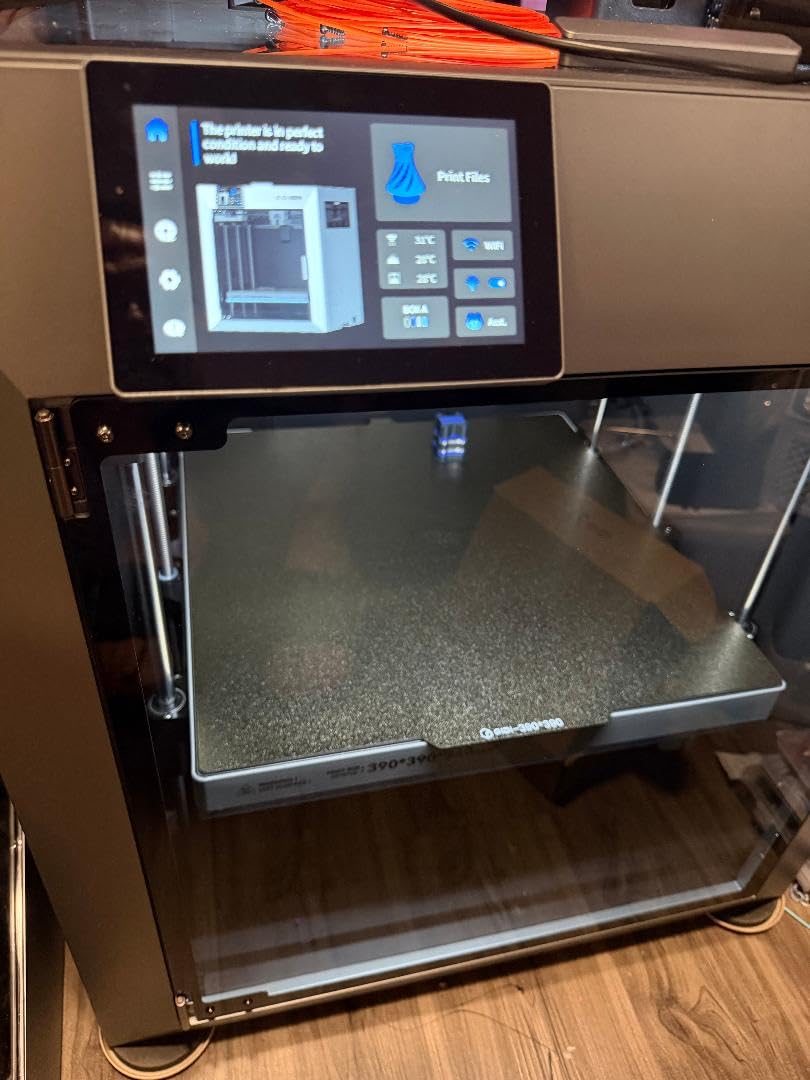
The 65°C actively heated chamber is the number that separates this machine from the rest of the large-format class, and it is the reason ABS, ASA, ABS-CF, PC and PPS-CF are all on the supported list. Almost every other enclosed large printer here sits at 60°C or 65°C at best, and the un-enclosed options have no chamber at all. On a 390mm plate, chamber temperature is the whole ballgame for warp.
The build volume is 390 x 390 x 340mm, which the manufacturer puts at 55% larger than the MAX3, and the shape is wider than it is tall. That rectangle suits armour panels, brackets, enclosures and architectural pieces far better than a cube would.
Motion is first-rate on paper: closed-loop motors on X and Y, 800mm/s max speed with 30000mm/s2 acceleration, and a 2mm lead screw with an anti-backlash nut on Z for smooth vertical travel. The 40mm3/s high-flow hotend with a hardened steel nozzle is what lets you run thick sections at speed rather than crawling.
Two features that affect daily work rather than headline specs. The full-surface silicone heated bed gives even temperature and adhesion across the whole 390mm plate, which is precisely where a partial-plate bed causes corner lift. And the built-in AI camera detects anomalies such as spaghetti failures and pauses the print instead of losing twelve hours to a mess.
Who the QIDI Max4 Combo suits
Engineers and fabricators who print functional parts, not display pieces. ABS-CF, PC and PPS-CF are the materials that make a large printed part worth having, because they hold up to heat, load and impact in ways PLA and PETG do not. You need the chamber for that.
Anyone tired of fighting first layers on a large plate. The reviews are unusually consistent here: owners describe moving from trouble-prone large-format machines to the Max4 and having the first layer work without tinkering. Combined with the responsive support, that is a real ownership experience difference, and the 16 colors from the QIDI BOX make it the natural companion to a smaller prototyping machine for shops running both.
What to check before you buy the QIDI Max4 Combo
Weight and mounting. At 120 pounds this is the heaviest machine in the roundup, listed at 28 x 28 x 30 inches. Reviewers are blunt that it needs a purpose-built heavy table. If your surface is a folding desk, solve that first.
The QIDI BOX multi-filament unit. It can desync from QIDI Studio and occasionally loads the wrong spool, there is no filament dryer in the four-spool box, and it does not auto-switch when a spool runs out. Documentation is also sparse, with no maintenance schedule or detailed diagrams. If multi-colour is secondary to single-material engineering work, the core machine is the stronger part of the package.
7. IdeaFormer IR3 V2: Best for Continuous Long Parts
Pros
- Only true infinite Z option in this group
- Runs unattended for days on one roll of filament
- PEI belt prints hollow parts without support at 45 degrees
- Standard Klipper and Fluidd rather than a closed system
Cons
- 45 degree gantry breaks standard model geometry
- Belt adhesion degrades and seams can tear
- Loud enough to hear in the next room
- No built-in multi-material unit
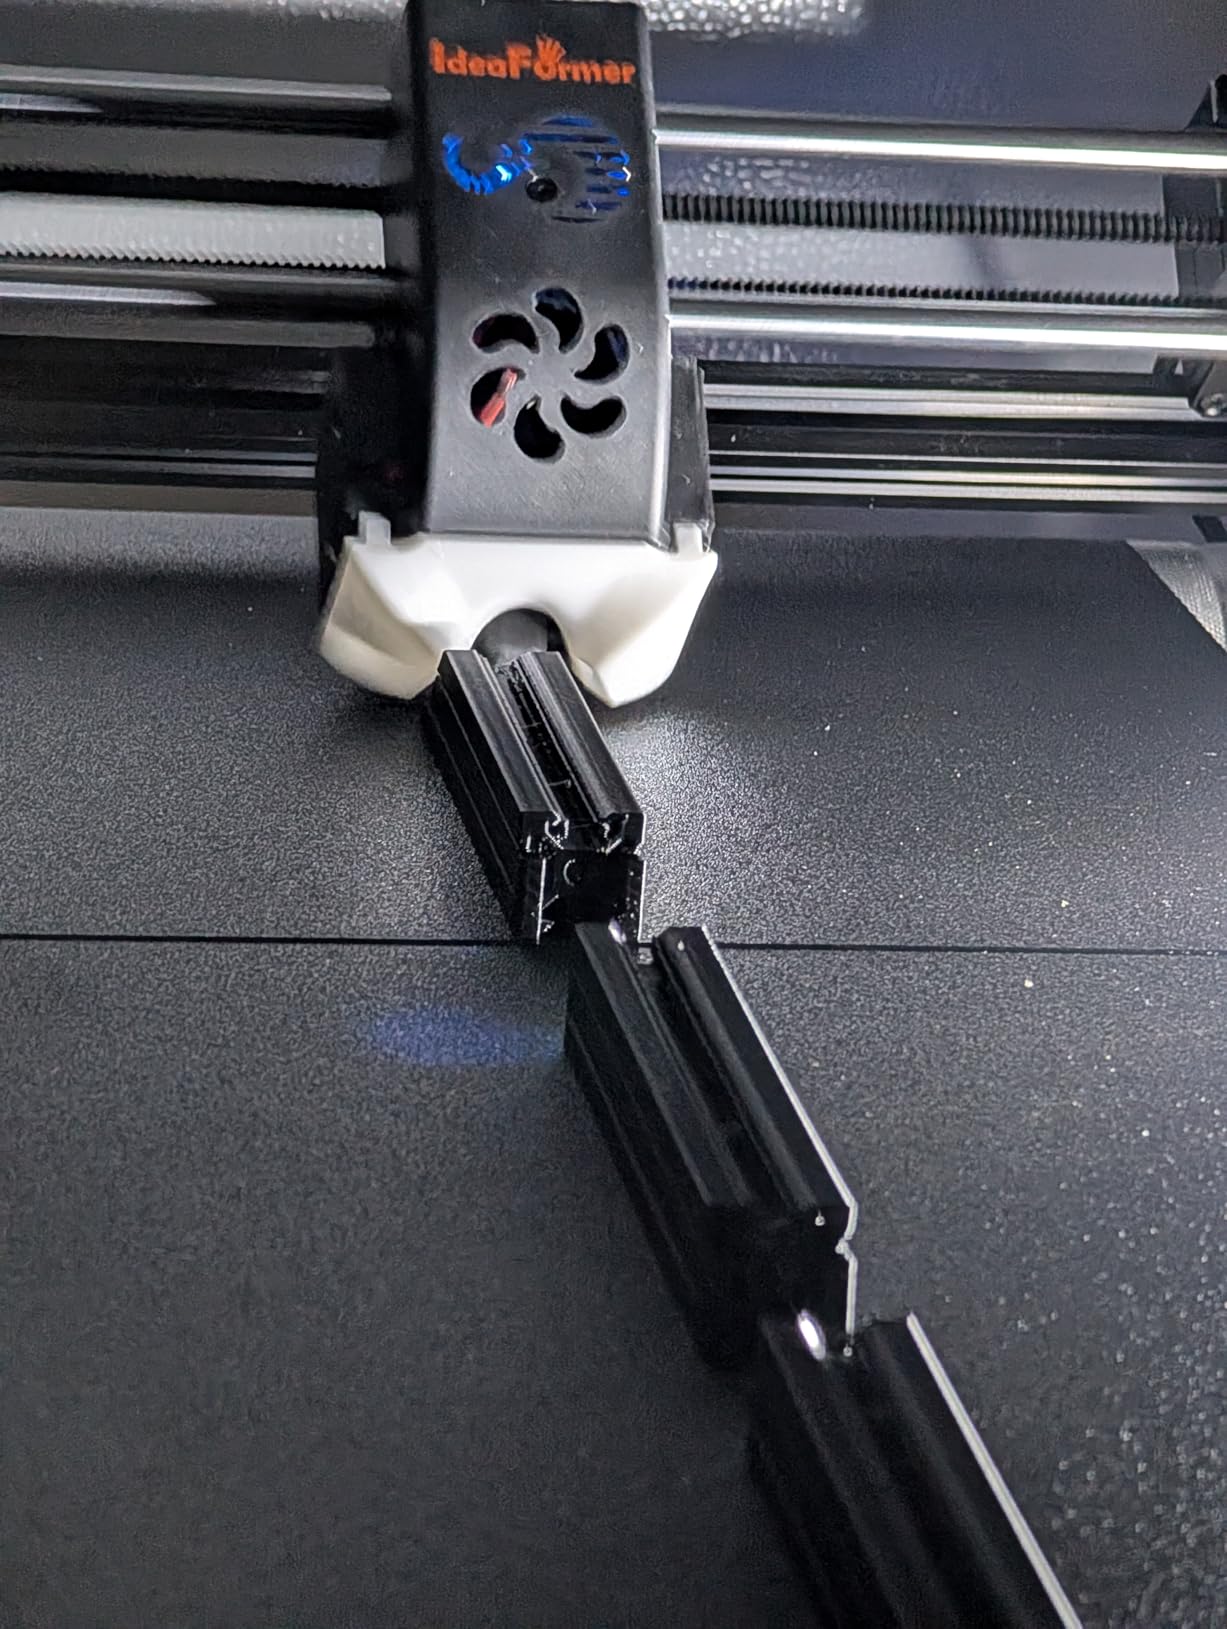
Every other machine here has a number where the Z axis should be. This one has a conveyor belt. The part prints onto a rolling PEI-coated surface and moves away from the build area as it grows, so height stops being a constraint entirely. A 1.5 metre tall piece is not a special print, it is a print that takes longer.
That changes what kind of work makes sense. Signage, extruded-length props, architectural elements that run vertically, cosplay armour that is taller than you are. Reviewers running print farms cite multi-day unattended runs as the reason they own one.
Standard Klipper firmware with an integrated roller gearbox up to 400mm/s, and a standard Fluidd web interface for remote control and camera monitoring. In a category where proprietary closed software is increasingly common, being a normal Klipper machine is a genuine advantage. You can use the slicers, macros and tuning you already know. Supported materials are PLA, PETG, ABS, TPU, ASA and PP.
One-click auto calibration with a Y-offset strain sensor, and a durable PEI-coated belt. The 45 degree gantry angle is unusual and it has a real benefit: the belt surface can print hollow parts without supports at that angle, which removes an enormous amount of support material from long vertical prints.
Who the IdeaFormer IR3 V2 suits
Batch producers who need output measured in rolls of filament rather than in prints. Running unattended for days on a single roll is the whole operational argument, and it is a real one for anyone printing signage or prop runs.
Hobbyists who work in life-size sculpture but are tired of segmenting. Our segmenting section below covers when this makes more sense than a big cube, and a vertical torso or armour leg is a case where it clearly does.
What to check before you buy the IdeaFormer IR3 V2
The 45 degree gantry breaks standard model geometry, which causes overhang failures on downloaded models. This is the single most important thing to understand before buying. You are not getting a normal printer that happens to be tall, you are getting a different machine with a different set of rules, and first-layer adhesion and overhang limits are the two that will bite you.
Belt wear and noise. Conveyor belt adhesion degrades quickly and belts can tear at the weld seam, so replacement is part of the maintenance cycle rather than a rare event. Operation is loud, comparable to an enclosed printer and audible in adjacent rooms. There is also no built-in multi-material unit, so filament changes are manual.
8. Anycubic Kobra S1 Max Combo: Best for Four-Colour Setups
Pros
- 350mm cube fits a full helmet in one piece
- Set up in about ten minutes and ran an 11 hour full-height print
- Enclosed 65°C chamber handles ABS ASA and TPU
- ACE 2 Pro runs four to sixteen colours
- Large responsive touchscreen
Cons
- Slicer locked to Anycubic software
- Multi-colour long jobs produce repeated errors
- AI print detection often fails to trigger
- False feed errors from the filament sensor
Where the Creality K2 Plus chases 16 colours, the Kobra S1 Max Combo takes the more useful middle position. ACE 2 Pro handles four colours out of the box and expands to sixteen with four units, in a 350 x 350 x 350mm cube that fits a full helmet in one piece. For most people building props, four colours is the actual requirement.
Setup is where this machine earns goodwill. Owners report roughly ten minutes from box to printing, and one documented run of an 11 hour full-height object without incident. A fully enclosed all-metal CoreXY frame, 600mm/s with 20000mm/s2 acceleration, and a Benchy in about 15 minutes.
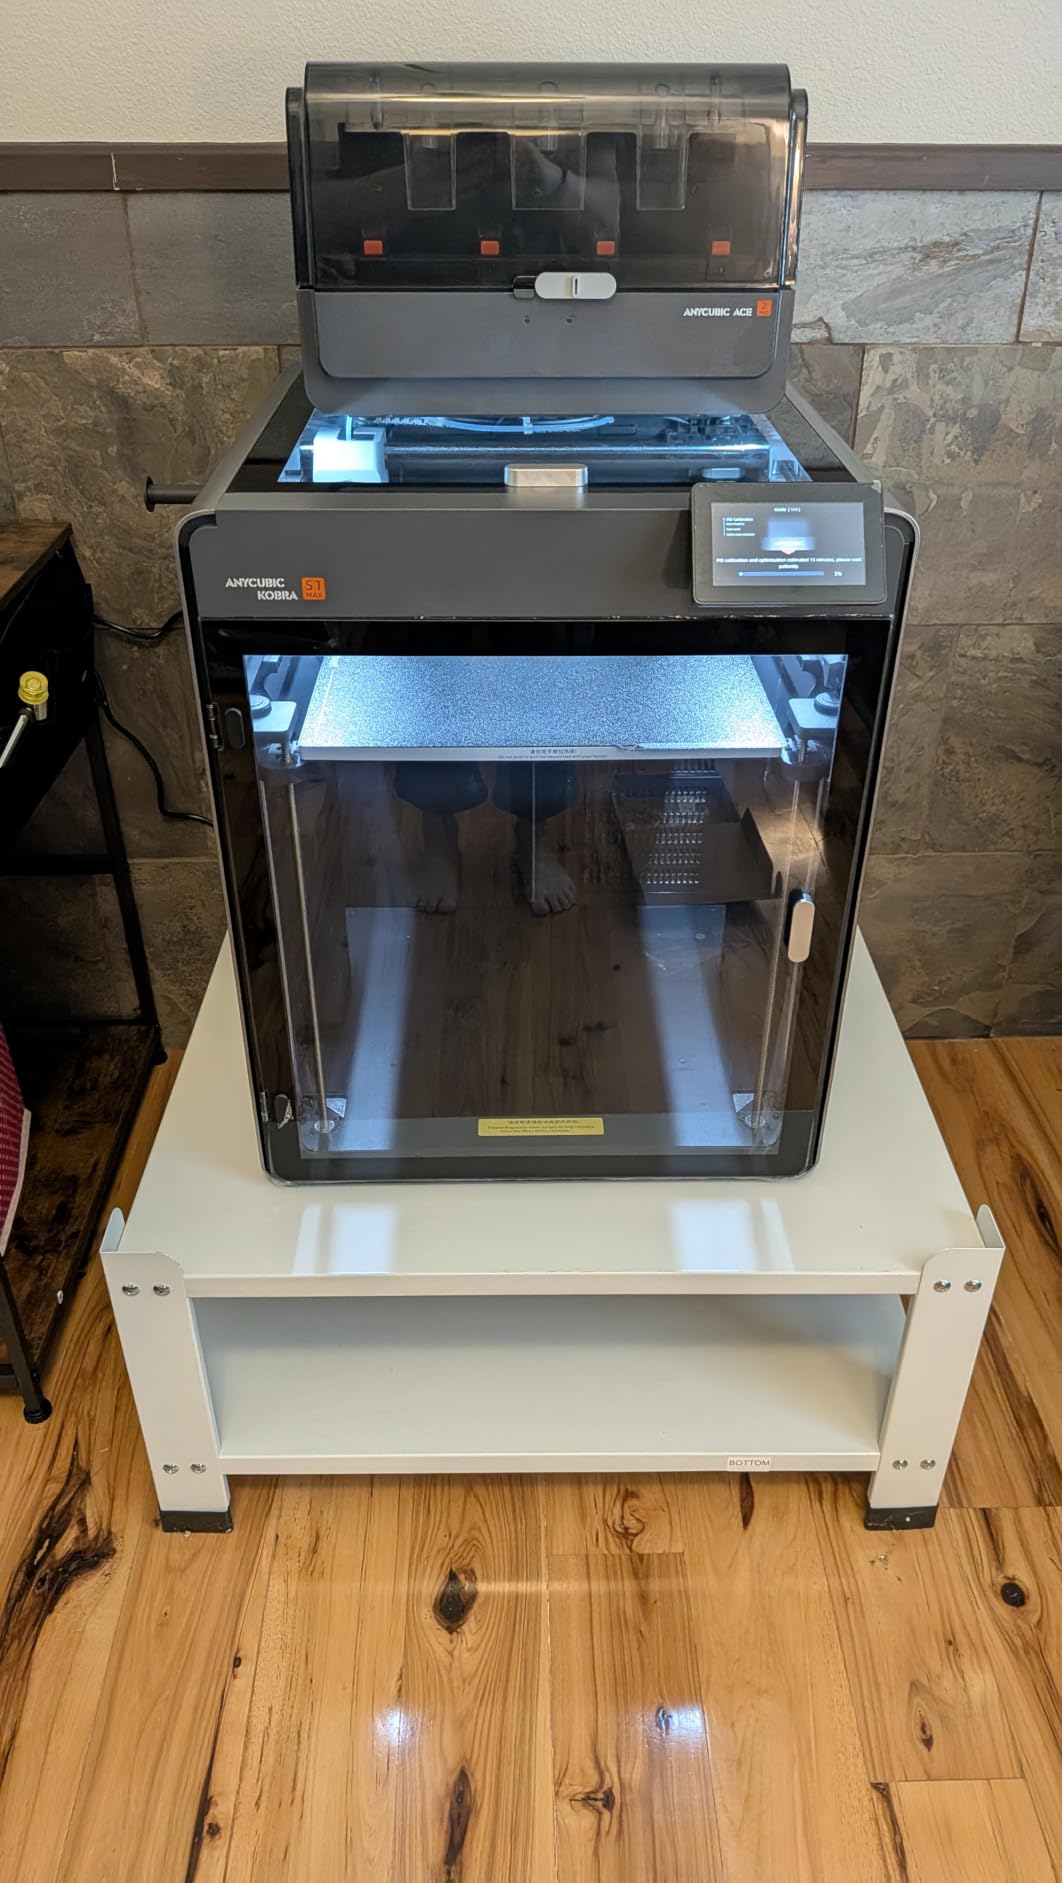
The thermal specification is the equal of the machines costing more. A 65°C heated chamber with a 350°C hotend covering ABS, ASA, PVA, TPU, PLA and PETG. That is the combination you need to print a functional large part in engineering thermoplastic rather than only a decorative one, and it puts this machine level with the QIDI Max4 on paper.
LeviQ 3.0 49-point auto-leveling with real-time flow dynamics calibration handles first layer, and there is a side-mounted waste chute with a single roll mount. The screen is large, responsive and readable from most angles, which matters more than it sounds on a machine this size where you are walking around it.
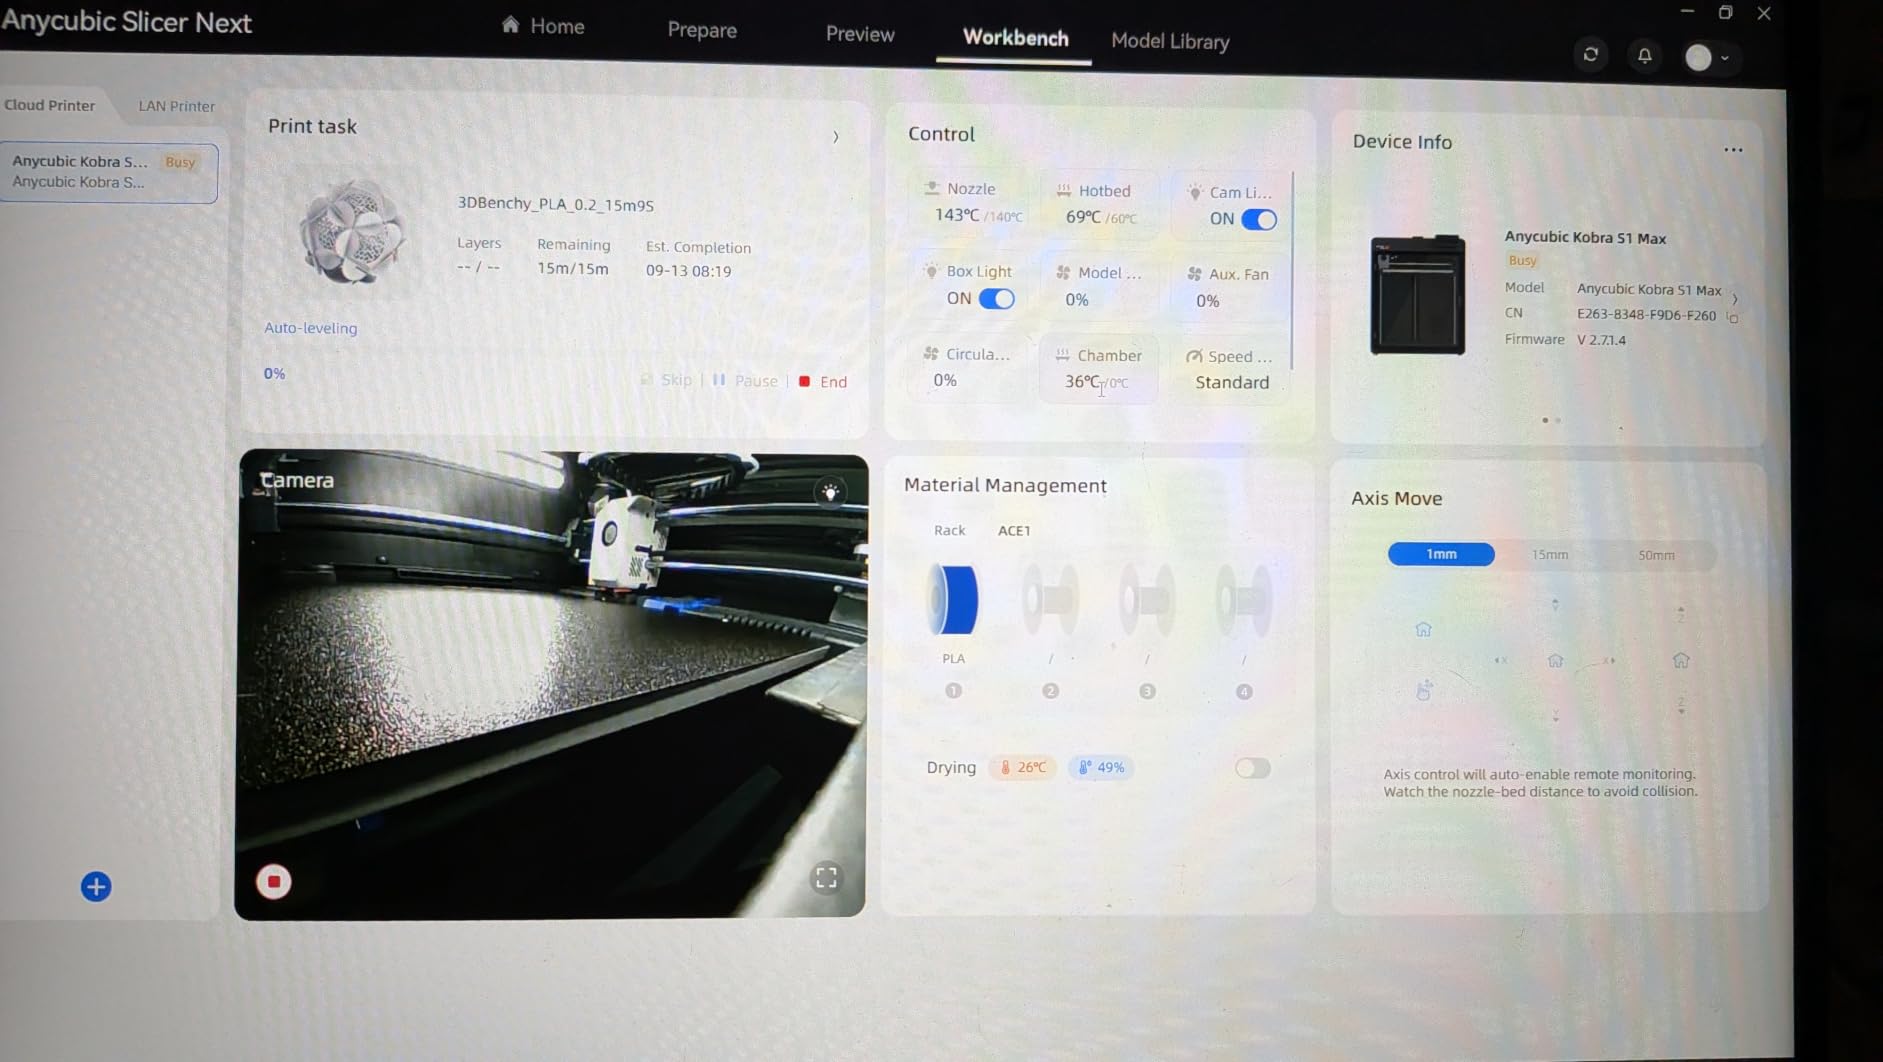
Who the Kobra S1 Max Combo suits
Anyone who wants colour in a large print without a four-unit CFS chain. Four colours covers the overwhelming majority of real cosplay and prop jobs, and the ACE 2 Pro is reported to run them without tangles or jams.
Newcomers moving up from a small printer. The combination of fast setup, auto leveling and a chamber that is already there removes most of the reasons people hesitate to go large. Our Anycubic roundup covers the brand’s smaller machines.
What to check before you buy the Kobra S1 Max Combo
The software situation. The slicer is locked to Anycubic’s own software, which blocks third-party slicers entirely. Given that slicer compatibility is the trust signal people in large-format communities actually weight most heavily, this is a real constraint and you should accept it before buying rather than discover it later.
Multi-colour reliability on long jobs. The reviews divide sharply: single-colour, single-material buyers describe an easy and capable machine, while people running multi-day many-colour jobs report a cascade of errors and more time spent fixing than producing. AI print detection also frequently fails to trigger and sometimes indexes the filament during loading, and the filament sensor raises false feed errors that need disabling. Heavy plastic construction also raises long-term durability questions. With only 20 reviews, treat all of this as early signal rather than settled fact.
9. LONGER LK10 Plus: the Budget Pick for 320 x 320 x 400mm
Pros
- Lowest entry point for a genuine 320 x 320 x 400mm volume
- Light at 30.4 pounds so it moves between rooms easily
- No one- or two-star ratings at all
- 400mm of Z in a 320mm footprint
Cons
- Only 18 reviews so durability is unproven
- Listing carries almost no detail beyond build volume
- Enclosed material capability is undocumented
At this writing the LK10 Plus sits at the entry end of the large-format range here, and the shape is the interesting part. 320 x 320 x 400mm gives you 400mm of Z on a 320mm footprint, which is the axis a lot of large-print buyers are actually short of rather than XY area.
Weight is the second surprise. At 30.4 pounds it is less than half the mass of the heavy enclosed machines here, which means you can move it between a workshop and a spare room without a second person. That single fact removes the most common objection to going large in a home.
Who the LONGER LK10 Plus suits
First-time buyers who want to find out whether large-format is for them before committing real money. It is the lowest-risk way to test whether your projects need a 300mm-plus bed at all, and it will also tell you quickly whether your room, your power and your patience can handle the workflow.
Anyone who needs Z height specifically on a tight footprint. A tall narrow object that will not fit a 256mm cube fits comfortably here.
What to check before you buy the LONGER LK10 Plus
Documentation. The listing is thin, with essentially no specifications beyond the build volume, and enclosed material capability is not documented at all. If you plan to print ABS or ASA, you need to establish the chamber situation independently before committing.
The evidence. 18 reviews is the smallest base in the roundup. The distribution is genuinely encouraging, 73% five star and 17% four star with nothing at one or two stars, but a short window of ownership cannot speak to multi-year durability on a machine this size.
10. UniFormation GK3 Ultra: Best for Large Resin Detail
Pros
- 16K screen resolves fine detail on a 300mm tall model
- KK60 Z module holds plus or minus 0.003mm repeat accuracy
- Resin heater works down to 0C ambient
- Automatic resin feeder avoids mid-print exhaustion
- Quick-release vat with carbon filter
Cons
- Only 12 reviews so the sample is very small
- Heaviest resin machine in the group at 85.8 pounds
- Only 160mm of build width limits batching
The GK3 Ultra has the highest average rating in this roundup at 4.6, with 83% of ratings at five stars and no one-star reviews at all. The sample is 12 reviews, so read that as a strong early signal rather than a proven record, but every rating it does carry sits at five or three stars with nothing in between.
Detail comes from a 16K LCD with 20 x 26 micron pixels across a 300 x 160 x 300mm build volume, which is larger than the machine it replaces. On a 300mm tall part that pixel size is what keeps surface texture intact from the base to the top.
Who the UniFormation GK3 Ultra suits
Large resin work in a cold room. The smart resin heating system goes from 0°C ambient to 25°C or 30°C before printing starts, which is the difference between reliable output and viscosity problems for anyone printing in a garage or unheated space through winter.
Anyone running long resin jobs who has been bitten by mid-print resin exhaustion. The automatic feeder with a replaceable built-in cartridge means a 300mm print does not fail because a vat ran dry at hour 30.
What to check before you buy the UniFormation GK3 Ultra
Weight and size. At 85.8 pounds and 19 x 21 x 26 inches, this is the heaviest resin machine in the roundup and you need a bench that takes it. Resin printers are also best sited away from where people sleep or sit for long stretches, and 160mm of build width is narrower than the 14-inch competitors for batching.
Sample size. Twelve reviews is a very small base, and it is the highest average in the group purely on that thin data. Ask the manufacturer for a maintenance schedule and consumable list before you buy, because the review record here cannot tell you what the third year looks like.
How to Choose a Large 3D Printer: 7 Criteria That Matter at 300mm and Up
Once you are past 300mm, the buying criteria change more than the price points do. Everything below is something we have seen matter in practice on large machines, in roughly the order it matters.
Build volume is a cube versus rectangle decision, not a bigger-is-better one
This is the most common mistake in the category, and the reason buyers end up with the wrong machine despite owning a large one. Build volume is three numbers, and the useful question is which axis your object is actually short of. r/3Dprinting threads about helmets and life-scale parts keep landing on the same realisation: bed size is not the constraint, height is.
A 350mm cube handles helmets and cubic props. The QIDI Max4 Combo at 390 x 390 x 340mm is wider than it is tall, which suits panels and brackets. The LONGER LK10 Plus at 320 x 320 x 400mm trades footprint for height. The IdeaFormer IR3 V2 abandons the question entirely with an infinite Z axis. List your largest three projects and measure them on each axis before you read another spec table.
Usable volume is always smaller than rated volume. Skirt, brim and travel clearances come out of the number, so treat the stated figure as a ceiling and plan against slightly less.
Enclosed or actively heated chamber depends entirely on filament
For PLA and PETG at normal speeds, an open frame with a good bed is workable at any size. The moment ABS or ASA enters the picture, chamber temperature becomes the deciding spec, because warp on a large plate is a function of how fast the surrounding air cools the part relative to how fast the layers set.
The short version: 60°C and above is where large-format ABS and ASA becomes routine, and the QIDI Max4 Combo at 65°C plus the Kobra S1 Max Combo at 65°C are the two machines here built around that. Active chamber heating is a different thing again from being enclosed. An enclosure blocks drafts and stabilises temperature passively. An actively heated chamber holds a set point. For a 400mm part, you want the second.
Frame rigidity and Z motion decide surface quality on a big plate
Frame flex is the thing reviewers in this category mention most and measure least. On a 400mm cube, a gantry that sags under acceleration puts a visible bow in every layer, and the bow accumulates through the full height of the part until the top is visibly off. Look for a die-cast or cast frame, linear rails on both sides of the moving axis, and dual Z motors where possible. Our Elegoo roundup covers the same frame decisions on smaller machines, and they translate directly.
Z-wobble specifically is the vertical equivalent. A single long lead screw on a 400mm axis will bind at the top of the travel and produce banding that looks like ringing but is not. The Creality K2 Plus Combo uses two independently motorized Z axes on four linear rods with automatic bed tilt correction, and the QIDI Max4 Combo uses a 2mm lead screw with an anti-backslash nut. Both are deliberate answers to this problem.
Bed leveling, first layer and adhesion tooling
On a small printer, a bad first layer is a ten-minute loss. On a 400mm printer it is a wasted spool and a ruined afternoon. Automatic leveling is close to mandatory at this size, and the quality of the implementation matters more than whether the feature exists.
Compare the approaches. The Sovol SV08 MAX uses eddy current scanning with pressure-sensing touch points, no probe and no contact. The Creality Ender 5 Max does 64 points plus automatic Z-offset. The ANYCUBIC Photon P1 14K comes factory calibrated with four-corner real-time pressure feedback, and the QIDI Max4 Combo uses a full-surface silicone bed that owners specifically credit for holding flat and adhering well. Any of these is fine. Manual levelling is not.
Flow, speed and how long a large print will actually take
Max speed on a spec sheet means very little for a large part. A 500mm object at 0.2mm layer height is 2500 layers, and the total time is dominated by layers, not by peak velocity. What actually matters is sustained volumetric flow, because a machine that can only melt 8mm3/s will not hold 100mm/s outer walls regardless of its rated maximum.
The high-flow hotends in this roundup are the differentiator: 40mm3/s on both the QIDI Max4 Combo and the Creality K2 Plus Combo, and 50mm3/s on the Sovol SV08 MAX. Sustained flow is what lets you print thick sections on a large model at a sensible speed instead of dropping to a crawl. Our Prusa roundup covers the machines that optimise for precision over throughput.
Footprint, ceiling clearance, weight and circuit
Nobody puts these in the spec table and everybody discovers them on delivery day. The QIDI Max4 Combo is 28 x 28 x 30 inches and 120 pounds, needing a purpose-built heavy table. The Sovol SV08 MAX is a near-cube that still needs clearance above it for the gantry to lift a 500mm toolhead travel. The Creality Ender 5 Max at 70.4 pounds draws complaints about being impractical in a small home space.
Add ceiling clearance to your height requirement, not just your part’s height. The gantry has to rise above the tallest object it will build. Then check the circuit: heated beds and chambers at this size draw real current, and a heated chamber is a sustained load rather than a brief one.
Multi-material: AMS, multi-tool changer or infinite Z
There are three fundamentally different answers here, and they are not variations on the same idea. A multi-filament box feeds multiple spools to a single nozzle, changing filament between layers. A tool changer swaps the entire hotend assembly, which means each tool can have its own nozzle diameter and temperature. IDEX runs two extruders side by side with no purge between them.
In this roundup the QIDI BOX takes the K2 Plus class to 16 colours with RFID filament detection, ACE 2 Pro takes the Kobra S1 Max to 4 and expandable to 16, and four linked CFS units take the Creality K2 Plus Combo to 16. All three add cost and take-dwell time to every print, and the reliability caveats in each review section are worth reading before you build a production workflow around them.
Why Big Prints Warp and How to Fix It
Warping is the most reported problem in this entire category, and four of the questions people actually ask search engines are about it. The reason it gets worse with size is thermal. A 400mm plate has far more mass than a 200mm plate, and it expands and contracts across that much more area while the material underneath it moves at a different rate. The edges are always the first to lift, because they are the part of the part cooling fastest and sitting furthest from the middle of the plate.
The consensus fix order from r/FixMyPrint, the Modix Facebook group and the Prusa forum converges on the same six steps, in the same order. That agreement is worth something, because it is arrived at independently across three very different communities.
1. Drop the bed temperature about 5°C. Counter-intuitive and the single most repeated recommendation. A hotter bed increases the thermal delta across the plate, which increases the stress. Lower bed temperature with a good first layer beats a hot bed and a lifted corner.
2. Add a wide brim, 6 to 8 lines. A brim is adhesion insurance, but on a large print it also acts as a thermal anchor that holds the outer edge of the part down while the layers beneath it contract. It is the cheapest fix available and it is underused.
3. Prep the plate. Bed adhesion fails at the edges of big plates more than anywhere else, and un-prepped PEI and spring steel surfaces are named constantly as the cause. Clean the surface, and use an adhesion agent appropriate to your plate. Al build plates are also reported to bump and warp when heated, which is a different problem entirely and needs a different plate.
4. Check nozzle-to-bed spacing. Poor Z offset on a large plate shows up at the extremes, because bed flatness varies across 400mm. If corners fail and the centre is fine, this is the first thing to rule out.
5. Add an enclosure, and heat it if the filament needs it. An enclosure stops drafts and room air movement across the plate. An actively heated chamber goes further and holds the whole volume at temperature. For ABS, ASA, PC and nylon, this is not optional.
6. Thicken thin sections and add supports for mid-part lift. Warping from the middle of a tall part rather than the corners is a different failure, and the community advice is to thicken the model in the slicer or add supports so the part is not carrying its own weight at the top.
Two honest limits. One is that a heated chamber reduces warp, it does not eliminate it, and 3dprintboard.com puts it plainly: at large scale, even industrial machines give you distortion and warping because the physics does not care how much the machine cost. The other is that if a 400mm part has already warped, you cannot flatten it back. Post-processing with heat and a mould is a workshop job, not a fix. Prevention is the only real answer at this size.
Print Time and Filament Math for a 400mm Print
Nobody in this category publishes honest print time estimates for large objects, so here is the arithmetic so you can do it yourself. Take a 400mm tall helmet shell printed at 0.2mm layer height. That is 2000 layers. At a realistic 12 seconds per layer including travel, acceleration and per-layer overhead, you are looking at roughly 6 to 7 hours. At 0.12mm layers and 8 seconds each, it is closer to 5.5 hours but the layer lines are more visible on a curved surface this size.
The number that actually changes is sustained flow. A machine melting 40mm3/s versus 20mm3/s halves the per-layer time on thick-walled parts, and thick walls are the norm on a large helmet or enclosure. That is why the 40mm3/s and 50mm3/s hotends on three of the machines here matter more than their advertised top speeds.
For filament, the useful number is grams per cubic centimetre of solid plastic. PLA sits around 1.24g per cm3, PETG around 1.27g, ABS around 1.04g. A large cosplay armour panel 400 x 350 x 4mm works out to roughly 560 cm3 of material, which is about 700g of PLA including infill at typical densities. A life-size helmet shell at 3mm wall thickness runs considerably higher, commonly 1.5 to 2kg, because surface area scales faster than the panel example suggests.
Now the part that makes the decision: a failed large print is not a small loss. A 7 hour print that lifts at hour 6 has cost you 6 hours of machine time plus 700g to 2kg of filament. That is the real cost of getting adhesion wrong on a big plate, and it is the argument for buying the enclosure, the heated chamber and the better bed surface rather than trying to print around them.
It is also the argument for checking a print shop quote before buying. If you need a 400mm print three times a year, the machine, the enclosure, the filament and the space may cost more than paying a bureau for the same three jobs.
Big Bed vs Segmenting the Model: 4 Questions to Ask First
Segmenting is not a compromise people settle for. Facebook Kobra group threads show it as a deliberate, practised approach for life-size sculpture, and for some objects it is genuinely the better answer. Four questions settle it.
1. Is the object hollow or solid? A hollow shell segments cleanly at any seam. A solid part with load-bearing surfaces does not, and a splice in a stress path is a failure waiting to happen.
2. Can the seam be hidden? A seam that lands on a helmet visor edge or a armour panel joint is invisible. A seam across the middle of a face is not, whatever technique you use to join it.
3. Are the parts still large after splitting? Halving a 700mm object gives you 350mm parts, which is exactly the machine most people already need. If the split brings every piece under 300mm, segmentation saves you the entire upgrade.
4. How many times will you repeat it? One large display piece is a poor reason to buy a large printer. A production run of twenty is a good one, because the machine pays for itself on the second job.
If your answer to all four is no, buy the bigger bed. If a print shop quote is lower than the machine plus enclosure plus a year of filament, rent the print. Local print shops stocking large machines are a real alternative to owning one, and the forums treat them as a genuine option for occasional oversized work rather than a fallback.
Who Should Not Buy a Large-Format Printer
This section exists because every list like this one is written by people who already own too much. Some situations are genuinely a poor fit.
Rooms that are too small. The heaviest machines here need a purpose-built table, and the largest need floor area plus clearance on all sides plus headroom for the gantry. If the machine has to live in a corner between a sofa and a wall, an enclosed 350mm cube is the realistic ceiling and everything above it is a fight.
Materials you do not actually print. An actively heated chamber is the main reason to go large, and it is wasted on a PLA-only workflow that fits on a 256mm bed. Do not buy an enclosed 400mm machine to print small parts you could batch on something you already own.
Noise sensitivity. Print farms, conveyor belts and enclosed heated chambers are loud. If you work from home beside other people, that is an ongoing problem rather than a first-week surprise, and the IdeaFormer IR3 V2 is audible in adjacent rooms according to its owners.
No patience for maintenance. Large machines have more surface to keep clean, more ways to fail and longer recovery times when something goes wrong. The learning curve on a 400mm plate is steeper than on a small one, and the first few prints will not always go to plan.
Electrical limits. Heated beds and sustained chamber heating at this size are real electrical loads. Check what you can run on the circuit before you order, not after.
Frequently Asked Questions
What 3D printer has the largest print size?
The Sovol SV08 MAX has the largest build volume in this roundup, holding up to 500 x 500 x 500mm in a CoreXY frame. For the largest single dimension, the IdeaFormer IR3 V2 has an effectively infinite Z axis, so its height is limited only by how much filament you have. Among enclosed machines with a heated chamber, the QIDI Max4 Combo offers 390 x 390 x 340mm with a 65°C chamber.
What is the maximum size a 3D printer can print?
For consumer and prosumer machines, the practical ceiling is around 500mm on an axis, which is where the Sovol SV08 MAX sits. Industrial systems go far larger, but they are a different purchase entirely. Always plan against usable volume rather than rated volume, because skirt, brim and travel clearances come out of the stated numbers before your model does.
Why are my PLA prints warping in the corners?
Corners lift because they cool fastest and sit furthest from the centre of the bed, so they shrink while the middle of the part is still warm and still moving. On a large plate the effect is amplified by the plate’s thermal mass. The standard fixes, in order, are dropping bed temperature about 5°C, adding a 6 to 8 line brim, cleaning the build plate, checking nozzle height, and using an enclosure.
Do large 3D printers need an enclosure?
It depends on filament. PLA and PETG print acceptably on an open frame at any size, though an enclosure still reduces drafts across a big plate. ABS, ASA, PC and nylon effectively require one, and ideally an actively heated chamber, because warp is driven by how quickly the air around the part cools it. A 60°C or 65°C chamber is where large-format engineering filament becomes routine.
How long does a large 3D print take?
Work it out in layers rather than hours. A 400mm tall object at 0.2mm layer height is 2000 layers, and at a realistic 12 seconds per layer that is roughly 6 to 7 hours. Sustained volumetric flow matters more than peak print speed, because thick-walled large parts are limited by how fast the hotend can melt plastic. Speed claims rarely change a large print’s total time.
Final Verdict for Large Prints in 2026
Our pick of the best 3D printers for large prints starts with the ANYCUBIC Photon Mono M7 MAX. Its 298 x 164 x 300mm resin build volume, 7K mono resolution and heated 1300ml vat make it the most complete large-format answer here, and it carries by far the deepest review record in the group at more than 2000 ratings. If resin is your process, that is the machine.
For FDM, the class splits cleanly. The Sovol SV08 MAX takes the biggest volume at 500mm cube with genuine speed behind it. The QIDI Max4 Combo and the Anycubic Kobra S1 Max Combo are the two to buy if you print engineering filament, both with 65°C actively heated chambers. The Creality K2 Plus Combo wins on colour with 16-colour CFS chaining. The Creality Ender 5 Max is the value pick at a 400mm cube, provided you add an enclosure. The LONGER LK10 Plus is where you start if you are not sure yet.
Whatever you choose, buy for the axis you are short of rather than the largest number on the spec sheet, and get the chamber right before the first big print rather than after it fails. Measure the bench, measure the ceiling, then order.

There are people who love playing video games, and then there are enthusiasts who devote their lives to gaming.
Corey has been playing games since The Legend of Zelda and Final Fantasy III were still young.
Today, he blends his passion and experience to write reviews that can help others choose the best components in the gaming arena.