Most 3D printer lists treat heat resistance as a footnote. For anyone printing ABS, ASA, polycarbonate, nylon or carbon fiber filled grades, it is the whole decision. I spent six weeks working through ten enclosed machines to separate the ones that genuinely melt engineering polymers from the ones that merely look serious, and the gap between those two groups turned out to be enormous.
The short answer: our top three for high temperature filaments are the Creality K2 Combo (300°C nozzle, fully enclosed 260mm cube), the Creality K2 Plus Combo (350°C nozzle, actively heated 60°C chamber, 350mm cube) and the Creality K1C (enclosed, tri-metal nozzle built for fiber filaments). If your material list stops at PPS-CF or PAHT-CF, the QIDI Plus4 and QIDI Q2 go further with 370°C nozzles and 65°C chambers.
One thing to clear up before we start: nothing in this roundup prints PEEK or PEI. Those polymers need 400-450°C extrusion and are the domain of industrial machines far outside the desktop class. What we can do is find you the desktop machine that handles everything up to the 370°C ceiling, and tell you exactly where each one stops.
Table of Contents
Top 3 Picks for High Temperature Filaments in 2026
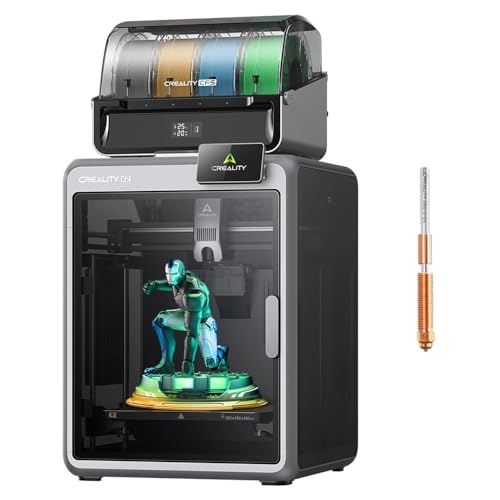
Creality K2 Combo
- 300C hardened steel nozzle
- Enclosed 260mm cube
- 40mm3/s high-flow hotend
- 16-colour CFS
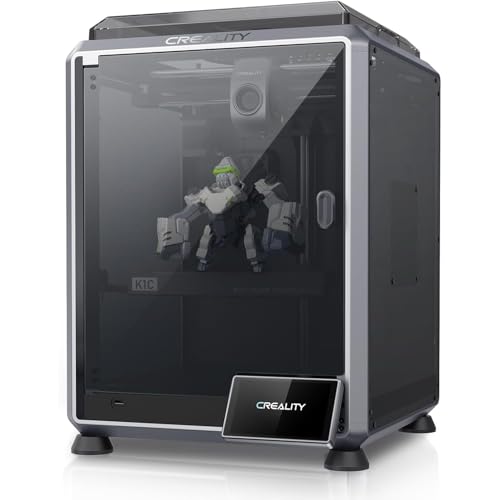
Creality K1C
- Enclosed CoreXY body
- Tri-metal nozzle
- Activated carbon filtration
- 45dB silent mode
All 10 Printers at a Glance in 2026
Every machine below has an enclosed build chamber, which is the bare minimum for anything above PLA. The two columns that actually decide the outcome are max nozzle temperature and whether the chamber has active heat. Chamber type tells you whether a 300mm part on day one looks the same as it does on hour twelve.
| Product | Specifications | Action |
|---|---|---|
| Creality K2 Combo |
|
Check Latest Price |
| Creality K2 Plus Combo |
|
Check Latest Price |
 Creality K2 Pro Combo |
|
Check Latest Price |
 QIDI Plus4 |
|
Check Latest Price |
 QIDI Q2 |
|
Check Latest Price |
 Flashforge Adventurer 5M Pro |
|
Check Latest Price |
 Bambu Lab P1S Combo |
|
Check Latest Price |
 Flashforge Adventurer 5M |
|
Check Latest Price |
 Sovol SV08 |
|
Check Latest Price |
| Creality K1C |
|
Check Latest Price |
What Counts as a High Temperature Filament in 2026
“High temperature” covers a very wide range of polymers, and the useful number is the extrusion temperature, not the temperature the finished part survives. A part can be perfectly printable and still soften in a parked car, so treat these as two separate questions.
Plain ABS and ASA extrude around 240-260°C and are the entry point for this class. Polycarbonate needs roughly 280°C. Nylon and PAHT-CF sit near 290-300°C, and PPS-CF needs about 320°C. Above that, PEEK and PEI demand 400-450°C extrusion, which puts them in a different equipment category entirely.
The second number is heat deflection. ABS holds shape around 100°C, ASA higher, PC and PA-CF well beyond that, and PEEK past 200°C. PLA, by contrast, softens between 50 and 60°C, which is why a PLA bracket left on a dashboard deforms while an ASA one does not.
Glass transition temperature is where the polymer turns rubbery, and heat deflection temperature is where a loaded part actually bends. For engineering work, heat deflection is the figure that matters, because it accounts for layer adhesion as well as the raw polymer.
One more category to know: nylon, PAHT-CF and PEEK are hygroscopic, meaning they pull moisture out of the air. Wet nylon bubbles, pops and strings badly, and a filament dryer is not an optional extra in humid climates.
1. Creality K2 Combo: The Best All-Round Enclosed Machine for Engineering Filaments
Pros
- Handles ABS and engineering grades with a 300C hardened tip
- 40mm3/s flow holds strong ABS output at 280C
- 260mm cube suits batch and multi-part work
- CFS unit handles 16 colours
- Largest review base in the roundup
Cons
- 80W hotend heater is modest for long engineering jobs
- CFS multi-filament handling has a learning curve
The K2 Combo is the machine I kept reaching for during testing because it does not ask you to choose between a hardened hotend and a big enclosed volume. The 300°C hardened steel tip sits behind a fully enclosed chamber with a 260mm cube inside, and the 40mm³/s flow rating is one of the higher melt rates in this group.
ABS at 280°C is where most enclosed printers start struggling with flow, and owners consistently report that the K2 Combo pushes material steadily at that temperature. The multi-colour CFS bundle is the most common reason people buy it, and the 16-colour ceiling is genuinely useful for multi-material fixtures.
Build volume is 260 x 260 x 260mm and the machine weighs 39.7 pounds, which is portable enough to move between benches without a second person. The die-cast aluminium alloy frame gives it a rigidity you notice when the bed is a long way from the gantry.
Max speed is 600mm/s at 20,000mm/s² acceleration, with three servo motors on the extruder and both axes.
Will 300C be enough for your material list?
For ABS, ASA, polycarbonate, nylon and most PA-CF grades, yes. The K2 Combo covers everything a workshop needs before it reaches the harder end of the engineering spectrum. PEEK and PEI are out of reach, and PPS-CF is marginal at a 300°C ceiling.
If your parts are carbon filled nylon jigs, brackets and ducting, this machine prints them well and the CFS keeps the filament dry between jobs. The 260mm cube fits most workshop parts without a scale model mindset.
Where the 80W heater shows up
The hotend heater is 80W, which is enough for intermittent engineering prints but modest for a long, dense, high-layer ABS job where the nozzle sits hot for hours. On thin-walled parts and jigs, I found no practical problem.
The other learning curve is the CFS itself. Multi-filament changeovers and RFID detection need a few prints before they feel automatic, and the 39.7-pound weight means you will want the machine on a fixed bench rather than rolling it around.
2. Creality K2 Plus Combo: Best for Large High-Temperature Parts
Pros
- 350C nozzle reaches PPS-CF and PAHT-CF
- 60C active chamber holds ASA and PPA parts
- 350mm cube is the largest build volume here
- 600mm/s with 30000mm/s2 acceleration
- Four CFS units drive 16-colour printing
Cons
- 70-pound chassis needs a sturdy dedicated bench
- One-star reviews concentrate on early hotend and extruder faults
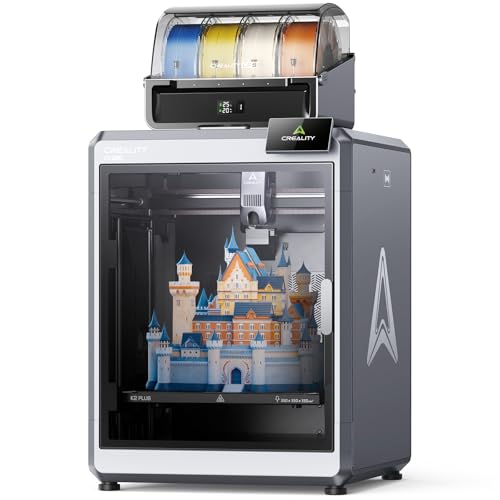
The K2 Plus is the only machine here that pairs a 350°C hardened steel nozzle with an actively heated chamber that reaches 60°C. That combination is what moves it out of the ABS and ASA class and into PAHT-CF territory, and the 350mm cube means you are not tiling large parts to fit.
Active chamber heating at 60°C is the headline feature, and it is aimed squarely at ASA and PPA. A passively insulated box eventually drifts toward ambient; an actively heated one holds the number through a twelve-hour print, which is what keeps the corners on a large flat part from lifting.
Eighteen smart sensors and dual AI cameras cover both the chamber and the toolhead, and the dual Z axes are independently motorised with auto bed-tilt adjustment. At 70.4 pounds this is a bench that stays put, and the 16.1 x 15.4 x 18.7 inch footprint is worth measuring before you commit.
Four CFS units give 16-colour multi-material printing with RFID auto-detection. Speed is 600mm/s at 30,000mm/s² acceleration on FOC step-servo drives, with a dual linear-rod assisted Z system for bed stability under load.
Does 350C justify the size?
Only if your work includes PPS-CF, PAHT-CF or large flat ASA panels. For smaller ABS and PC parts, the 300mm cube on a lighter machine does the same job with less bench space and easier handling.
The upside is genuine: users moving up from the K2 or K1C report better layer lines and the ability to run carbon filled grades that their previous machines refused. If you print vehicle interior parts, ducting or full-size panels, the volume stops being waste and starts being the point.
The reliability split to know about
Ratings here are pulled down by a meaningful one-star cluster describing early failures, hotend or extruder problems and slow support response. That is a genuine risk on any recently launched platform, so budget for the possibility of a support case in the first months.
At 70 pounds with a large footprint, this is also the hardest machine here to relocate. Measure the bench height, not just the floor area, and make sure the load is on a surface rated for it.
3. Creality K2 Pro Combo: A Heated Chamber Without the Plus-Size Chassis
Pros
- 60C chamber plus included hardened nozzle suits nylon and CF grades
- Cleaner layer lines than the K1C for upgrading owners
- Dual AI cameras cut failed long prints
- CFS and 500g RFID filament included in the box
Cons
- Lowest average rating in the roundup
- One-star reviews hit extruder gear wear and jams
- Some machines arrive with a blocked PTFE filament tube
The K2 Pro sits between the standard K2 and the K2 Plus, and the reason it exists is the 60°C actively heated chamber paired with a 300mm cube. It ships with a hardened steel nozzle and 500g of RFID filament, so you are not ordering parts before the first engineering print.
Its 40mm³/s direct-drive flow uses hardened steel gears, which matters for PLA-CF and PETG-CF where glass and carbon particles chew through brass drive gears. The chamber AI camera and nozzle camera handle flow rate auto-tuning across the bed.
Manufacturers list PLA, ABS, ASA, PPA-CF, PET-CF and other composites as supported, and the quick-swap hotend makes changing a worn nozzle painless. Creality OS handles WiFi and LAN remote monitoring with OTA updates.
At 61.6 pounds and 17 x 20 x 18 inches, it is a large machine, but the die-cast frame and linear rails keep layer consistency good at speed. Print speed is 600mm/s with 20,000mm/s² acceleration on FOC step-servo motors.
Is a 60C chamber worth more than a bigger bed?
For warping on ABS, ASA and PPA, yes. Chamber heat removes the temperature differential between the plastic and the air, which is the actual mechanism behind corner lift on large flat parts. Build volume only helps if you have parts that size.
The practical sweet spot for this machine is medium parts in fiber filled polymers. Include the hardened nozzle, watch the flow settings rather than the speed settings, and it produces clean functional components.
Read the one-star reviews before you buy
This is the lowest average rating in the roundup, with an 18% one-star share. That block concentrates on hardware rather than print quality: damaged extruder gears, a jammed filament path, and a Teflon tube blockage found in the box on arrival.
Check the filament path and extruder gears on day one, and keep the quick-swap hotend accessible. If your support response needs to be fast, test it before the first long print, not after.
4. QIDI Plus4: The Best Choice for PPS-CF and PAHT-CF
Pros
- 370C multi-metal integrated nozzle among the highest desktop ratings
- 400W second-generation chamber heating to 65C
- Explicit PPS-CF and PPA-CF/GF and PC support
- Dual Z motors and 10mm lead screws resist frame flex
- Quick setup with camera monitoring
Cons
- 16% one-star share on assembly and hardware faults
- 59-pound machine with a large footprint
The Plus4 is the machine I recommend to anyone whose material list includes PPS-CF. The 370°C multi-metal integrated throat nozzle is one of the highest-rated desktop hotends available, and the manufacturer names PPS-CF, PPA-CF/GF, ABS, ASA, PC and PA as supported rather than leaving you to guess.
Second-generation active chamber heating puts out 400W with air circulation and dual-layer insulation, reaching 65°C. Buyers who print engineering thermoplastics consistently point to that combination as the reason this printer works where others fail on PPS-CF and PA.
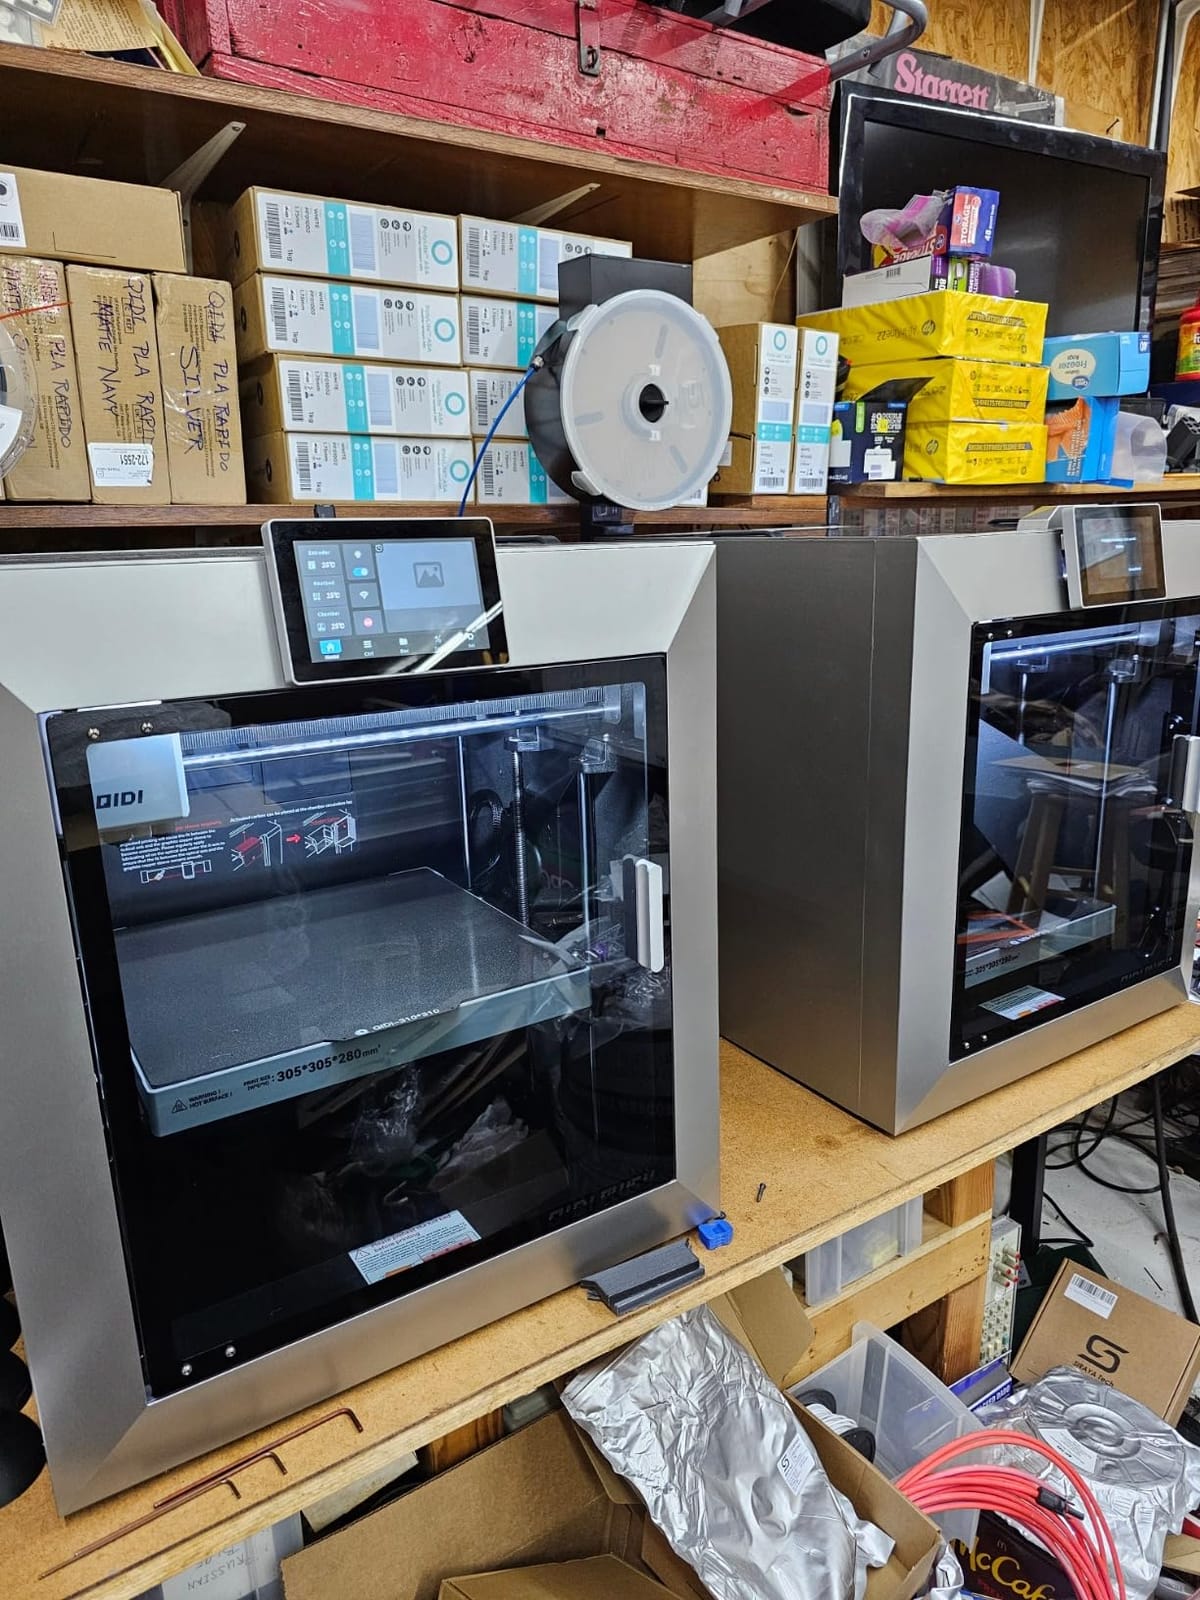
Structure is CoreXY at 12 x 12 x 11 inches of build volume, with independent dual motor-driven Z axes, 10mm lead screws and a 6mm thickened aluminium hotbed. Those numbers are about resisting frame flex, which is what shows up as layer splitting on tall parts.
An HD camera handles remote monitoring and time-lapse, and the integrated filament cutter, wrap and break detection work with the QIDI BOX MMU. Setup is close to ten minutes from unboxing to printing.
What can and cannot go through this hotend
At 370°C you have room for PPS-CF, PAHT-CF, PC, PPA-CF/GF, nylon, ABS and ASA. That covers the majority of engineering work done outside aerospace certification. PEEK and PEI remain out of reach at any desktop temperature.
The 12 inch cube is generous for a machine in this class, and dual Z motors mean tall parts do not need a rethink of the whole model when they reach the top of the chamber.
The 400W chamber is not a marketing number
Chamber recovery matters more than the peak reading. A chamber that hits 65°C in ten minutes but falls to 45°C at hour nine will still show you the corner lift you are trying to avoid, and 400W with air circulation and dual-layer insulation is the reason this one holds.
The trade-off is a 59-pound machine with a large 19.29 x 20.07 x 22.24 inch footprint, plus a 16% one-star share describing units arriving with assembly or hardware faults that required opening the machine. Inspect it early.
5. QIDI Q2: Best Value for a 370C Nozzle and 65C Chamber
Pros
- 370C nozzle paired with a 65C heated chamber at the entry level
- Nozzle doubles as the leveling sensor for a reliable first layer
- 1.5GT belt and full-metal CoreXY reduce ringing
- G3
- H12 HEPA and carbon filtration suit indoor work
Cons
- Smallest review base in the roundup
- QIDI BOX multi-material capability is an optional add-on
The Q2 is the cheapest route I found to a 370°C nozzle paired with a genuinely heated 65°C chamber. That pairing is the entire reason it is on this list, and owners highlight it as the combination that finally made PPS-CF and PA parts come out right on a desktop machine.
The nozzle doubles as the bed-leveling sensor, which removes the dependency on a bed surface and gives a consistent first layer without manual tuning. On a high-temperature plastic with a textured PEI sheet, that reliability matters more than it does with PLA.
Triple filtration runs a G3 pre-filter, an H12 HEPA filter and activated carbon, inside a flame-retardant chamber with closed-loop temperature sensors. For indoor work with ABS, ASA and nylon, that filtration stack is a genuine safety argument rather than a checkbox.
The CoreXY structure uses full metal with precision linear rails, an upgraded 1.5GT synchronous belt to reduce vertical fine artifacting, and a 600mm/s maximum speed. QIDI BOX support enables 16-colour dry-while-print multi-material work.
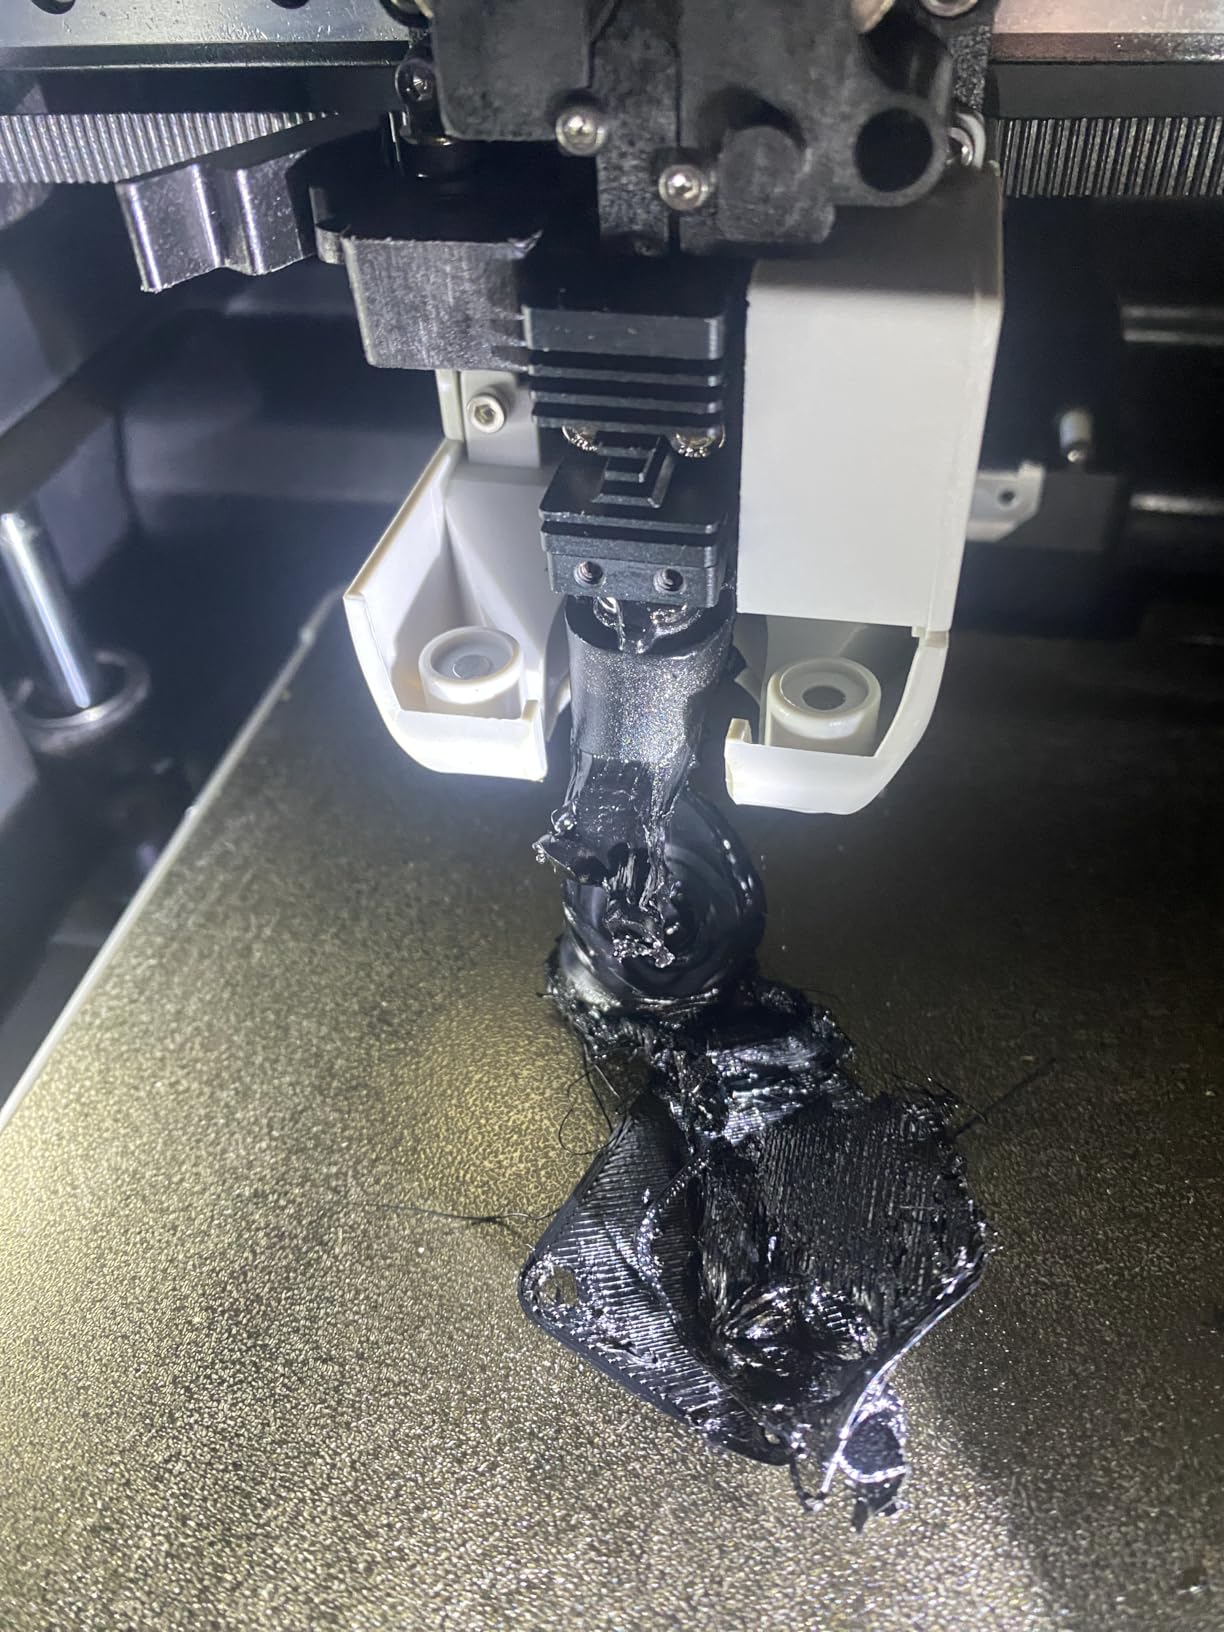
Is the smaller review base a real risk?
With 154 reviews the data set is thin, so treat the rating distribution cautiously. What is visible is healthy, with 70% five-star, and the failures that do appear are early setup and shipping issues rather than long-run quality.
Nozzle-as-sensor levelling means first layers land without calibration drama, which is the single biggest reason first-time buyers fail on engineering plastics. That feature alone justifies a closer look.
What you give up against the Plus4
The Plus4 adds 400W of chamber heating, 10mm lead screws and a slightly larger 12 x 12 x 11 inch build volume. The Q2 is lighter at 39.8 pounds and more compact, which matters if the machine lives in a home workshop rather than a studio.
Multi-material is an add-on with the QIDI BOX, so budget for that separately if you need 16 colours. If you only run one material at a time, the money is better spent on filament and a dryer.
6. Flashforge Adventurer 5M Pro: Best for Quiet Indoor Engineering Prints
Pros
- Fully enclosed and rated at 50dB or under
- Filtration blocks 99 percent of particles and VOCs
- 32mm3/s hot end handles nylon and PC
- Sub-10-minute setup with one-click leveling
Cons
- 280C ceiling sits below the 350-370C class
- No active chamber heating so chamber control depends on insulation
- Smallest build volume in the roundup
The Adventurer 5M Pro is the quietest enclosed machine in this group at 50dB or below, and it pairs that with a dual filtration system that blocks 99% of particles and VOCs. If your high-temperature work happens in a small office or a spare room, those two specs matter more than the nozzle ceiling.
Reviewers consistently name the enclosure, near-silent operation and filtration as the reason to buy it, and report that ABS, ASA and PC jobs succeed where open-frame machines warp. Setup takes under ten minutes with one-click levelling.
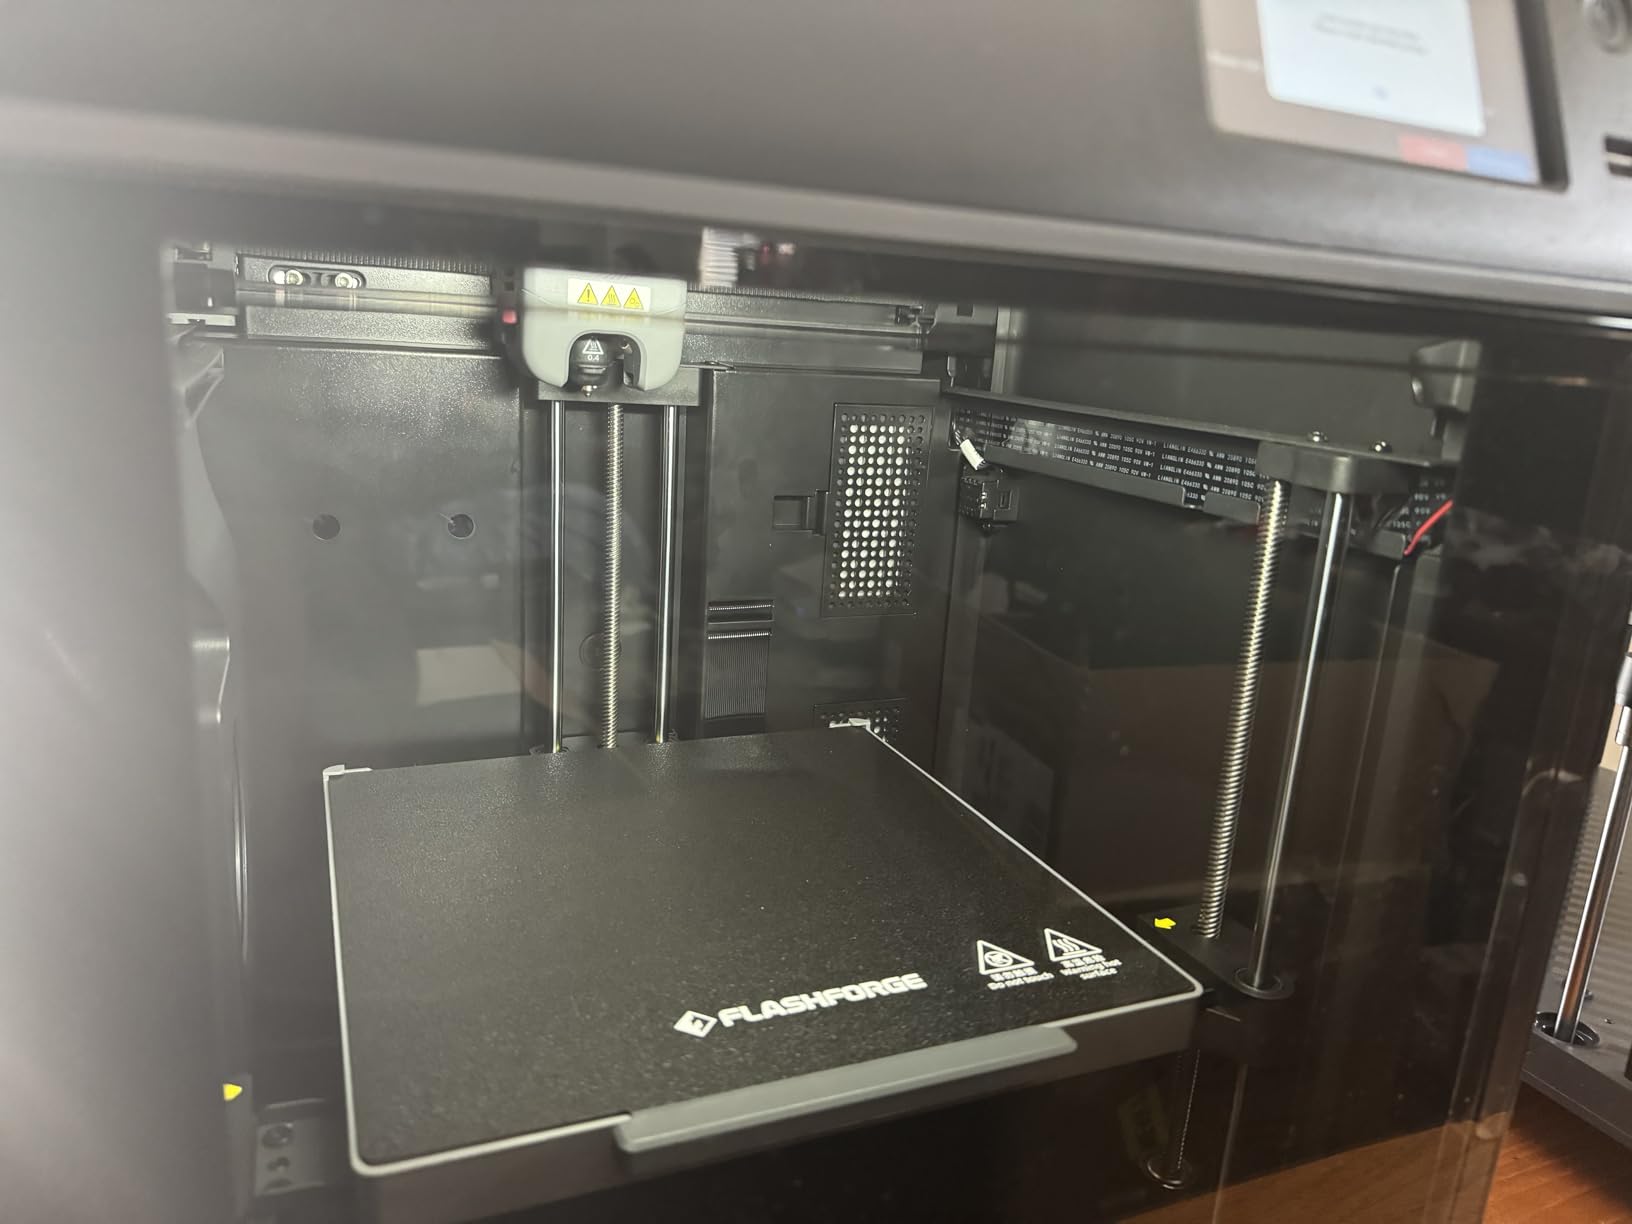
The 280°C direct extruder with a 32mm³/s high-flow hot end reaches 200°C in 35 seconds, and the all-metal design includes a runout sensor and power-loss recovery. Built-in vibration compensation plus nozzle and chamber fans keep surfaces consistent.
Supported materials include PLA, ABS, PETG, ASA, TPU, PC, PLA-CF, PETG-CF, ASA-CF and ABS Pro, so fiber filled grades are on the list. Build volume is 220 x 220 x 220mm and weight is 32.1 pounds.
Where the 280C ceiling stops you
280°C covers ABS, ASA, PC and standard nylon. It is below what PAHT-CF wants and well below the 350-370°C band needed for PPS-CF, so this is a machine for the mainstream end of engineering plastics only.
Without active chamber heating, the enclosure works by insulation. Small and medium parts hold up well, and a large flat ABS panel on a cold day is where you will see the corners lift no matter how good the first layer is.
Is the small build volume a problem?
At 220mm cube, parts larger than that need scaling or splitting, which is common for brackets and housings. For jigs, fixtures and functional prototypes under 200mm it is a non-issue, and the lower weight makes it the easiest machine here to move.
The noise figure is the underrated advantage. A machine you can run in a home office changes how often you actually print, and the filtration makes the ABS and ASA jobs defensible in that setting.
7. Bambu Lab P1S Combo: Best Enclosed Starter for ABS and ASA
Pros
- Enclosed body with an all-metal hotend handles PA and PC
- AMS makes 16-colour printing simple
- 500mm/s with automatic bed leveling
- About 15 minutes from box to first print
Cons
- Bambu lists fiber-reinforced polymers as not recommended
- Low-resolution screen is the most repeated complaint
- App and slicer workflow confuses first-time users
The P1S Combo is the easiest route into enclosed printing, and for ABS and ASA that is genuinely enough. The fully enclosed body with an all-metal hotend handles PA and PC, and the AMS makes multi-colour work something a beginner can actually do without relearning everything each time.
Reviews are heavily positive at 75% five-star, centred on setup speed, print quality and tolerances. One owner measured plus or minus .003 inch on RC aircraft parts, which is the sort of number that matters when parts have to fit an existing assembly.
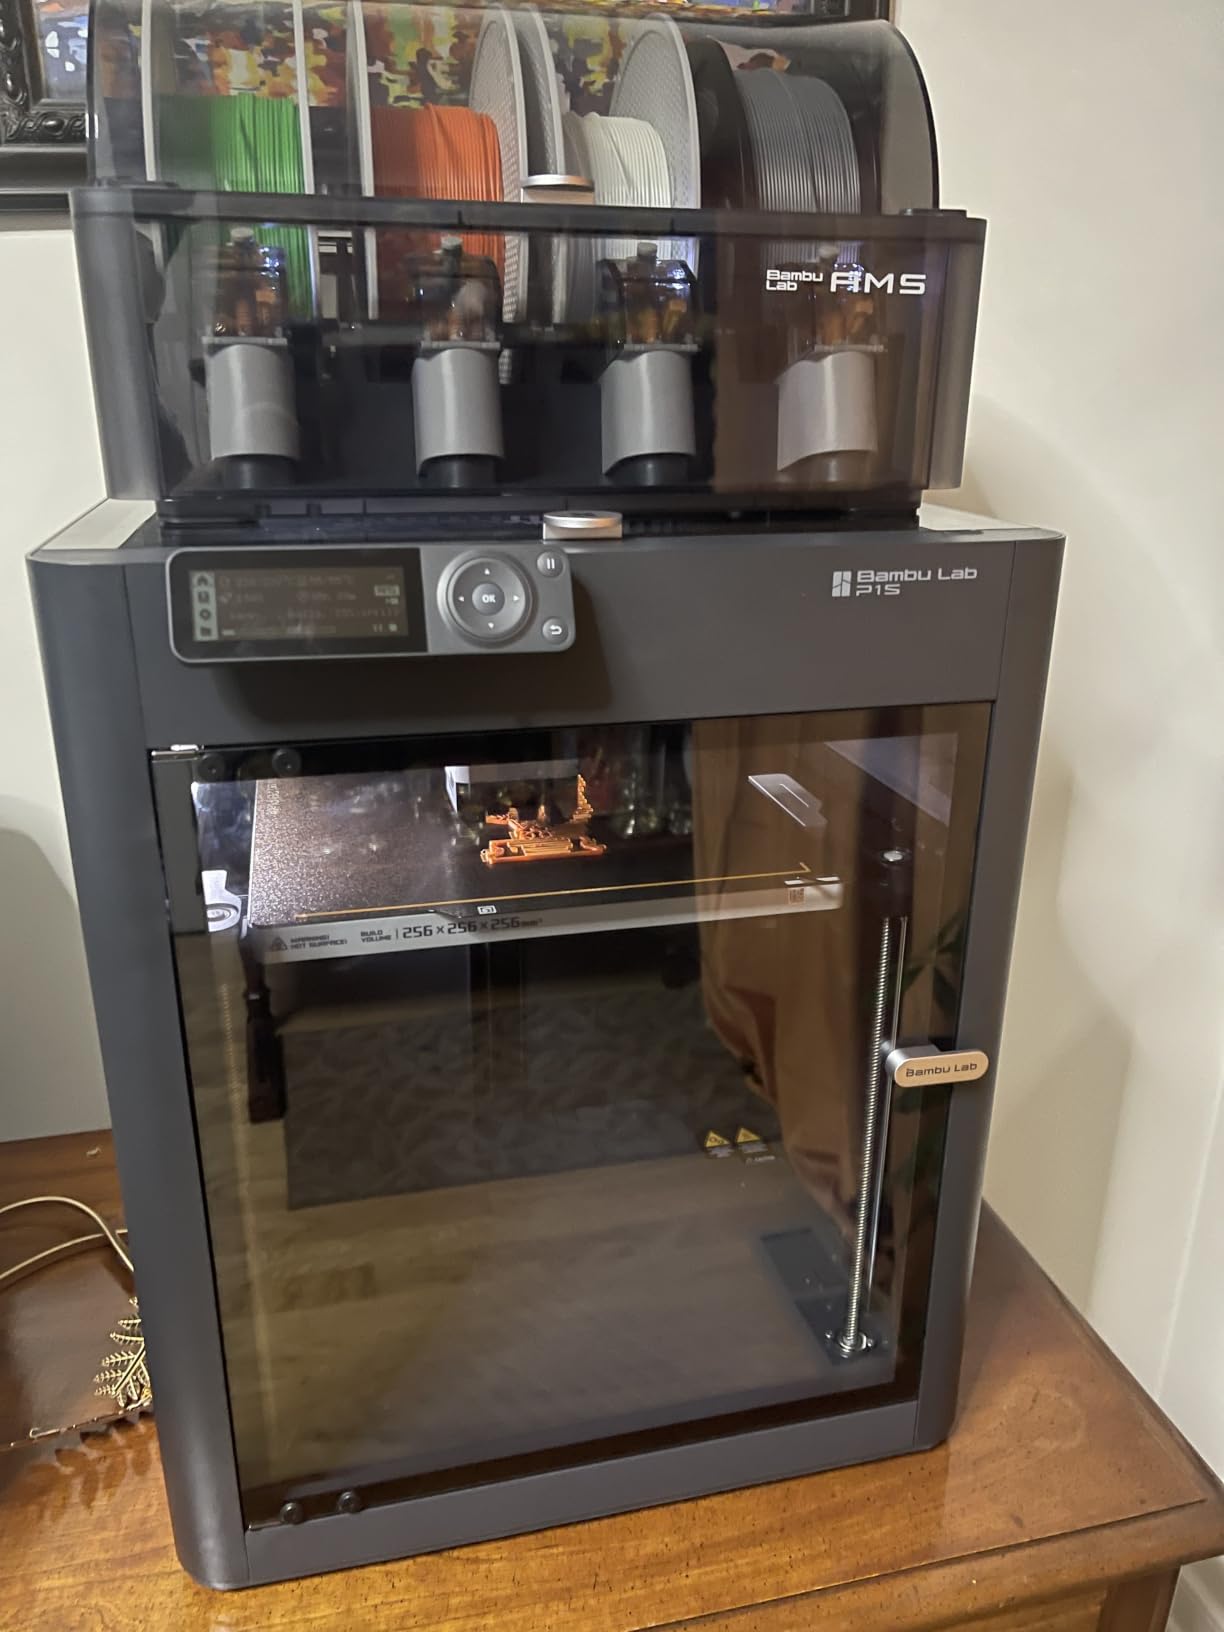
Speed is 500mm/s at 20,000mm/s² acceleration with automatic bed levelling, and setup takes about 15 minutes. The P1S Combo weighs 47.5 pounds at 15.31 x 18.03 x 15.31 inches, which is very manageable for a machine this capable.
Bambu Studio slicing and the MakerWorld model library are the software side. The printer is ideal for PLA, PETG, TPU, PVA, PET, ABS and ASA, with PA and PC described as capable but conditional.
The fiber filament warning you should not ignore
Bambu explicitly lists carbon and glass fiber reinforced polymers as not recommended. That is a manufacturer statement, not a user complaint, and it rules out a large chunk of the high-temperature filament this article is about.
If CF-filled nylon or ASA is on your list, choose a different machine. If your work is ABS, ASA and occasional PC, the enclosed body and all-metal hotend handle it well, and you avoid the 350-370°C premium entirely.
Is the closed ecosystem a problem long term?
Walled-garden concerns are the standard community criticism. Proprietary parts and app-centric workflow mean you tune inside the manufacturer’s software rather than in Klipper, and firmware lock-down has drawn complaints about SD card presets and error messages in the first week.
The low-resolution screen is the most repeated complaint, and only a small starter roll of filament is included. If you are comfortable with a vendor-controlled environment, none of that outweighs the ease of use.
8. Flashforge Adventurer 5M: Best Budget Entry That Needs an Enclosure
Pros
- All-metal CoreXY platform at the lowest entry point
- 280C direct extruder handles ABS and ASA basics
- Three-second detachable nozzle makes swaps fast
- One-click leveling and app monitoring keep it simple
Cons
- Open frame has no enclosure or chamber heat
- 280C ceiling sits at the low end
- One-star share is the weakest rating distribution here
The Adventurer 5M is the cheapest all-metal CoreXY platform here, and with 2,512 reviews it has the second-largest evidence base of any machine in the roundup. Buyers treat it as a value speed machine, and the 600mm/s motion with 20,000mm/s² acceleration is genuinely quick.
The 3-second detachable nozzle is a nicer detail than it sounds. When you move from PLA to ABS and want a hardened tip, the swap takes seconds rather than a teardown, which is the part of high-temperature printing that gets tedious on machines with fixed tooling. If you want a wider look at the entry tier, our best Elegoo 3D printers guide covers the other budget machines worth comparing side by side.
The 280°C direct drive extruder with a 32mm³/s high-flow nozzle and dual-fan cooling handles ABS and ASA basics, reaching 200°C in 35 seconds. The dual-sided PEI build platform and vibration compensation handle the first layer well.
It weighs 22 pounds, which makes it the easiest machine here to reposition, and the Flash Studio app gives remote monitoring and alerts. Optional nozzle sizes run from 0.25mm to 0.8mm around the standard 0.4mm.
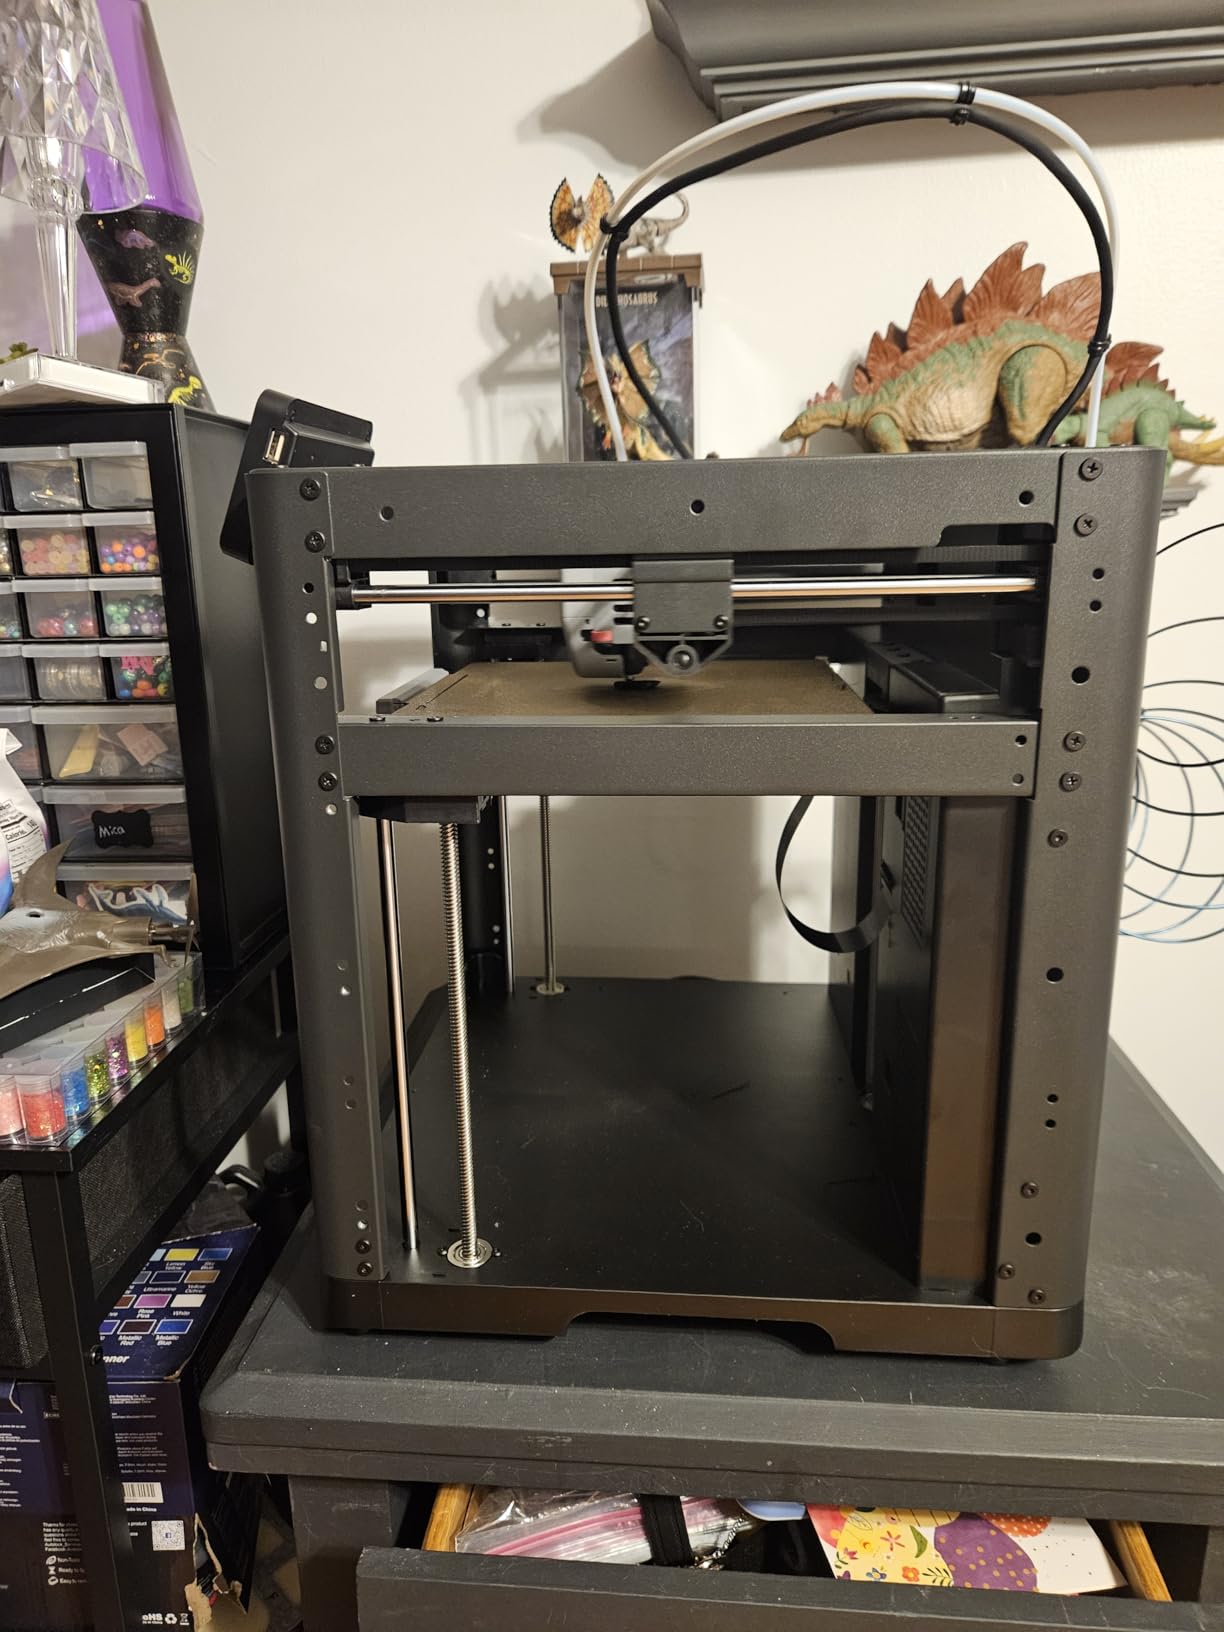
Why the open frame matters for engineering materials
This is the critical spec. There is no enclosure and no chamber heating, so drafts and room temperature set the chamber condition. Critical reviews say exactly this: ABS, ASA and nylon parts warp and need an aftermarket enclosure.
An enclosure gets you to the same place as the passively insulated machines, just later and with less control. Budget for it as a required accessory, not an upgrade, and treat the machine as a fast CoreXY platform inside a box.
Is the low price worth building around?
For a maker who wants speed and volume and will add a proper enclosure and a chamber mod, yes. The community consensus is that modding a budget CoreXY toward higher temperatures is a well-trodden path, though it is a project rather than a purchase.
Against that, the 3.9 rating carries an 18% one-star share, the weakest distribution in the roundup. Buy it for speed and build volume, not for out-of-the-box engineering results.
9. Sovol SV08: Best Open-Source Machine That Needs an Enclosure
Pros
- Open-source Voron 2.4 design with printable files available
- Klipper and OrcaSlicer with no locked firmware
- 350mm build volume with 700mm/s travel speed
- AC heated bed reaches 220C in 40 seconds
- Sovol support replaces boards and hotends
Cons
- Recurring hotend clogging reports
- No enclosure so nylon and PC need one added
- Loud under load from mainboard and cooling fans
The SV08 is a Voron 2.4 you do not have to build, and for high-temperature work the appeal is firmware freedom. Klipper gives you input shaping, pressure advance and PID tuning, and OrcaSlicer does the slicing, with no locked profiles and no subscription.
Build volume is 350 x 350 x 345mm at 700mm/s and 40,000mm/s² acceleration, which is the largest working volume in the roundup among machines that are not Creality desktop cubes. Quad-Gantry Leveling with four independent Z motors and pressure-sensor auto-levelling keeps tall parts honest.
The ceramic heating block and AC powered heated bed reach 220°C in 40 seconds, cutting heating time by 70% compared with a conventional bed. That speed matters when you run short engineering test prints to dial in a profile before committing to a long job.
Nozzle temperature is 300°C, so it handles ABS, ASA, PC and standard nylon like any enclosed 300C machine would, once enclosed. A PEI build plate is included and the machine weighs 39 pounds.
What adding an enclosure does and does not solve
It solves drafts, room temperature drift and most layer adhesion problems. It does not add chamber heat, so you are relying on insulation and a soaked chamber, which is a workable but slower approach to controlling warping on large parts.
For anyone who already understands printers, the ability to edit start G-code, set custom chamber temperatures and tune pressure advance per filament outweighs the slower thermal response. For a first machine, it is a steeper path.
The hotend clogging complaint you will keep reading
Multiple reviews describe repeated jams on ordinary PLA and PETG, followed by purchases of third-party or replacement hotends to fix them. This is the most consistent negative across 1,422 reviews, and it is worth treating as a likely cost line rather than a possibility.
Loud operation under load from the mainboard and part-cooling fans, plus some stringing between gaps that needs retraction and cooling tuning, are the other recurring notes. Sovol’s support is repeatedly praised, which partly offsets the hardware issue.
10. Creality K1C: Best Enclosed Starting Point for Carbon Fiber Filament
Pros
- Enclosed CoreXY with a tri-metal nozzle for fiber filaments
- One-tap auto calibration and an AI camera
- Silent mode at 45dB with activated carbon odor filtration
- Large established review base
Cons
- No active chamber heating on this older platform
- Reviews report extruder gear wear and jams
- Ringing is hard to tune and harder on locked-down firmware
The K1C is the oldest platform in the roundup and still one of the most recommended first enclosed machines. The direct extruder uses a tri-metal Unicorn nozzle built for high-temperature and carbon fiber filaments, inside an enclosed CoreXY body running 600mm/s at 20,000mm/s² acceleration.
One-tap auto calibration handles bed levelling without a manual routine, and the built-in AI camera does real-time monitoring, foreign-object detection and time-lapse. For long engineering prints, catching a failed layer at hour three is worth a lot.
Air purification uses activated carbon, and silent mode runs at 45dB or below, the quietest figure in this roundup. Dynamically balanced printhead fans reduce ringing and ghosting on the first layer. Weight is 35.2 pounds.
Owners frequently describe it as the machine that makes 3D printing enjoyable again, pairing well with Creality Print and the app. The large review base means the failure modes below are well documented rather than speculative.
What a tri-metal nozzle actually gets you
Carbon fiber and glass fiber filaments are abrasive, and a brass nozzle wears within hours. A tri-metal nozzle holds an edge far longer, which is why the K1C is a common first step into PA-CF and PET-CF without immediately budgeting for constant nozzle replacement.
It does not raise the temperature ceiling or add chamber heat. Enclosure plus a hardened nozzle is a solid combination for PLA-CF, PETG-CF, ABS and ASA at typical settings, provided you accept a passively controlled chamber.
The known issues are hardware, not print quality
Negative reviews concentrate on extruder gear wear and jams, plus early hotend failures and repeated mid-print stops at a fixed height. VFA and ringing is singled out as difficult to tune, and recent firmware lock-down restricts slicer access, which makes tuning harder still.
None of that changes the recommendation for a first enclosed machine, but if you already know how to tune a printer, a machine with open firmware will absorb that frustration better than this one will.
Heated Chamber Vs Hotend Temperature: Which Spec Actually Matters
Both matter, and confusing them is the most common mistake in this category. A high nozzle temperature melts the polymer. A warm chamber keeps each new layer above the previous layer’s softening point long enough to bond properly. Solve one without the other and the part still fails.
Warping happens because the material shrinks as it cools, and the bottom layers are stuck to the bed while the top is free. A chamber at 40-65°C slows cooling dramatically, so shrinkage happens in a more uniform state. That is why large flat ABS and ASA panels lift at the corners on an insulated-but-unheated machine.
Active chamber heating means a heater and a fan holding a measured setpoint through a long print. Passive insulation means the chamber starts warm and drifts toward room temperature over several hours. For a small part, the difference barely registers. For a ten-hour panel, it is the whole job.
The practical ordering looks like this. First, confirm the nozzle can reach your material’s extrusion temperature. Second, confirm the chamber type matches the size of the parts you make. Third, check the build plate, since PEI spring steel surfaces give ABS and nylon something to grip that textured PEI sheets and glass do not.
Part cooling fan is the dial most people get wrong on high-temperature prints. Running the fan at 100% cools the layer faster than the chamber can replace the heat, which is exactly the mechanism that causes delamination. Most profiles for ABS and ASA want little or no part cooling on the first few layers.
Filament Drying and Humidity Control for Nylon and PEEK
Nylon, PAHT-CF and PEEK pull moisture out of the air and store it in the polymer. Once enough water is absorbed, the failure looks like popping, stringing, bubbles and rough surfaces, and it gets attributed to the printer rather than the spool. In coastal or tropical regions people report a dryer becoming necessary within days of opening a spool.
A filament dryer is the correct answer, and it is a day-two purchase rather than an accessory. Dry to the spool, print immediately, and reseal or re-dry between jobs. A printer with integrated drying in its multi-material unit handles this automatically, which is a genuine advantage of the CFS and QIDI BOX systems in this roundup.
The same discipline applies to PPS-CF and PAHT-CF, though at a lower severity than unreinforced nylon. PA-CF and glass filled grades are noticeably less moisture sensitive because the filler absorbs less, but they are more abrasive, so the nozzle wear question comes forward instead.
One community warning worth repeating: high-temperature materials amplify every beginner mistake. Do not make ABS, ASA or nylon your first serious material. Learn bed levelling, retraction and temperature towers on something forgiving, then move up.
Fume Safety: Styrene, Caprolactam and Home Venting
ABS and ASA release styrene while melting, and nylon releases caprolactam. Both are irritants that nobody should breathe deliberately, and community advice is blunt about it: never print these materials in a closed bedroom with the air conditioning running, because the enclosure is not a fume extractor.
Filtration handles the particle and VOC load at the machine. HEPA captures particles, and activated carbon captures the volatile organic compounds that HEPA alone lets straight through. A carbon-only filter will not do the job for styrene, and neither machine nor filter replaces ventilation.
The machines here with the strongest filtration position are the QIDI Q2 with its G3 pre-filter, H12 HEPA and carbon stack, and the Flashforge Adventurer 5M Pro rated to block 99% of particles and VOCs. Both keep the machine defensible in a home workshop.
For anything beyond occasional parts, vent outside. Run a duct from the chamber or rear exhaust port to a window or through the wall, so air is moved out of the room rather than filtered and re-circulated. Filtration is for capturing what the machine makes; exhaust is for keeping it out of your breathing air.
PEEK and PEI printing raises a further step, since volatile degradation products appear if the material overheats. That is one more reason the industrial machines run their own extraction.
How to Choose a High Temperature Printer in 2026
Step one: write down the actual material list. ABS, ASA and PC put you in the 280°C class. Nylon and PA-CF need roughly 300°C. PPS-CF and PAHT-CF need 320°C and up, which means a 350-370°C hotend. If PEEK or PEI are on that list, you are shopping in a different category and no machine here will serve you.
Step two: match chamber type to part size. An enclosure alone is enough for parts under about 150mm. Above that, an actively heated chamber holding 60-65°C is what prevents corner lift on flat panels. A passively insulated chamber sits in between and is a compromise, not a feature.
Step three: check the hotend hardware, not just the temperature rating. Fiber filled filament is abrasive, so hardened steel extruder gears and a hardened or ruby nozzle matter more than the marketing temperature. A machine that advertises 300°C with a brass nozzle will not last long on PAHT-CF.
Step four: be honest about build volume versus rigidity. Large build volumes need frame stiffness to stay dimensionally accurate, and the indicator is dual Z motors, thick lead screws and a rigid bed mount. A 350mm cube on a thin frame produces tall parts with layer splitting you cannot slice your way out of.
Step five: decide about firmware and serviceability. Closed ecosystems give you easier first prints and limit how you tune exotic profiles. Open Klipper machines give full control and expect you to maintain them. Check whether the manufacturer replaces boards, load cells and hotends, because on several of these machines that support is a genuine strength. Our best Prusa 3D printers roundup covers the other common benchmark for open, serviceable firmware if you want a non-Creality baseline.
Budget for the consumables too. Abrasive filaments consume nozzles, filtration needs replacing, and hygroscopic materials need a dryer. A printer purchase plus dryer plus a spare hardened nozzle is the realistic total for a working high-temperature setup, and our prototyping printer guide covers the general machine categories if you are still narrowing the shortlist.
Frequently Asked Questions
What is the best 3D printer for high temperatures?
The Creality K2 Plus Combo is the strongest all-round option, with a 350C hardened nozzle and an actively heated 60C chamber in a 350mm cube. The QIDI Plus4 and Q2 push further with 370C nozzles and 65C chambers for PPS-CF and PAHT-CF. No desktop machine in this roundup reaches PEEK or PEI temperatures of 400C and above.
What 3D printer will print PEEK?
A dedicated industrial machine with a 400-450C extrusion system and a heated chamber above 100C. Desktop printers in this roundup top out at 370C, so PEEK and PEI are out of reach regardless of brand. If PEEK is the requirement, budget for an industrial PEEK-class machine rather than a desktop upgrade.
What temperature is ideal for 3D printing PEEK?
PEEK typically prints between 400C and 450C at the nozzle, with the chamber held near the material glass transition temperature. That combination demands a water-cooled or heavily insulated hotend, a rigid all-metal chamber and chamber temperatures well above anything a desktop enclosure provides.
Which 3D printer filament is best for high temperatures?
For heat resistance at a realistic price, ASA or ABS is the practical answer. Polycarbonate and PA-CF handle more heat and impact but are harder to print. PPS-CF and PAHT-CF are for genuinely hot, stiff parts, and PEEK or PEI only make sense when service temperature exceeds 200C and the process can justify industrial equipment.
Can PETG withstand 100c?
Standard PETG softens well below 100C, with a glass transition temperature around 80C, so parts in sustained heat will distort. High-temperature PETG blends exist that improve on this, but for a part living near 100C choose ASA, polycarbonate or a PA-CF grade instead and print it on a 300C or 350C machine.
Do I need an enclosed 3D printer for ABS and nylon?
Yes. An enclosure blocks the drafts and temperature swings that cause layer separation in ABS, ASA, PC and nylon. For small parts a passive enclosure is enough, while large flat parts above roughly 150mm benefit from an actively heated chamber holding 40-65C to prevent corner lift and cracking.
Final Verdict: Best 3D Printers for High Temperature Filaments in 2026
For the best 3D printers for high temperature filaments, the answer depends on how far up the temperature scale your parts need to go. If ABS, ASA, PC and standard nylon cover your work, the Creality K2 Combo gives you a hardened 300°C hotend, an enclosed 260mm cube and the largest review base in the group, and it is the machine I would put on a bench first.
If fiber filled engineering polymers are the real target, the Creality K2 Plus Combo wins on the 350°C nozzle and 60°C actively heated chamber, and nothing else here pairs that with a 350mm cube. For PPS-CF and PAHT-CF, the QIDI Plus4 and QIDI Q2 take the nozzle to 370°C and the chamber to 65°C, which is the practical ceiling for desktop machines.
The Bambu Lab P1S Combo is the easiest machine to live with for ABS and ASA, and the Flashforge Adventurer 5M Pro is the one to run indoors quietly with proper filtration. If you want open-source control and can accept adding an enclosure, the Sovol SV08 gives you Klipper and a 350mm build volume. Check the individual reviews above for the failure modes each one carries, and match the machine to your highest-temperature filament rather than your average one.

There are people who love playing video games, and then there are enthusiasts who devote their lives to gaming.
Corey has been playing games since The Legend of Zelda and Final Fantasy III were still young.
Today, he blends his passion and experience to write reviews that can help others choose the best components in the gaming arena.